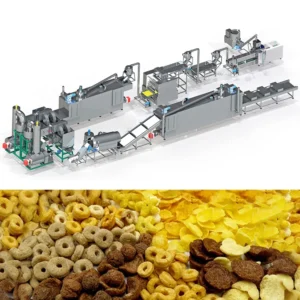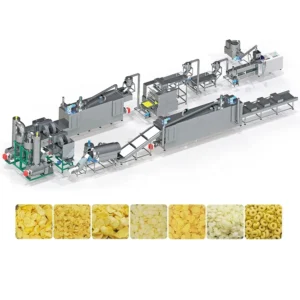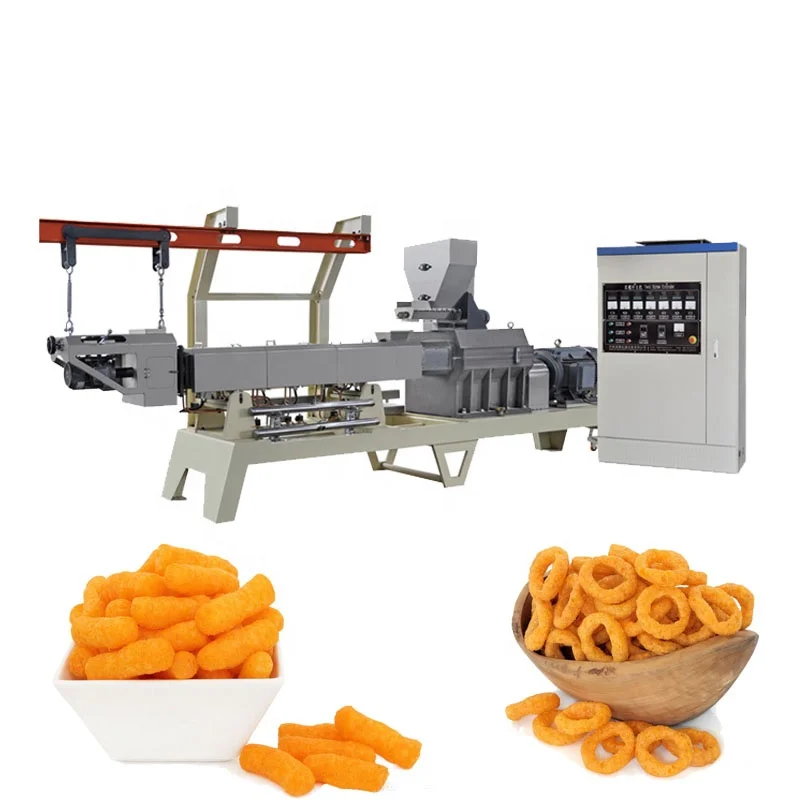
Material-matched extrusion design — screw profiles and barrel zones specified to the exact cereal formulation before the line is built, ensuring consistent starch gelatinization and flake density.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 (also available: MT70, MT85) |
| Product Type | Twin Screw Extruder Corn Flakes Production Line |
| Extruder Type | Twin Screw with automatic lubricating and cooling |
| Installed Power (MT75) | 210 kW |
| Power Consumption (MT75) | 150 kW |
| Output Capacity (MT75) | 300–500 kg/h (basis to be confirmed on specific raw material) |
| Overall Dimensions (MT75) | 45 × 1.5 × 3.5 m |
| Control System | PLC and MCC control |
| Flaking Machinery | Hydraulic double rollers, separate motor drive, infrared temperature sensing |
| Roasting Oven | Vibrating pan, conciliation burner, cyclone dust removal |
| Dryer Heating Source | Gas or electric (selectable) |
| Voltage & Frequency | Customized to local grid |
| Assembly State | Complete production line |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn powder, corn grits |
| Sugar-coated cereal flakes | Corn, rice, wheat, oat, barley blends with sugar coating |
| Shaped breakfast cereals | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart formats |
| Fortified cereal production | Multi-grain formulations with added nutritional profiles |
| Instant porridge making | Pre-gelatinized grain powders |
Why Generic Screw Profiles Sink Corn Flakes in Milk
A copied screw configuration produces the wrong starch gelatinization, leading to poor bowl-life and immediate sogginess.
When process engineers evaluate a breakfast cereal line, the quoted throughput often ignores the material science happening inside the barrel. A standard screw setup might process basic corn grits adequately, but once the formulation shifts to include oats, barley, or fortified additives, the shear profile changes entirely. The barrel temperature zones fail to deliver the necessary thermal input, resulting in incomplete gelatinization. The final flake lacks the internal cellular structure required to resist milk absorption, sinking to the bottom of the bowl within seconds [NEED_CITE: starch gelatinization requirements for cold cereal bowl-life].
Shear, Moisture, and the Gelatinization Window
Twin-screw extrusion relies on precise mechanical and thermal energy to alter the starch matrix. The corn flakes extruder extrusion technology requires balancing moisture content with barrel heat to achieve full gelatinization without premature expansion. If the moisture is too low or the shear insufficient, the starch granules remain partially crystalline. This structural failure only becomes apparent after flaking and roasting, when the product exhibits a dense, hard texture rather than the expected crispness.
Barrel Temperature Profiling for Cereal Formulations
Modern extrusion barrels are divided into multiple heating and cooling zones. Managing these zones allows the operator to control the viscosity of the melt as it moves toward the die. For high-sugar or fortified formulations, the melt viscosity drops significantly, requiring aggressive cooling in the final zones to maintain die pressure. Without this precise control, the extrudate expands unpredictably at the die face, ruining the uniformity required for consistent flake thickness [NEED_CITE: thermal management in twin-screw food extrusion].
Interpreting the Drive and Flaking Specifications
The MT75 operates with a substantial installed power draw to maintain torque across the twin shafts, especially when processing high-fiber or multi-grain blends that increase melt viscosity. The automatic lubricating system within the gearbox ensures continuous operation under heavy load, protecting the screw bearings from premature wear. Downstream, the flaking machinery utilizes a hydraulic system for its double rollers, with separate motors driving each roll. This independent drive, combined with infrared temperature sensing, maintains uniform nip pressure and roll temperature, preventing the cooked extrudate from tearing or sticking during the critical flattening stage.
The Hidden Cost of Unmatched Line Throughput
A frequent failure point in cereal processing occurs when the extruder output exceeds the capacity of the downstream flaker or roaster. Extrudate backs up, cooling unevenly before it reaches the nip rolls, which destroys the necessary plasticity for smooth flaking. Alternatively, if the roasting oven lacks the residence time to handle the volume, surface bubbling and caramelization remain incomplete, leaving the flake chewy and prone to staling [NEED_CITE: throughput balancing in food processing lines].
Why Engineering the Process Matters Here
Every line is configured from the batching system through to packing to ensure throughput matches at every station, eliminating bottlenecks that strand hot extrudate. Screw configurations and die designs are specified against the buyer’s exact raw material and target density rather than relying on generic builds. Before any equipment ships, raw materials are run through the in-house testing workshop to verify gelatinization, expansion, and final flake texture. This technical validation ensures the extrusion parameters are locked in before installation begins.
Documentation & Verification
- Line layout showing throughput calculations matched across extruder, flaker, and roaster
- Screw and die configuration record specified to your cereal formulation
- Factory trial run report on your actual raw material before dispatch
- Electrical schematic with confirmed local voltage and control language
- Operation manual detailing barrel zone profiles and hydraulic flaker pressures
Installation, Commissioning & Support
- Foundation planning accounts for the 45-meter length and heavy extruder mass
- Power infrastructure review ensures dedicated circuits for the 210 kW extruder drive
- Barrel zone calibration and PLC interface setup during initial commissioning
- Hydraulic flaker nip pressure tuning matched to your specific cooked extrudate
- Roaster airflow balancing to achieve target moisture reduction and surface blistering
- Wear parts inventory covering twin screws, die plates, and flaker roll scrapers
Inquiry Parameters for Process Engineers
To properly configure the screw profile and barrel heating zones, technical buyers should provide the exact grain formulation, including protein and fiber percentages. Detailing the target flake thickness and required bowl-life performance allows for precise die selection. Please also specify the available plant footprint and local electrical standards to align the line layout and motor control centers.
Frequently Asked Questions
Q: How is screw configuration determined for different cereal raw materials?
A: Screw elements are selected based on the starch and protein content of your specific grain blend. High-fiber materials require specialized kneading blocks to generate sufficient shear for gelatinization without excessive wear, while high-sugar blends need elements that manage melt viscosity and prevent burning inside the barrel.
Q: What barrel temperature profile is needed for proper starch gelatinization?
A: A stepped temperature profile is typically required, starting lower in the feed zone to prevent premature gelatinization and bridging, then ramping up through the mixing and metering zones. The final zones often require active cooling to stabilize the melt pressure before it exits the die.
Q: How does die design affect flake expansion and final crispness?
A: The die aperture geometry and land length control the pressure drop at the exit, which dictates the initial expansion of the extrudate. Proper die design ensures a consistent, dense pellet that flattens uniformly in the flaker and develops the correct cellular structure during roasting for optimal crispness.
Q: Can we run a trial on our raw material before the line ships?
A: Yes, raw materials are processed in the testing workshop prior to shipment. This trial verifies the screw configuration, barrel profile, and die selection, generating a physical sample and a technical report confirming that the target flake density and texture are achievable.
Q: How is throughput balanced between the extruder and the roasting oven?
A: Capacity calculations ensure that the residence time in the roasting oven matches the extruder output. If the oven is undersized, flakes exit with too much residual moisture; if oversized, the product over-bakes or burns, degrading the final color and taste profile.