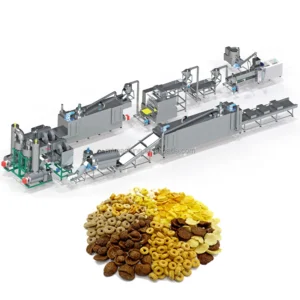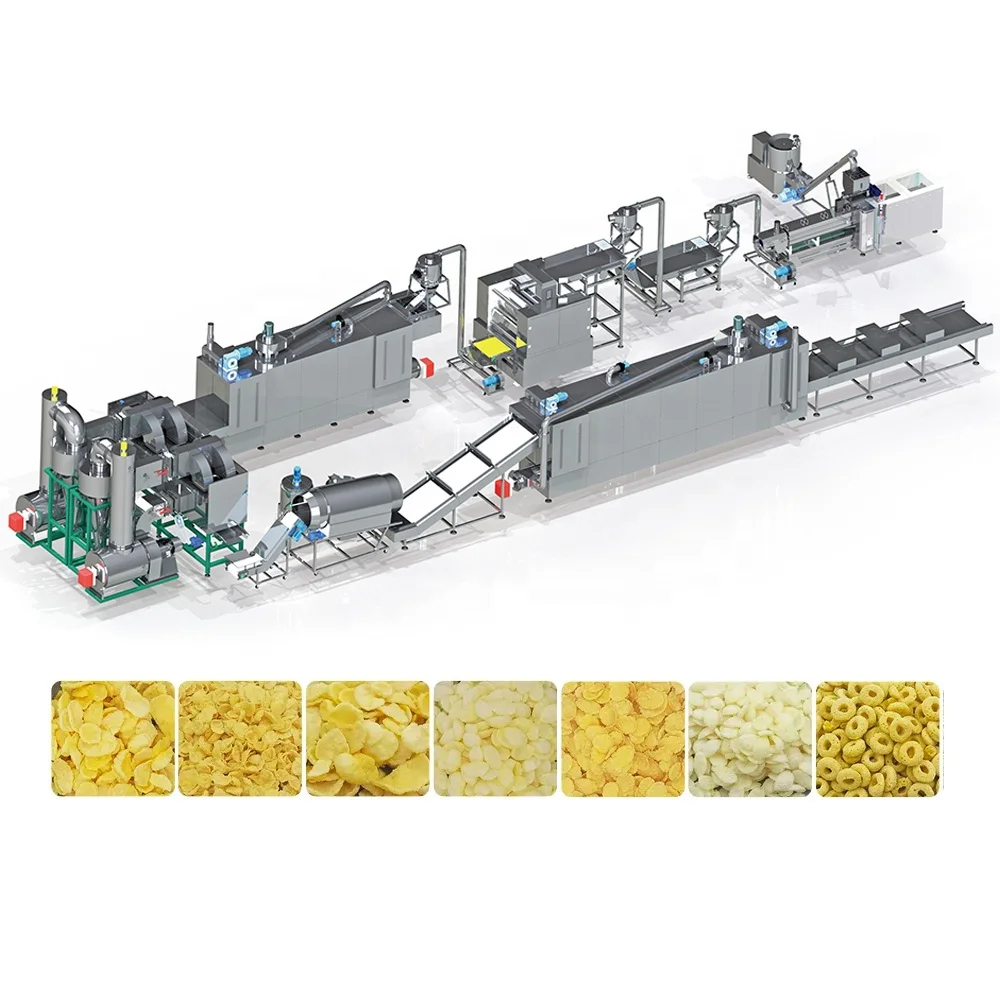
Screw Configuration Matched to Your Grain Blend — Every MT-75 barrel segment and die opening is specified against the buyer’s actual corn, rice, or oat flour mix before the line ships.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-75 |
| Product Type | Twin Screw Breakfast Cereal Extrusion Line |
| Screw Type | Co-rotating twin screw, sectional modules |
| Mixer Tank Size | φ600 × 500 mm |
| Mixer Power | 4 kW |
| Mixer Output | 10–30 kg per load |
| Screw Elevator Driving Power | 0.75 kW |
| Corn Flakes Press Machine Power | 16.12 kW |
| Press Roller Size | 510 × 310 × 1050 mm |
| High-Temperature Oven Size | 4.5 × 1.4 × 1.8 m |
| Oven Heating Method | Gas, both-side baking system |
| Sugar Spraying System Power | 28.75 kW |
| Sugar Spraying Roller Size | Ø600 × 2700 mm |
| Control System | Separate controller box (PLC/MCC option to confirm) |
| Voltage & Frequency | Configurable (e.g., 3ph 380V 50Hz, 3ph 415V 60Hz) |
| Line Assembly | Complete from batching to packing |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn flakes production | Corn grits, maize flour, rice flour |
| Cereal rings and hoops | Wheat flour, oat flour, mixed grain blends |
| Choco hoops and fruit loops | Grain base with cocoa or fruit additive |
| Sugar- or honey-coated snacks | Extruded cereal shapes with syrup glazing |
| Fortified breakfast cereals | Grain flour with added vitamin premix |
What "Nominal Throughput" Hides About Your Grain Blend
A breakfast cereal line only meets its rated output when the screw profile matches the starch behaviour of your exact flour mix.
Many producers discover after installation that a twin screw extrusion breakfast cereal line specifications sheet assumed a standard corn grits recipe, while the buyer intended to run a high-fibre oat or whole wheat blend. The result is under-gelatinised dough, poor expansion at the die, and flakes that crack rather than crisp [NEED_CITE: starch gelatinisation temperature variance across grain types]. I have seen lines sit idle for weeks while the supplier ships replacement screw elements from overseas. The gap between quoted capacity and real output almost always traces back to one variable that was never tested before the contract was signed.
How Barrel Zones Shape Starch Gelatinisation
The co-rotating twin screw design on the MT-75 uses sectional modules that can be arranged for forward transport, mixing, de-gassing, cooking, and forming in sequence. Each barrel zone carries an independent heating circuit, allowing the temperature profile to rise gradually from feed intake through the gelatinisation window. For corn-based flakes, the starch typically requires sustained heat above a threshold that differs from wheat or oat recipes. Adjusting the screw element pitch and barrel zone sequence lets the operator hold the dough inside the cooking zone long enough for complete starch conversion without scorching the barrel wall.
Die Geometry and Expansion Control
The die plate sits at the discharge end of the barrel, and its opening diameter combined with the land length determines the expansion ratio of the extrudate as it exits into atmospheric pressure. A wider land length restrains expansion, producing a denser pellet suited to corn flakes pressing, while a shorter land allows greater puff for cereal rings. The twin screw extrusion breakfast cereal line specifications must document which die insert is matched to each target shape so that operators can swap dies when switching from flakes to hoops without trial-and-error downtime [NEED_CITE: die land length and expansion ratio relationship in twin screw extrusion].
Reading the Press Machine and Oven Specs
The corn flakes press machine uses rollers sized at 510 × 310 × 1050 mm with an adjustable gap to set flake thickness, and an integrated cooling circuit keeps the roller surface from sticking to the hot pellet. Downstream, the gas-fired oven stretches 4.5 metres with a both-side baking arrangement that exposes flakes to heat from above and below, reducing the moisture gradient that causes curling or uneven colour. The sugar spraying system adds 28.75 kW of drive and heating power across a Ø600 × 2700 mm roller, coating the cereal with syrup before the final drying pass. These three stations must be balanced so that the press output rate matches the oven belt speed, preventing pile-ups or gaps that ruin batch consistency.
The Cost of Skipping the Trial Run
When a line ships without a test on the buyer’s actual flour blend, the first production run becomes the trial. Operators adjust screw speed, moisture addition, and barrel temperatures while raw material is consumed and off-spec product accumulates [NEED_CITE: material waste during unplanned commissioning runs]. Coating drums may overflow if the extruder throughput exceeds the syrup application rate, and the final dryer may fail to bring moisture down to the shelf-stable target. These problems compound because each station depends on the one before it, and correcting one variable often shifts another out of tolerance.
Why the MT-75 Line Holds Up Across Formats
Screw and die configurations are written to the buyer’s grain blend and target cereal shape, not copied from a generic build. The in-house testing workshop runs the buyer’s raw material through the extruder before shipment, generating a trial report that locks in barrel temperatures and screw speed. Every station from the flour mixer through the packing machine is sized under one supplier, so the press, oven, and coating drum capacities are matched to the extruder output rather than assembled from mismatched vendors. Electrical schematics confirm voltage and frequency before production starts, avoiding commissioning delays caused by incompatible motor starters or heater elements.
Documentation & Verification
- Screw and die configuration record tied to your grain flour and target shape
- Trial run report using your raw material before the line leaves the factory
- Electrical schematic with confirmed voltage and control language
- Line layout drawing showing throughput balance across every station
- CE declaration of conformity covering the full assembly
Installation, Commissioning & Support
- Foundation plan accounts for the 4.5 m oven length and press machine footprint
- Separate controller box requires a dedicated circuit matched to confirmed voltage
- Line ships in modular stations for staged assembly inside the production hall
- First-run parameter sheet from the trial report guides initial screw speed and barrel set-points
- Roller and screw element wear parts list included for the first replacement cycle
Preparing Your Inquiry
To configure the twin screw extrusion breakfast cereal line specifications for your facility, share your primary grain flour type, any vitamin or cocoa additives, and the target cereal shapes. Include your local three-phase voltage and frequency, the available floor length and ceiling height, and whether you plan to coat with sugar syrup or honey. If you can send a sample of your flour blend, a pre-shipment trial run can be scheduled to verify expansion and density before the line is finalised.
Frequently Asked Questions
Q: How is the screw configuration adjusted for different grain flours?
A: Sectional screw modules are rearranged to change the balance of transport, mixing, and cooking elements. Higher-fibre flours like oat or whole wheat typically need more shear and a longer cooking zone than refined corn grits, so the element sequence and barrel heating profile are revised accordingly before the trial run.
Q: What barrel temperature profile works for corn flakes versus wheat hoops?
A: Corn flakes generally need a steady temperature climb that holds starch in the gelatinisation range long enough for full conversion before the die. Wheat hoops often require a slightly different peak and shorter land length to allow greater expansion. Both profiles are documented in the trial run report for your specific blend.
Q: How do you match die design to the target cereal shape?
A: The die insert opening diameter and land length are selected to control the expansion ratio as dough exits the barrel. Flakes use a die that produces a compact pellet for pressing, while rings and hoops use a die that allows more radial puff. Inserts are swapped when the production format changes.
Q: Can throughput be verified on my raw material before shipment?
A: Yes. The in-house testing workshop runs your flour blend through the MT-75 extruder, recording barrel temperatures, screw speed, moisture addition, and the resulting expansion and density. This trial report ships with the line and serves as the baseline for commissioning at your facility.
Q: How are the dryer and coating drum matched to extruder output?
A: Each station is sized under one supplier so that the press, oven belt speed, and sugar spraying drum capacity align with the extruder discharge rate. This prevents material pile-ups between stations and keeps moisture and coating levels within the target specification throughout the run.