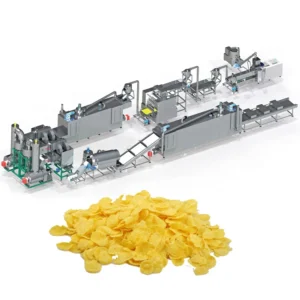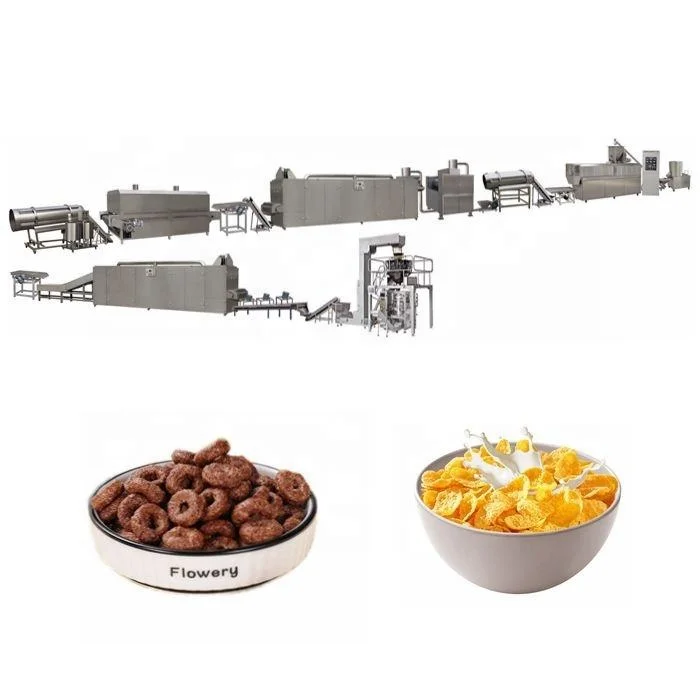
Matched extrusion and downstream stations — throughput from the twin-screw barrel through flaking, drying and roasting is calculated as one system so no single station bottlenecks the corn flakes line.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extruded Corn Flakes Production Line |
| Models Available | MT70, MT85, MT75 |
| Screw Type | Twin-screw |
| Installed Power (MT70 / MT85 / MT75) | 160 kW / 190 kW / 210 kW |
| Power Consumption (MT70 / MT85 / MT75) | 120 kW / 140 kW / 150 kW |
| Output Capacity (MT70) | 150–200 kg/h (basis not stated in source) |
| Output Capacity (MT85) | 300–400 kg/h (basis not stated in source) |
| Output Capacity (MT75) | 300–500 kg/h (basis not stated in source) |
| Overall Dimensions (MT70 / MT85 / MT75) | 41 × 1.5 × 2.2 m / 43 × 1.5 × 3.2 m / 45 × 1.5 × 3.5 m |
| Control System | PLC (flaking machinery), MCC |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Extruder Features | Automatic lubricating, cooling function |
| Flaking Drive | Double motors for separate roller driving; hydraulic system |
| Flaking Temperature Control | Infrared sensor |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Final Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart |
| Line Stations | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Sugar Coating (optional) → Cooling → Packing |
| Standards | CE (since 2014), ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal market | Corn grits or corn flour, flaked and roasted without sugar coating |
| Sugar-coated or frosted corn flakes | Corn base with sugar syrup applied in tumble coating drum |
| Multi-grain breakfast cereals | Blends of rice, wheat, oat and barley powder extruded on the same twin-screw platform |
| Shaped cereal pieces for children’s segments | Fruit loops, stars, wheels and hearts formed by swapping the extruder die |
| Expanded snack formats | Corn, rice or wheat pellets expanded through the same extrusion barrel |
Why "300 kg/h" Means Nothing Without the Raw Material Context
A rated capacity only holds when the starch content, particle size and moisture of the actual grain match what the screw configuration was designed for.
I spent two weeks in Colombia re-tuning a corn flakes line because the buyer switched from standard corn grits to a locally sourced corn flour that was finer and lower in starch. The gelatinisation window shifted, the flakes came out hard with no surface blisters, and the barrel temperature profile had to be rebuilt from scratch. Any corn flakes extrusion line specifications you compare across suppliers should be read against the exact grain source you plan to run [NEED_CITE: effect of starch content on twin-screw gelatinisation]. A number quoted on one feed stock may not transfer to another, which is why locking in a trial on your raw material matters more than the headline output figure.
How Screw Configuration Defines the Flake
The twin-screw extrusion technology behind this line starts with selecting the screw element arrangement — conveying, kneading and reverse elements — to match the grain blend and target gelatinisation degree. Corn demands a different shear profile from oat or barley, and the die aperture sets the pellet size that the flaking rollers will later flatten. Getting the screw and die combination right determines whether the final flake has the internal void structure that gives milk-bowl crispness, and this is the core of twin screw corn flakes extruder technology.
Barrel Temperature, Moisture and Starch Gelatinisation
Each barrel zone is independently heated and cooled, letting the operator build a temperature curve that moves the dough from partial gelatinisation at the feed end to full cook before the die. Moisture injection points and vent ports control the water activity that the starch granules see during their residence time. [NEED_CITE: starch gelatinisation temperature range for corn and wheat in extrusion]. If the moisture drops too early the dough skins over and the pellet will not flatten uniformly in the flaking station; if it stays too high the pellet sticks to the rollers and edges tear.
Reading the Power and Dimension Data
The three models — MT70, MT85 and MT75 — step up in installed power from 160 kW to 210 kW, and actual power consumption sits roughly 75% of installed figures, which reflects the motor load under typical corn dough conditions. Line length grows from 41 m to 45 m across the range, driven mainly by the dryer and roasting oven sections needed to handle higher throughput. The flaking station draws power from double motors with separate roller drives, so each roller speed can be fine-tuned to prevent flake tearing at higher feed rates. The hydraulic gap system and infrared temperature sensor hold roller spacing and surface heat constant, which is where uniform flake thickness originates before the product ever reaches the roaster.
When Downstream Stations Become the Real Bottleneck
An extruder that pushes more dough than the flaking rollers can flatten simply piles wet pellets at the infeed, and those pellets cool below the temperature window where they can be pressed into intact flakes. The roasting oven faces a similar constraint: if the residence time inside the dual-fan chamber is too short for the volume passing through, surface blisters never form and the flake tastes raw rather than toasted. [NEED_CITE: hot-air roasting residence time and blister formation in breakfast cereal production]. Matching extruder output to flaker capacity and oven belt speed at the design stage avoids these downstream choke points that no amount of on-site tweaking can fully fix.
What the Line Delivers When Configured as One System
Every station from batching to packing is specified by a single supplier, so throughput, utility loads and control signals are calculated together rather than bolted together from separate vendors. The screw configuration and die design are selected against your raw material and target flake density before the extruder is built, not copied from a generic template. An in-house testing workshop runs your actual grain through the barrel and flaking station before shipment, so the temperature curve and roller gap are locked rather than guessed. PLC and MCC control across the full line keeps barrel zones, roller drives and roasting oven burners on one coordinated platform. Pre-sales engineering, on-site installation, commissioning and ongoing wear-part support stay with one team from first inquiry through production ramp-up.
Documentation & Verification
- Line layout and capacity calculation matching extruder output to flaker and roaster throughput
- Screw and die configuration record matched to your grain blend and target flake density
- Trial run report on your raw material conducted in the testing workshop before dispatch
- Electrical schematic confirming voltage, frequency and PLC language for your facility
- CE declaration of conformity and ISO certificate for customs and regulatory entry
- Operation and maintenance manual with wear parts list for screws, dies and roller shells
Installation, Commissioning & Support
- Floor space of up to 45 × 1.5 m requires level concrete with anchor points for the extruder and flaking station
- Dedicated power circuit sized for up to 210 kW installed load on the MT75 model
- Line arrives in modular sections; extruder barrel segments, flaking rollers and oven panels assembled on site
- First run includes barrel temperature curve mapping and hydraulic roller gap calibration on your grain
- Operator training covers PLC screen navigation, screw element swapping and infrared sensor zeroing
- Wear parts stock includes spare screw elements, die plates and roller shells sized to the line
What to Include in Your First Technical Inquiry
Share the grain type and particle size you plan to run, the daily output target and the shift pattern your plant operates. Confirm the local voltage and frequency so the MCC and PLC panels are wound correctly before the line leaves the factory. If you have an existing dryer or packing system that the new line must integrate with, send the interface dimensions and throughput so the upstream stations are sized to match.
Frequently Asked Questions
Q: How is screw configuration and die design selected for different grain blends and target flake density?
A: The screw element arrangement — conveying, kneading and reverse segments — is laid out to deliver the shear and residence time that each grain blend requires for full starch gelatinisation. The die aperture is then matched to the pellet size that the flaking rollers will flatten into the target flake thickness and density.
Q: What barrel temperature profile and moisture level produce the correct starch gelatinisation for corn flakes?
A: Barrel zones are staged so the dough heats gradually from the feed end, reaching full gelatinisation before the die without premature moisture flash-off. Moisture content at the die is held within a narrow window so the pellet stays plastic enough to flatten under the rollers without sticking or tearing at the edges.
Q: How is line throughput matched between extruder output, flaker capacity and roaster residence time?
A: Each station’s capacity is calculated against the others during layout design so that pellet flow into the flaking rollers and oven belt speed both accommodate the extruder’s actual output on your grain, preventing upstream pile-ups or under-loaded roasting chambers.
Q: Can a trial run on my raw material be conducted before shipment to verify expansion and flake quality?
A: Yes, your grain is run through the extruder, flaking station and a bench-scale roaster in the in-house testing workshop. The trial locks the screw configuration, barrel temperature curve and roller gap before the line is crated, so product development is not deferred to your factory floor.