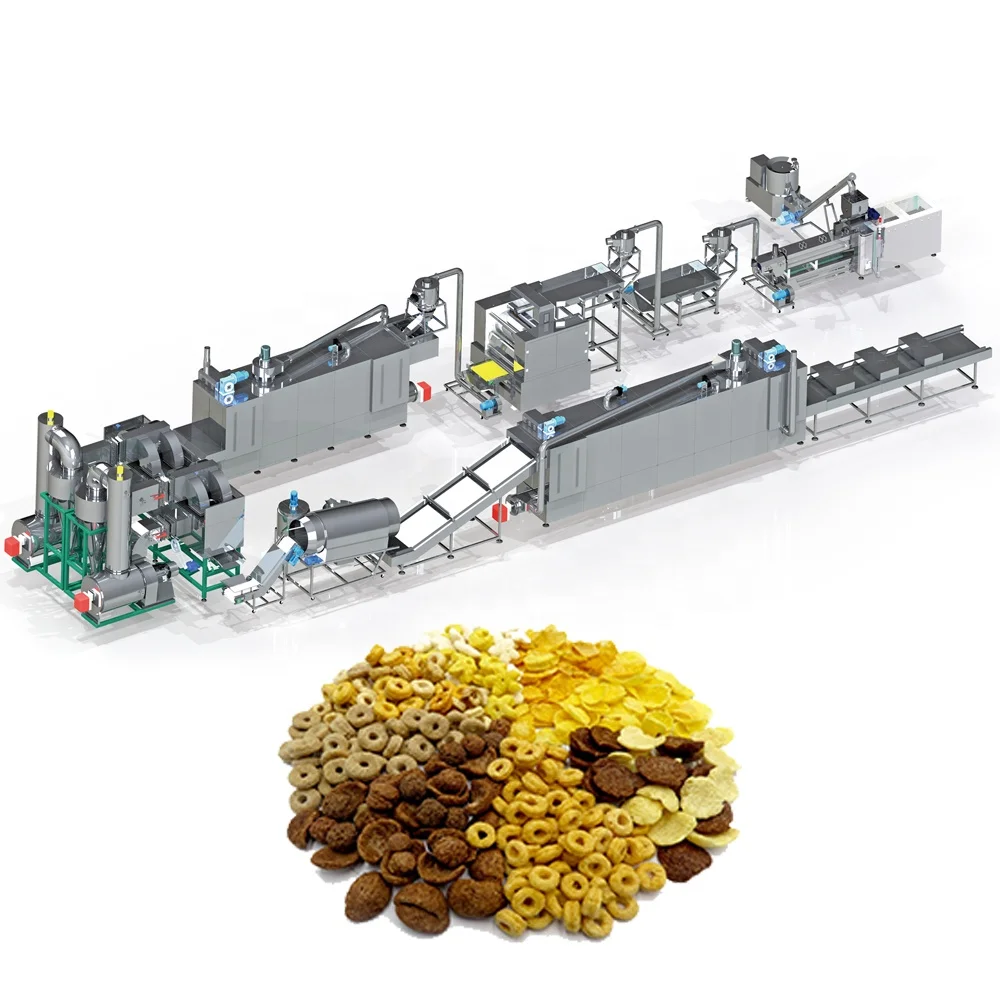
Extrusion Process Control — screw configuration and barrel temperature profiles specified to your corn formulation before the corn flakes extrusion production line specifications are finalized.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-65 (MT-70 / MT-75 / MT-85 also available) |
| Product Type | Corn Flakes Production Line |
| Extruder Type | Twin screw, co-rotating with modular screw segments |
| Installed Power | 84 kW (MT-65 line) |
| Real Power Consumption | 59 kW (MT-65 line) |
| Output Capacity | 120–150 kg/h (basis not stated in source — confirm raw material, moisture and flake thickness) |
| Overall Dimensions | 12000 × 1200 × 2200 mm (MT-65 line) |
| Mixer Tank Size | φ600 × 500 mm |
| Mixer Power | 4 kW |
| Corn Flakes Press Machine Power | 16.12 kW |
| Press Machine Roller | 510 × 310 × 1050 mm |
| High-Temperature Oven Size | 4.5 × 1.4 × 1.8 m |
| Oven Heat Source | Gas, dual-side baking system |
| Sugar Spraying System Dimension | 4000 × 1900 × 1880 mm |
| Sugar Spraying System Roller Size | Ø600 × 2700 mm |
| Gearbox Lubrication | Oil forced automatic lubrication system |
| Cutting System | Non-stop cutting system |
| Extruder Self-Cleaning | Yes |
| Standards | CE (certified since 2014), ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional corn flakes | Corn grits, corn flour with sugar and malt coating |
| Multi-grain breakfast cereals | Rice flour, wheat flour and oat blends |
| Fortified flaked cereals | Vitamin premix blended grain bases requiring uniform flake geometry |
| Core-filled snacks | Soya bean, peanut, walnut and chocolate fillings |
| Standard puffed snacks | Corn and rice-based formulations in various shapes |
What "120–150 kg/h" Actually Depends On
Capacity on a corn flakes extrusion production line specifications sheet only holds when screw geometry, moisture content and die design match your exact raw material.
I spent five days on a customer site in Southeast Asia recalibrating an entire line because their corn flour carried a fat content our standard configuration could not handle. The flakes came out thick, dense, and refused to crisp up in the oven. We had to rebuild the screw module sequence and open the die gap before the extruder could gelatinise starch properly at the throughput they expected. When a line ships without a trial run on the buyer’s actual formulation, the nominal capacity figure becomes meaningless [NEED_CITE: starch gelatinisation behaviour under varying fat content in twin-screw extrusion].
Screw Module Sequencing and Starch Gelatinisation
The MT-65 uses co-rotating twin screws built from sectional modules, meaning each segment can be swapped to adjust shear intensity and residence time. Corn grits require a different shear profile than fine corn flour — grits need more mechanical energy in the compression zone to break down particle structure, while flour demands gentler handling to prevent over-gelatinisation. This corn flakes extrusion production line specifications configuration allows operators to tune the screw arrangement so that starch gelatinises at the correct barrel zone rather than too early or too late in the process.
Barrel Temperature Zones and Die Geometry
Each barrel section heats independently, creating a temperature gradient that drives moisture migration and expansion. The die plate at the discharge end shapes the extrudate into a rope or sheet that feeds directly into the flaking press. Die aperture size and land length control backpressure inside the barrel — tighter dies increase pressure and produce denser extrudate, which translates to a harder final flake. Matching die design to the press roller gap setting is critical [NEED_CITE: die land length effect on extrudate density in breakfast cereal production].
Reading the Power and Dimension Figures
The 84 kW installed power versus 59 kW real consumption gap reflects typical motor oversizing for start-up torque and peak-load buffer. The overall line footprint of 12 metres in length means buyers need to confirm floor space and utility routing before installation. The press machine draws 16.12 kW through a separate controller box, which isolates its speed and gap adjustment from the main extruder PLC loop — this matters when operators need to adjust flake thickness without interrupting extruder throughput. The large-diameter flaking roller includes a cooling circuit to prevent the extrudate from sticking during compression.
The Cost of Skipping the Trial Run
A line that arrives on site with a generic screw build forces the buyer into a costly commissioning period. Operators spend days running material through the extruder, adjusting barrel temperatures and swapping screw elements, burning raw material and energy with every failed batch. Flakes that come out too dense or too thin cannot be corrected downstream — the problem originates inside the barrel. I have watched production teams lose an entire first week to this process because no one ran the buyer’s grain blend before the machine left the factory [NEED_CITE: commissioning delays caused by unmatched extruder screw configuration].
Why This Line Ships Ready for Your Formulation
Every MT-65 line is configured around the buyer’s raw material, not a default build. Screw modules and die plates are selected based on your corn source, moisture range and target flake density. Before shipment, the line runs your actual grain blend in the testing workshop, producing sample flakes that confirm throughput, texture and oven behaviour. The press machine and gas oven are sized so that no single station bottlenecks the others — the dual-side gas baking system and the Ø600 × 2700 mm coating drum are matched to the extruder’s output range. Gearbox oil forced lubrication extends continuous run intervals, reducing unplanned downtime during peak production schedules.
Documentation & Verification
- Line layout and capacity calculation matched to your corn blend and target flake thickness
- Screw and die configuration record documenting module sequence and die aperture for your formulation
- Trial run report produced on your raw material in the testing workshop before shipment
- Electrical schematic confirming voltage, frequency and control language for your market
- Operation and maintenance manual covering press roller gap adjustment and extruder self-cleaning procedure
- Wear parts list identifying screw segments, die plates and flaking roller bearings for reorder planning
Installation, Commissioning & Support
- Floor plan must accommodate the 12-metre line length plus material staging and access clearance
- Separate electrical circuits required for the 84 kW extruder system and the 16.12 kW press machine
- Gas supply line and exhaust routing planned for the 4.5-metre high-temperature oven before equipment arrival
- First run supervised on-site with barrel temperature profiling and press roller gap calibration to your product
- Operator training covers screw module changeover, self-cleaning cycles and oil lubrication system checks
- Spare screw segments, die plates and flaking roller bearings supplied with initial shipment package
What to Include in Your Inquiry
To configure a corn flakes extrusion production line specifications package for your plant, share the grain type and particle size you intend to process, along with target flake thickness and daily output volume. Specify your local voltage, frequency and preferred control panel language. If you already run upstream mixing or downstream packing equipment, note the interface requirements so the line layout accounts for existing conveyors and storage bins.
Frequently Asked Questions
Q: How is screw configuration selected for different raw materials like corn grits versus rice flour blends?
A: Each screw module controls shear and residence time in a specific barrel zone. Corn grits require higher compression energy to break down particle structure, so kneading blocks are placed earlier in the sequence. Rice flour gelatinises at lower temperatures, so conveying elements dominate and compression zones are shortened. The configuration record documents every module position for your specific grain source.
Q: What barrel temperature profile and moisture range produce the target flake density?
A: Typical corn flake production requires barrel zones ramping from around 60°C at the feed section to above 120°C near the die, with feed moisture adjusted between 18% and 24%. The exact profile depends on starch content and particle size. During the trial run, we map temperature against extrudate density to find the operating window that delivers consistent flake crispness after oven baking.
Q: How is output capacity verified on the buyer’s actual raw material before shipment?
A: The testing workshop runs your grain blend through the configured extruder, press and oven at sustained production speed. We measure throughput in kg/h, record flake thickness and moisture after baking, and document the screw and die settings that achieved those results. This trial run report ships with the line so operators can replicate the conditions from day one.
Q: How does the flaking press roller gap interact with extruder die design to control final flake thickness?
A: The die produces extrudate ropes or pellets at a specific diameter and density. The press roller then compresses these into flakes — a wider gap yields thicker flakes, while a narrower gap produces thinner, more brittle ones. Die aperture and roller gap must be matched; an oversized die feeding a tight gap causes edge cracking and uneven moisture loss during baking.