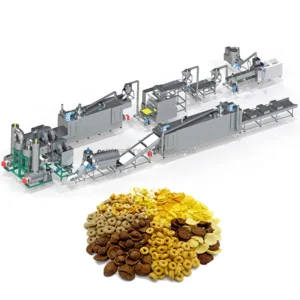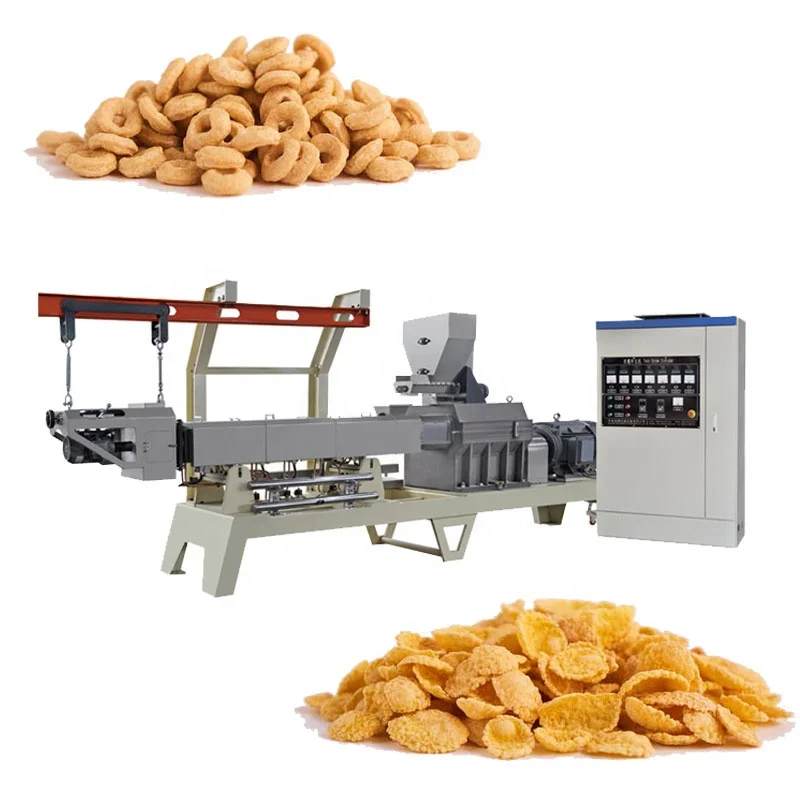
Modular Screw Architecture — Twin-screw sections are sequenced and tested against your actual corn grits or flour blend before shipment, not assembled from a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-65, MT-70, MT-75, MT-85 |
| Product Type | Corn Flakes Production Line / Breakfast Cereal Extrusion Line |
| Screw Type | Co-rotating twin screw, sectional modules |
| Line Stations | Mixer → screw conveyor → twin screw extruder → air conveyor → dryer → hoister → flavoring drum and oil sprayer → cooling machine → packing machine |
| MT-65 Installed / Real Power | 84 kW / 59 kW |
| MT-65 Output | 120–150 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| MT-65 Dimension | 21000 × 1200 × 2200 mm |
| MT-70 Installed / Real Power | 132 kW / 92 kW |
| MT-70 Output | 200–250 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| MT-70 Dimension | 23000 × 1500 × 2200 mm |
| MT-75 Installed / Real Power | 186 kW / 140 kW |
| MT-75 Output | 400–500 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| MT-75 Dimension | 24000 × 1500 × 2800 mm |
| MT-85 Installed / Real Power | 239 kW / 167 kW |
| MT-85 Output | 300–400 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| MT-85 Dimension | 28000 × 3500 × 4300 mm |
| Corn Flakes Press Machine | Stainless steel, big roller pressing, adjustable roller gap, integrated cooling, separate controller box, 16.12 kW, 1550 × 1300 × 2000 mm |
| High-Temperature Oven | Gas-fuelled, both-side baking system, 3.75 kW, 4500 × 1400 × 1800 mm |
| Control System | PLC and MCC (voltage, frequency and interface language to be confirmed per site) |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional corn flakes production | Corn grits or corn flour at controlled moisture |
| Rice-based breakfast flakes | Rice flour or rice grits blends |
| Multi-grain cereal flakes | Wheat, oat, barley, millet combinations |
| Fortified breakfast cereal | Grain flour blended with vitamin and mineral premix |
| Puffed cereal snack variants | Corn, rice or mixed grain bases in pellet or direct-expanded format |
Why "Nominal Output" Means Nothing Without Your Raw Material
A capacity number only holds when screw configuration, barrel profile and moisture are matched to the starch behaviour of your specific grain blend.
I once watched a corn flakes line ship out to a Southeast Asian site with a quoted throughput that looked solid on paper. The problem surfaced during the first week of production: the corn grits the buyer sourced locally had a coarser particle size distribution than the flour used during factory testing. Starch gelatinisation dropped, the pressed flakes came out dense, and after baking they cracked at the edges and sank straight to the bottom of the milk bowl. The first production batch was returned by the retail buyer. [NEED_CITE: starch gelatinisation degree and particle size correlation in cereal extrusion]
That failure had nothing to do with the extruder’s motor power or the oven’s temperature range. It came down to screw shear segments that were not reconfigured for a different grit size, and a barrel temperature profile calibrated to a different moisture curve. When corn flakes extrusion technology is discussed only in terms of kilograms per hour, the real variables that determine flake quality get buried.
Screw Module Sequence and Starch Gelatinisation Control
The co-rotating twin screw in each MT model uses sectional modules that can be rearranged along the shaft. Forward-conveying elements, kneading blocks and reverse-screw segments are positioned in a sequence that determines how long material stays in each barrel zone and how much mechanical shear it receives. For corn flakes extrusion technology, the balance between shear-driven cooking and residence time directly sets the gelatinisation degree of the starch — too low and the flake lacks structure after pressing, too high and the pellet over-expands before it reaches the roller.
Barrel Temperature Profile Across Heating Zones
Each barrel zone has independent heating and cooling, allowing a gradient that typically ramps from preconditioning temperatures in the feed section through peak cooking temperatures in the metering zone. The exact profile must be matched to the grain’s starch type: corn starch gelatinises at a different temperature window than wheat or oat starch, and multi-grain blends require compromise settings. When the profile is wrong, the pellet exits the die with uneven moisture distribution, and the flaking press cannot produce a consistent thickness. [NEED_CITE: barrel zone temperature profiling for multi-grain breakfast cereal extrusion]
Interpreting Power, Press Gap and Oven Capacity
The installed versus real power figures across the four models reflect the difference between motor nameplate rating and actual energy drawn during steady-state extrusion. For a process engineer comparing breakfast cereal twin-screw extrusion options, the real power number is the one that matters for utility planning and transformer sizing. The corn flakes press machine uses an adjustable roller gap with a separate controller box, so flake thickness can be dialed in independently of extruder speed. The gas-fuelled high-temperature oven bakes from both sides, which matters because single-sided heat creates curl and uneven colour — common defects that buyers attribute to the extruder when the fault sits downstream. Line throughput is only as fast as the slowest station, and oven baking time is typically the constraint that sets the ceiling.
When Screw Configuration Is Copied, Not Specified
A generic screw build might produce acceptable flakes on the supplier’s test flour, but it will not compensate for differences in your raw material’s particle size, fat content or moisture absorption rate. The consequence is not a machine that fails to run — it is a machine that runs steadily while producing flakes that sink in milk, shatter during packing or stale within days on the shelf. [NEED_CITE: flake density and bowl-life correlation in breakfast cereal quality standards]
Process engineers who inherit a line with a copied configuration face a choice: reconfigure the screw modules and re-profile the barrel zones based on lab analysis of the local grain supply, or accept a product that does not meet the texture and density specifications the market expects. The reconfiguration is straightforward when the extruder uses sectional modules; it becomes impossible with a fixed-screw design.
Why Procurement for Extrusion Lines Works Differently Here
Complete lines from batching through packing are supplied under one source, so throughput at every station — mixer, extruder, dryer, press, oven, cooler — is calculated against the same raw material and target flake specification rather than assembled from independent vendors who each size their equipment to a generic duty point.
Screw configuration and die geometry are specified to the buyer’s actual grain blend and target flake density, documented in a configuration record that ships with the machine.
An in-house testing workshop runs trial production on customer-supplied raw material before the line is dispatched, generating a trial run report that covers actual throughput, gelatinisation results and flake quality data.
Electrical schematics, voltage and frequency are confirmed against the buyer’s site standard, and PLC interface language is locked before production begins — eliminating the commissioning delays that occur when control panels arrive with the wrong language or voltage rating.
Documentation & Verification
- Line layout drawing with capacity calculation matched to your grain type and target flake thickness
- Screw and die configuration record showing module layout specified to your raw material
- Trial run report on your actual corn grits or flour blend covering output, gelatinisation and flake density
- Machine specification sheet confirming every station’s throughput match across the full line
- Electrical schematic with voltage, frequency and control language confirmed for your site
- CE declaration of conformity and ISO certificate included in the shipping documentation package
Installation, Commissioning & Support
- Foundation plan accounts for the MT-85’s 28-metre line length and 4300 mm height clearance requirement
- Electrical room must supply confirmed voltage and frequency with dedicated circuits for the 167 kW real-power draw on the MT-85 extruder
- Modular station delivery allows phased installation, with the extruder and dryer positioned first for early utility connection
- Commissioning includes screw module verification and barrel zone calibration on your raw material before handover
- Operator training covers PLC interface navigation, press roller gap adjustment and oven temperature profiling for your recipe
- Wear parts list identifies screw elements, die inserts and press roller bearings with recommended replacement intervals
What to Include with Your Inquiry
To configure the extrusion section accurately, we need the specific grain type and particle size distribution you will be running, the target flake thickness and density, and the moisture content of your raw material at the mixer stage. Share your site’s voltage, frequency and preferred control language so the electrical package is built correctly from the start. If you have an existing dryer or packing system that the line needs to integrate with, include those specifications so station throughput can be matched end to end.
Frequently Asked Questions
Q: How is screw configuration selected for corn versus wheat or multi-grain breakfast cereal recipes?
A: Each grain has a different starch gelatinisation temperature and shear sensitivity. Corn requires higher barrel zone temperatures and moderate kneading-block intensity, while wheat tolerates more shear but needs lower peak heat. For multi-grain blends, the screw module sequence is balanced to reach an average gelatinisation degree that holds all components together without over-processing the most heat-sensitive grain. The configuration is documented and can be adjusted as your recipe evolves.
Q: What barrel temperature profile produces the correct gelatinisation for a crispy flake without over-browning in the oven?
A: The profile typically ramps gradually through the feed and compression zones, peaks in the metering section at a temperature matched to your grain’s starch window, then drops slightly before the die to control expansion. If the peak is too high, the pellet exits with residual sugars that caramelise excessively in the oven, causing dark edges. The correct profile gives a pale pellet that browns evenly during baking. [NEED_CITE: temperature profiling methodology for breakfast cereal extrusion]
Q: How do you verify that the line’s real output matches the quoted capacity on my specific flour or grits blend?
A: We run a trial in the testing workshop using your raw material before shipment. The trial covers extruder throughput at steady state, gelatinisation degree measurement, pellet moisture at the die, and pressed flake density and thickness. Results are compiled in a trial run report so you can confirm output and quality before the line leaves the factory.
Q: How does die geometry interact with the flaking press roller gap to control final flake thickness and density?
A: The die aperture determines pellet diameter and initial density. Larger apertures produce thicker pellets that require more roller compression, which increases internal stress and can cause edge cracking after baking. The press roller gap is set relative to the pellet size so that the flake reaches target thickness without exceeding the material’s fracture limit. Both parameters are adjusted together during commissioning.
Q: Can we run a trial on our own raw material before the line ships, and what does the trial report cover?
A: Yes. Send a representative sample of your grain blend to the testing workshop. The trial produces extruded pellets and finished flakes on the same screw and die configuration that will ship with your line. The report documents throughput, barrel zone temperatures, screw speed, gelatinisation percentage, flake thickness, density and bowl-life observations, giving you a baseline to compare against once the line is installed at your site.