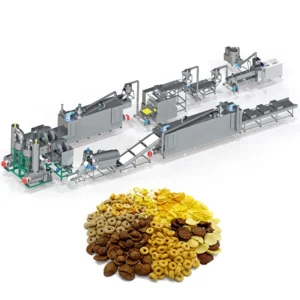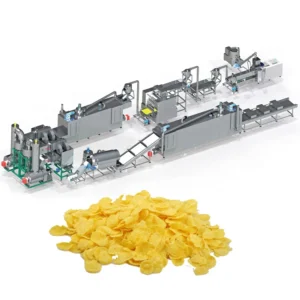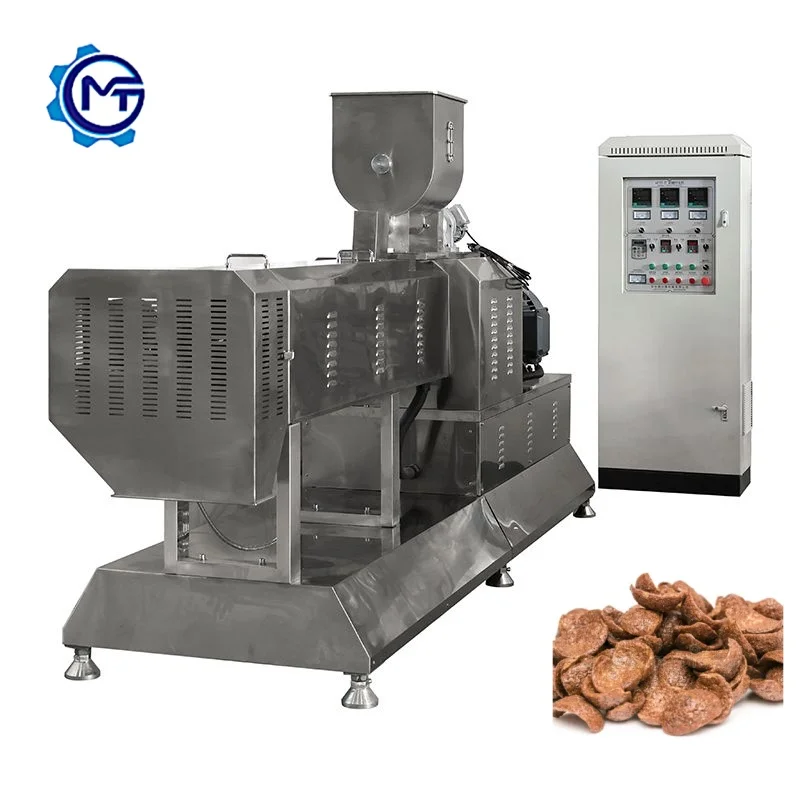
Matched Screw Profile — Every MT70, MT85 and MT75 build ships with a screw configuration and die geometry documented against the buyer’s actual flour blend and target flake density.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes and Breakfast Cereal Extrusion Production Line |
| Screw Type | Twin-screw |
| Available Models | MT70, MT85, MT75 |
| MT70 Installed Power / Consumption | 160 kW / 120 kW |
| MT85 Installed Power / Consumption | 190 kW / 140 kW |
| MT75 Installed Power / Consumption | 210 kW / 150 kW |
| MT70 Output Capacity | 150–200 kg/h (basis not stated in source — confirm raw material / moisture content / product format) |
| MT85 Output Capacity | 300–400 kg/h (basis not stated in source — confirm raw material / moisture content / product format) |
| MT75 Output Capacity | 300–500 kg/h (basis not stated in source — confirm raw material / moisture content / product format) |
| MT70 Overall Dimensions | 41 × 1.5 × 2.2 m |
| MT85 Overall Dimensions | 43 × 1.5 × 3.2 m |
| MT75 Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC control, MCC |
| Flaking Machine | Hydraulic double-roller, PLC control, infrared sensor temperature control, dual motor drive |
| Dryer Heating Source | Gas / Electric / Steam (multi-fuel option) |
| Hot Air Roasting Oven | Vibrating pan, dual circulating fans, cyclone dust removal, precise temperature control |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Final Products | Natural corn flakes, sugar-coated corn flakes, shaped cereals (ball, tube, stick, ring, fruit loop, star, wheel, flower, heart) |
| Standards | CE certified, ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | Corn grits or corn flour base |
| Sugar-coated breakfast cereal | Corn, rice or multi-grain blend with sugar slurry coating |
| Multi-grain cereal processing | Wheat, oat, barley blended with corn or rice powder |
| Shaped puffed cereal formats | Same base materials extruded through profile dies (ring, star, wheel) |
| Fortified breakfast cereal | Grain base with vitamin and mineral premix addition |
What the Nominal Capacity Number Hides About Your corn flakes extrusion production line screw configuration barrel temperature die design
The throughput on the brochure assumes a reference flour at a reference moisture — your formulation may behave entirely differently inside the barrel.
I remember a commissioning visit where the extruder ran fine on standard corn grits during the factory test, but the moment the buyer switched to a blend cut with oat and barley, the dough viscosity shifted, the barrel back-pressure climbed, and the flakes came off the roller too thick to toast evenly. The machine was not wrong. The specification was. A corn flakes extrusion production line screw configuration barrel temperature die design built around one recipe will struggle the first day a second recipe enters the hopper, and the gap between quoted output and actual sustained output is where most disputes start [NEED_CITE: common causes of throughput shortfalls on cereal extrusion lines].
Barrel Zone Temperature and Starch Gelatinisation
The barrel on this line is divided into independently heated zones. Getting the profile right means the starch in your corn or multi-grain blend reaches full gelatinisation without over-expanding before it hits the die. Too much heat too early and the dough flashes into steam inside the barrel; too little and the flake stays raw-tasting and breaks during roasting. The corn flakes extrusion production line screw configuration barrel temperature die design is adjusted zone by zone during the trial run, and the final settings are recorded in the configuration document that ships with the line.
Die Geometry and Flake Density
The die is the last restriction the dough sees before the knife cuts it into pellets. Its channel length and outlet diameter together determine how much the pellet expands, and that expansion sets the density of the flake after rolling and roasting. A pellet that expands too much produces a flake that floats in milk and dissolves too fast for the bowl-life the market expects. The die on each build is specified to the buyer’s target density, not pulled from a generic catalogue [NEED_CITE: relationship between die L/D ratio and cereal pellet expansion].
Reading the Spec Sheet Against Your Own Recipe
Installed power and consumption figures — 160 kW / 120 kW on the MT70, up to 210 kW / 150 kW on the MT75 — tell you the thermal and mechanical headroom available. What they do not tell you is how much of that energy your specific flour blend will absorb. High-fat formulations demand different screw shear than lean corn grits, and a vitamin premix may degrade if the barrel residence time is too long. The dimension envelope (41 m to 45 m line length depending on model) also governs how many drying and roasting passes you can fit, which directly affects final moisture content and shelf stability. Twin-screw operation gives you independent control over feed rate and screw speed, so adjusting one recipe does not force you to re-gear the main drive.
When the Wrong Configuration Reaches Your Floor
A screw profile copied from a standard build may produce flakes that are too dense to crisp during roasting, or too fragile to survive the coating drum. Either way, the output fails the pack-weight check and the rejection rate climbs through the first production weeks. I have watched lines sit idle while replacement screw elements are machined and shipped across borders — downtime that could have been caught by a single week of trials on the actual flour [NEED_CITE: cost of unplanned downtime on food processing lines].
Why Buyers Specify This Line for Extrusion-Critical Cereal Work
Screw configuration and die design are documented against your raw material before production starts, not guessed from a previous customer’s order. The in-house testing workshop runs your flour blend through the extruder and flaker, and the trial run report records throughput, expansion ratio and flake density before the line is approved for shipment. PLC and MCC control are programmed to the confirmed voltage and frequency of the destination country, so the cabinet labels and HMI language match the operators who will use them. The hot air roasting oven uses dual circulating fans and a cyclone dust collector to keep surface blistering consistent across the full pan width, and the hydraulic flaking unit holds roller gap with infrared temperature feedback to prevent sheet-thickness drift during long shifts. Every station — mixer, extruder, flaker, dryer, roaster, coater, cooler — is sized so throughput matches rather than bottlenecks at one point.
Documentation & Verification
- Screw and die configuration record specifying profile, L:D arrangement and die geometry for your flour blend
- Trial run report documenting throughput, expansion and flake density on your raw material
- Line layout and capacity calculation matching throughput across every station
- Electrical schematic with voltage, frequency and control language confirmed to your market
- CE declaration of conformity and ISO certificate for customs and regulatory filing
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Foundation plan references the 41–45 m line length to confirm bay length and utility trench positions
- Electrical room must supply three-phase power at confirmed voltage for the 120–150 kW consumption range
- PLC and MCC panels arrive pre-wired; on-site connection limited to field devices and utility hook-ups
- Commissioning includes barrel temperature profiling and screw speed tuning on your production flour
- Operator training covers die changeover, roller gap adjustment and roasting oven fan balance
- Wear parts list identifies screw elements, die inserts and roller bearings with recommended stock quantities
What We Need to Quote Accurately
Send the exact flour blend — including any oat, barley, rice or premix fractions — along with target flake thickness and bowl-life expectation. Confirm the local voltage, frequency and whether the control language needs to match a specific operator group. If you are switching from an existing line, share the current screw profile so the trial can be benchmarked against your baseline.
Frequently Asked Questions
Q: How is screw configuration determined for different raw materials and moisture levels?
A: We start from your flour analysis — starch content, protein, fat and fibre — and the moisture you plan to condition to. Screw elements are selected for the shear and residence time that gelatinise your specific blend without over-cooking. The configuration is validated in the testing workshop on your material before the production build is locked in.
Q: What barrel temperature profile is needed for full starch gelatinisation without over-expansion?
A: Each zone is tuned during the trial run. Corn-based blends typically need a stepped ramp that peaks before the die, while oat-heavy mixes require a flatter profile to avoid gumming. The final settings are recorded in the configuration document so your operators can restore them after any recipe change.
Q: How does die design affect flake density and whether the product sinks or floats in milk?
A: The die channel length and outlet diameter control how much the pellet expands before cutting. Greater expansion produces a lighter flake that floats; less expansion yields a denser flake that stays submerged longer. We specify the die to the bowl-life your brand promises and verify it during the trial.
Q: Can I run a trial on my own flour blend before ordering?
A: Yes. The in-house testing workshop runs your exact material through the extruder and flaker. You receive a trial run report with throughput, expansion ratio and flake density data, and the screw and die configuration is adjusted if the results fall outside your specification.