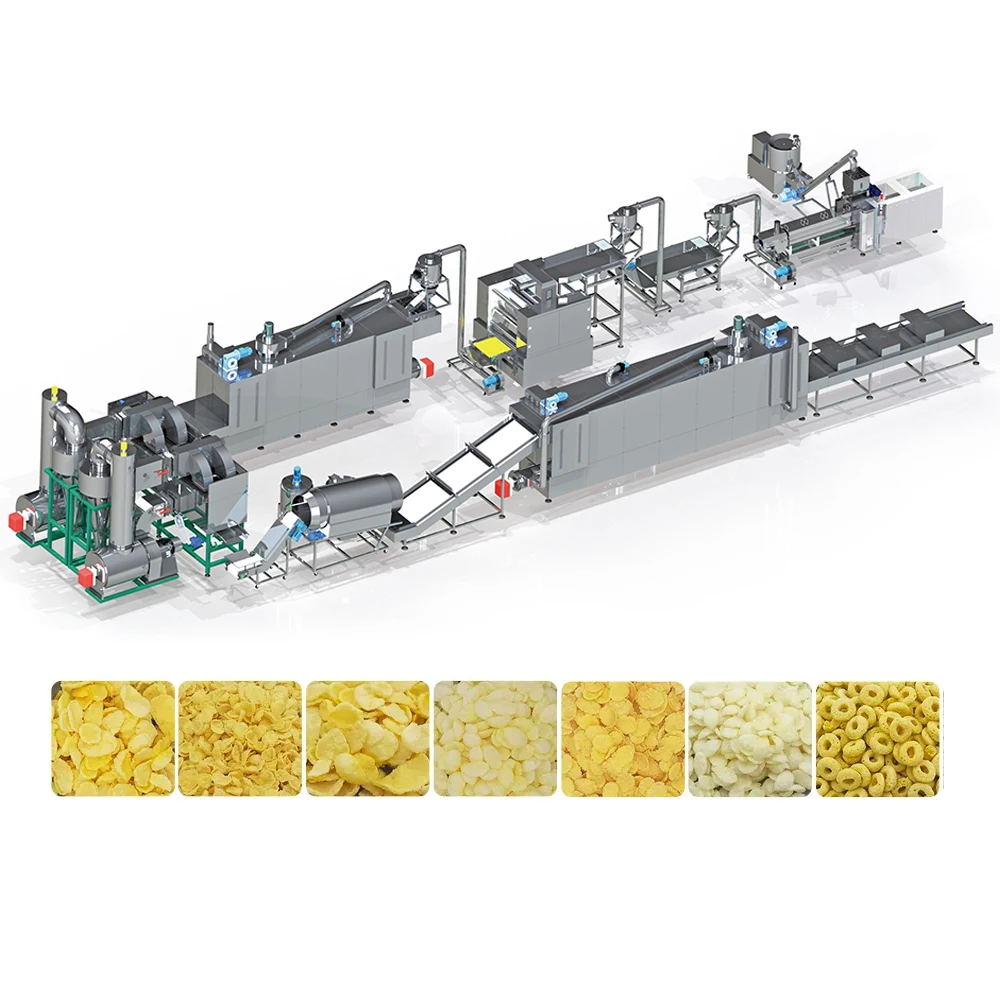
Screw configuration specified to grain formulation — each corn flakes extrusion build starts with the buyer’s actual flour blend and target density, not a copied template.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Breakfast Cereal Processing Production Line |
| Extruder Model | MT-65 |
| Screw Type | Co-rotating twin-screw, sectional modules |
| Extruder Functions | Forward/backward transport, mixing, de-gassing, cooking, forming |
| Mixer Output | 10–30 kg per load |
| Mixer Power | 4 kW |
| Mixer Tank Size | φ600 × 500 mm |
| Mixer Structure | Stainless steel, food-grade contact parts |
| Screw Conveyor Power | 0.75 kW |
| Screw Conveyor Feature | Sealed stainless steel roller, vibrating sifter for stable feeding |
| Corn Flakes Press Machine Power | 16.12 kW |
| Corn Flakes Press Roller Size | 510 × 310 × 1050 mm |
| Press Feature | Big roller, integrated cooling system, adjustable roller gap for flake thickness |
| High-Temperature Oven Size | 4.5 × 1.4 × 1.8 m |
| Oven Heating | Gas-fired, both-side baking system |
| Sugar Spraying System Power | 28.75 kW |
| Sugar Spraying Roller Size | Ø600 × 2700 mm |
| Sugar Spraying Components | Conveyor, melting tank, temperature-keeping roller |
| Line Stations | Flour Mixer → Screw Elevator → Twin-screw Extruder → Elevator → Dryer → Elevator → Coating Line → Vibrating Spreader → Elevator → Dryer → Cooling Conveyor |
| Control System | Separate controller box for press; MCC/PLC across line |
| Voltage & Frequency | Configurable (e.g., 3ph 380V 50Hz, 3ph 415V 60Hz, 3ph 220V 60Hz) |
| Output Capacity | Basis to be confirmed on buyer’s raw material and flake specification |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional corn flakes | Maize flour, corn grits at varying moisture levels |
| Multi-grain breakfast cereals | Rice flour, oat flour, blended grain powders |
| Nutritionally fortified cereals | Grain base with vitamin and mineral premix additions |
| Sugar-coated or honey-coated flakes | Plain flakes passed through coating drum with syrup |
| Shape variants | Ring, ball, star, stick forms via die and mould changeover |
| Leisure snack crossovers | Coated cereal pieces packaged for snack-market distribution |
Why a Generic Screw Profile Ruins Flake Density
The corn flakes extrusion production line screw configuration must match your flour’s starch behaviour, or no amount of downstream adjustment will fix the texture.
A copied screw build designed for standard corn meal often fails when the buyer’s local grain carries higher fat or different particle sizing. The result is pellets that press into flakes that are either too dense to crisp properly or too fragile to survive coating and packing. I have watched lines ship out with a one-size-fits-all screw arrangement and then need days of on-site rework to stabilise flake density. Every corn flakes extrusion production line screw configuration should be validated on the buyer’s own flour before the extruder leaves the factory [NEED_CITE: starch gelatinisation behaviour across grain varieties].
Gelatinisation Window and Barrel Temperature Profile
Starch gelatinisation in corn flour demands a specific moisture and temperature window inside the barrel. The sectional screw modules on the MT-65 allow the transport, mixing, de-gassing, cooking, and forming zones to be tuned independently so that the gelatinisation point is reached at the right barrel position. When the profile is off, the dough either exits under-cooked — producing hard, glassy flakes — or over-cooked, causing sticky pellets that jam the flaking press. Getting this window right is the single biggest factor in achieving consistent flake crispness batch after batch.
Press Roller Gap and Flake Thickness Control
The flaking press sits between the extruder and the high-temperature oven, and its job is to flatten cooked pellets to a precise thickness. The adjustable roller gap on the 510 × 310 × 1050 mm roller set determines whether flakes finish at a delicate breakfast-cereal gauge or a thicker snack format. An integrated cooling system stabilises pellet temperature before pressing, preventing the dough from smearing across the roller face. Without that cooling stage, warm pellets can deform unevenly, and the resulting thickness variation shows up as inconsistent browning in the oven [NEED_CITE: roller gap tolerance and flake uniformity in cereal processing].
Oven Baking and Moisture Removal
The gas-fired, both-side baking oven measures 4.5 × 1.4 × 1.8 m, providing enough residence length for gradual moisture removal. Both-side heat application prevents the common fault of flakes that are dry on the surface but retain a damp core — a defect that leads to sogginess once the product sits in the bowl. The baking stage also develops the colour and toasted flavour profile buyers expect from a premium corn flake.
The Cost of Skipping Raw-Material Validation
When a line ships without a trial run on the buyer’s actual flour, problems surface during commissioning. Flakes may stick to the press rollers, expansion may fall short, or the final moisture after baking may drift outside specification. Resolving these issues on-site means reconfiguring screw elements, adjusting barrel moisture injection, and re-tuning oven residence time — all while the production schedule slips. A corn flakes extrusion production line screw configuration that was never tested against real material is essentially an unverified hypothesis [NEED_CITE: on-site commissioning delays from untested extrusion parameters].
Why Source This Line Here
Screw and die geometry is specified against the buyer’s grain formulation and target flake density, not pulled from a standard catalogue. The in-house testing workshop runs trial batches on customer-supplied raw material so that gelatinisation, expansion, and flake thickness are confirmed before shipment. Throughput across the mixer, extruder, press, dryer, and coating stations is calculated to prevent bottlenecking at any single point. Electrical schematics and control language are locked in during the specification stage, matching the buyer’s local voltage and operator requirements. Pre-sales consultation through installation, commissioning, and ongoing wear-part support stays with one supplier from start to finish.
Documentation & Verification
- Screw and die configuration record matched to your grain blend and target flake density
- Trial run report on customer-supplied raw material from the in-house testing workshop
- Line layout and capacity calculation confirming station-to-station throughput balance
- Electrical schematic with voltage, frequency, and control language confirmation for your market
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Operation and maintenance manual with wear parts list specific to your line configuration
Installation, Commissioning & Support
- Floor plan and utility layout provided for the full station sequence from mixer to cooling conveyor
- Voltage and frequency confirmed before production to match local supply (e.g., 3ph 415V 60Hz)
- Separate controller box for the press machine simplifies wiring and troubleshooting on site
- Gas-fired oven requires dedicated gas supply line and exhaust ducting per local code
- Operator training covers screw element changeover, roller gap adjustment, and PLC parameter recall
- Wear parts list covers screw modules, die plates, and press roller surfaces for first reorder cycle
What We Need to Configure Your Line
Share your grain formulation — maize, rice, oat, or a multi-grain blend — along with the target flake thickness and whether you plan to run plain, sugar-coated, or honey-coated variants. Your local voltage and frequency, workshop dimensions, and preferred control language help us finalise the electrical and layout package. If you can send a sample of your production flour, we will run a trial in the testing workshop and include the results with the proposal.
Frequently Asked Questions
Q: How is screw configuration and die design matched to my grain formulation and target flake density?
A: We review your flour composition, particle size, and fat content, then select screw element types, pitch sequence, and die geometry to hit the correct gelatinisation and expansion point. A trial run on your raw material validates the corn flakes extrusion production line screw configuration before the extruder ships, so you receive a documented build record rather than a generic assembly.
Q: What barrel temperature profile and moisture level are needed for proper starch gelatinisation in corn flakes?
A: The required profile depends on your specific grain blend and moisture content at the mixer stage. Sectional screw modules and barrel heating zones are adjusted during the trial run to locate the gelatinisation window. The confirmed temperature and moisture parameters are recorded and provided to your operators as baseline settings for production start-up.
Q: How do I verify that the flaking press roller gap produces the correct flake thickness for my market?
A: During the factory trial, we run extruded pellets through the press at several gap settings and measure resulting flake thickness with a micrometer. The setting that meets your specification is documented in the trial report. The adjustable roller gap and integrated cooling system let your operators reproduce that thickness consistently during daily production.
Q: Can the line handle both plain and sugar-coated cereal variants on the same equipment?
A: Yes. The coating line includes a sugar spraying system with a melting tank and temperature-keeping roller that can be engaged or bypassed. Switching between plain and coated runs involves routing flakes through or around the coating drum and adjusting syrup temperature. No additional extruder or oven hardware change is required.
Q: Is a trial run on my raw material available before shipment to confirm product texture and expansion?
A: The in-house testing workshop conducts trial runs using your supplied flour before any line leaves the factory. The trial report covers extrusion behaviour, pellet condition, flake thickness after pressing, and final crispness after baking. This step ensures the corn flakes extrusion production line screw configuration and downstream settings are verified against your actual production input.