
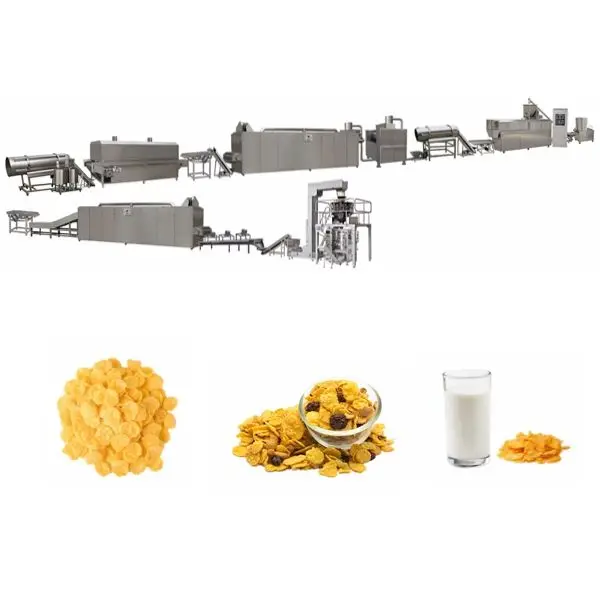
Screw geometry matched to your cereal blend — Every MT70 barrel zone and die land length is dimensioned after reviewing your specific corn, rice, or multi-grain formulation rather than copied from a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 |
| Product Type | Corn Flakes Production Line |
| Screw Type | Twin-screw |
| Installed Power | 160 kW |
| Power Consumption | 120 kW |
| Output Capacity | 150–200 kg/h (basis not stated in source — confirm raw material, moisture content, flake thickness) |
| Overall Dimensions (L×W×H) | 41 × 1.5 × 2.2 m |
| Control System | PLC with MCC line integration |
| Flaking Drive | Double motors with hydraulic roller pressure |
| Flaking Temperature Monitoring | Infrared sensor |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven Airflow | Dual circulating fans with cyclone dust removal |
| Coating System | Double tumble melting, elevator, spray nozzle |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn grits or corn flour, toasted without sugar addition |
| Sugar-coated corn flakes | Corn base with sugar syrup tumbling and secondary drying |
| Multi-grain breakfast cereals | Blends of rice, wheat, oat, and barley requiring adjusted screw profile |
| Shaped cereal formats | Ball, tube, ring, star, and fruit loop profiles via interchangeable die plates |
| Fortified cereal production | Vitamin-mineral premix incorporated at mixing stage with roasting temperature controlled for nutrient retention |
What "150 kg/h" Actually Depends On in Breakfast Cereal Twin-Screw Extrusion Process
Nominal throughput only holds when starch gelatinisation matches your exact grain blend and moisture window.
I have watched lines stall at two-thirds of quoted capacity because the corn grits arriving at the hopper carried a different protein and starch ratio than the sample used during vendor testing. The barrel temperature profile that works for one supplier’s corn produces under-cooked, dense flakes with another [NEED_CITE: starch gelatinisation temperature ranges for different cereal grains]. When corn flakes extrusion technology is specified without locking the screw configuration to the buyer’s actual raw material certificate, the result is inconsistent expansion and flake density that drifts outside what the packaging market expects.
Barrel Temperature Zones and Starch Behaviour
The MT70 barrel is divided into independently heated zones, each governing a different phase of the breakfast cereal twin-screw extrusion process. Early zones hydrate and begin gelatinisation, while the final metering zone controls melt viscosity before the die. When processing high-fibre oat blends, the moisture and heat input must shift compared to pure corn, otherwise the dough reaches the die either too stiff to flake or too wet to hold shape after roasting.
Die Geometry and Flake Density Control
Die land length and orifice diameter together determine how much shear the dough receives in the final moments before exit. A longer land increases back-pressure, producing a denser pellet that flakes into a thicker, crunchier corn flake with extended bowl-life. Shorter lands suit lighter, faster-expanding formats. This is where corn flakes extrusion technology either delivers the target crunch profile or misses it entirely — and why die selection must follow the product specification, not the machine catalogue default [NEED_CITE: die land length influence on extrudate density in cereal processing].
Reading the Specs That Actually Matter
The 160 kW installed power and 120 kW operating consumption indicate the thermal and mechanical headroom available across the barrel heaters and main drive. A twin-screw configuration provides positive conveying and self-wiping action, essential when switching between sticky sugar-coated formulations and dry natural corn recipes. The 41-meter line length encompasses every station from mixing through packing, meaning floor planning must account for the full footprint rather than the extruder alone. The hydraulic flaking system with infrared temperature monitoring keeps roller gap and surface temperature stable, which directly governs whether every flake leaves the press at uniform thickness. The dual-fan roasting oven with cyclone extraction ensures even blistering without fine dust accumulation that could scorch and discolour the product.
When Generic Screw Builds Cost You Product
A screw configuration copied from a standard template assumes a single corn variety at a fixed moisture level. When the actual raw material deviates, the extruder either surges — producing alternating thick and thin flakes — or fails to gelatinise the starch fully, leaving a raw centre that turns brittle after roasting [NEED_CITE: effects of incomplete gelatinisation on cereal flake texture]. Operators then chase the problem by adjusting feeder speed or barrel heat, which only masks the mismatch. The batch is already compromised before anyone notices the pattern on the quality chart.
Why Procurement Here Reduces Extrusion Risk
Every screw element and die plate is selected after reviewing your raw material analysis report, not pulled from a standard assembly list. The in-house testing workshop runs your actual grain blend through the MT70 before the line ships, generating a trial report that documents the exact temperature profile, moisture window, and screw arrangement that produced acceptable flakes. Throughput is calculated across every station — extrusion, flaking, drying, roasting, and coating — so no single unit bottlenecks the rest. Electrical schematics confirm voltage and frequency for your facility before production begins, avoiding the commissioning delays that occur when a control panel arrives wired for the wrong grid [NEED_CITE: industrial voltage and frequency standards by region]. CE and ISO documentation accompanies every shipment, supporting import compliance and local safety inspection.
Documentation & Verification
- Screw and die configuration record tied to your raw material certificate and target flake density
- Trial run report from in-house testing on your specific cereal blend before dispatch
- Line layout drawing with throughput calculation across extrusion, flaking, roasting, and packing stations
- Electrical schematic confirming voltage, frequency, and control language for your facility
- CE declaration of conformity and ISO certificate for import and local compliance
Installation, Commissioning & Support
- 41-meter line footprint requires level concrete floor with anchor points mapped to the layout drawing
- 160 kW installed load needs dedicated circuit with voltage and frequency matching the confirmed schematic
- Twin-screw extruder ships partially assembled; barrel sections and screw elements aligned on site
- PLC and MCC commissioning includes parameter upload from the trial run report
- Operator training covers screw swap procedure, hydraulic roller adjustment, and roasting oven temperature profiling
- Wear parts list specifies screw elements, die plates, and flaking roller shells with reorder intervals
Before You Send an Inquiry
Specify the cereal grain or blend you intend to process, along with a recent proximate analysis if available. State your target flake thickness, final moisture content, and whether sugar coating is required. Confirm the voltage and frequency at your plant, plus the language preference for the PLC interface. If you are replacing an existing line, note the upstream mixer capacity and downstream packing format so throughput matching starts from accurate data.
Frequently Asked Questions
Q: How is screw configuration selected for different cereal raw materials?
A: Each screw element profile and die land length is chosen after reviewing the buyer’s grain composition, protein content, and target flake density. The configuration is documented and validated during an in-house trial run on the actual raw material before the line ships, ensuring starch gelatinisation and expansion match the product specification.
Q: What barrel temperature and moisture range produce correct gelatinisation for corn flakes?
A: The range depends on the specific corn variety and any secondary grains in the blend. During the pre-shipment trial, temperature across each barrel zone and feed moisture are adjusted incrementally until the extrudate shows full gelatinisation without over-cooking, and those settings are recorded in the trial report for commissioning reference.
Q: How is the pre-shipment trial run conducted?
A: The buyer sends a representative batch of raw material to the testing workshop. The MT70 runs the material through extrusion, flaking, and roasting under varying parameters. The resulting trial report documents screw build, barrel temperatures, moisture levels, flake thickness measurements, and sensory evaluation of the final product.
Q: How is throughput verified across all stations to prevent bottlenecks?
A: Capacity calculations cover the extruder output, flaking roller pass rate, dryer residence time, roasting oven belt speed, and coating drum cycle. Each station is sized so the slowest unit still meets the line target, and this matched layout is included in the documentation package before production begins.
Q: How does the roasting oven design affect final flake crispness?
A: The oven uses two independent circulating fans and a vibrating pan to expose every flake surface to uniform hot air. The conciliation burner combustion chamber and cyclone dust removal prevent scorching from fine particle buildup. Temperature profiling during the trial run establishes the residence time and air velocity needed for consistent surface blistering and target crunch.



