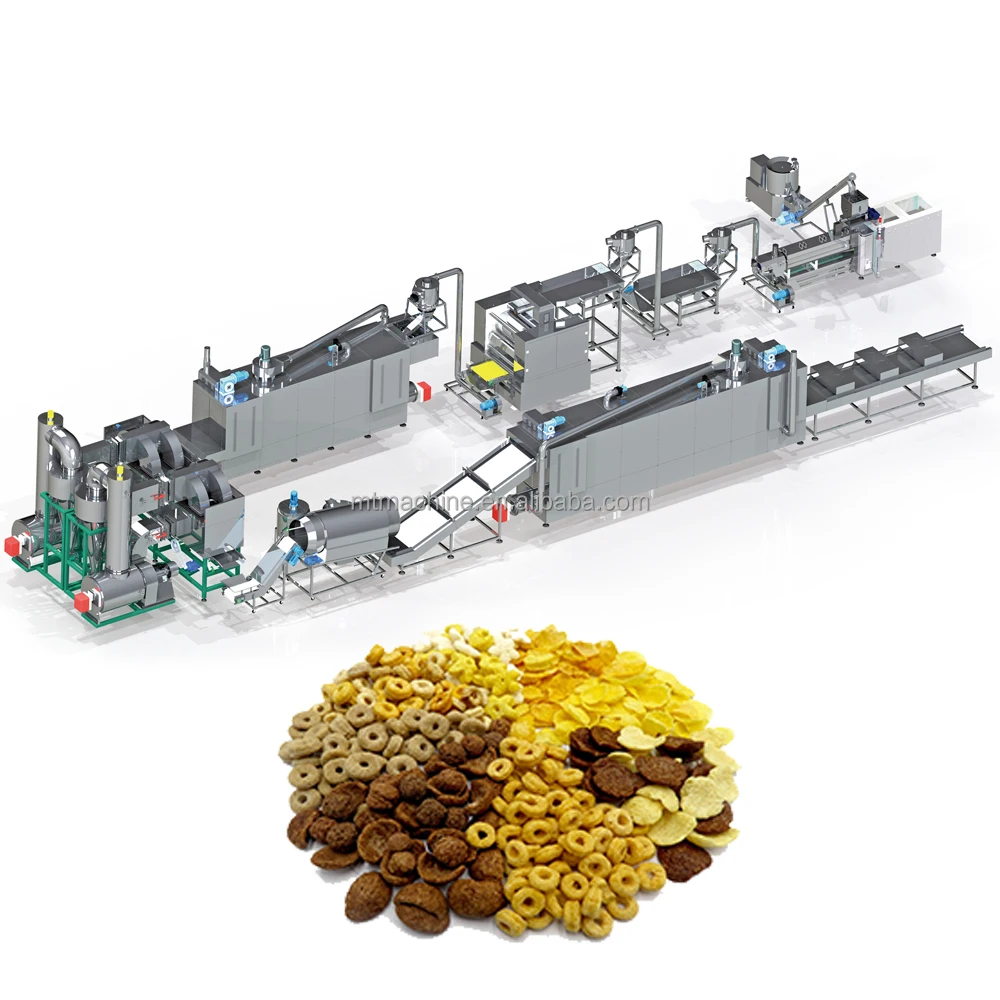
Process-Specific Engineering — Every MT-75 screw profile and die geometry is tuned to the buyer’s actual cereal formulation before the line is cleared for production.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-75 Twin Screw Extruder |
| Product Type | Twin Screw Extruder Corn Flakes Production Line |
| Screw Type | Twin-screw with automatic lubricating and cooling |
| Output Capacity | 200–300 kg/hr (basis not stated in source — confirm raw material, moisture and pellet format) |
| Heating Source (Dryer / Roaster) | Gas or Electric |
| Flaking Station | PLC-controlled hydraulic double-roller system; dual independent motors; infrared sensor for temperature pipe regulation |
| Roasting Oven | Hot air circulating; conciliation burner; two separate circulating fans; cyclone dust removal |
| Coating System | Double tumble for sugar melting; elevator; coating drum; spraying nozzle |
| Voltage | 220V / 380V (configurable) |
| Power | 3 kW (rated or peak not specified — verify against final motor schedule) |
| Control System | PLC with automatic lubricating and cooling function on extruder |
| Assembly State | Complete line: Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Cooling → Packing (sugar-coated variant adds Sugar Spraying → Sugar Coating → Drying) |
| Warranty | 1 Year (core component: Gearbox) |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes from whole corn grits | Corn, maize, degerminated corn meal |
| Multi-grain breakfast flakes | Rice, wheat, oat, barley and blended cereal bases |
| Sugar-coated and frosted flakes | Corn or rice base with sugar glaze or honey coating |
| Extruded cereal snacks | Various grain formulations using the same extrusion and shaping stations |
Why the Wrong Screw Profile Destroys Your Corn Flake Density
Corn flakes live or die by gelatinisation uniformity inside the barrel.
Generic screw builds copy a configuration that worked on pure corn grits, then watch it fail the moment a buyer switches to an oat-rice blend or adjusts moisture content. The starch does not fully gelatinise, the pellet exits under-expanded, and the flaking rollers produce uneven thickness that burns in the roasting oven. I have seen entire batches scrapped at commissioning because the die design was never matched to the buyer’s actual recipe. A corn flakes extrusion production line technology audit must start with the raw material certificate, not the catalog sheet [NEED_CITE: starch gelatinisation temperature thresholds by cereal grain type].
Barrel Temperature Profiling and Starch Gelatinisation
The MT-75 barrel is divided into multiple heating and cooling zones, each managed independently so that the corn flour mixture passes through a controlled gelatinisation curve. Automatic lubricating and cooling keeps the screw shaft stable even during extended runs, preventing thermal drift that would shift the gelatinisation window. Getting this profile right is the core of corn flakes extrusion production line technology — too low and the pellet is dense; too high and the starch degrades before it reaches the die.
Die Geometry and Pellet Expansion Control
The die plate determines the cross-section and initial expansion ratio of the extrudate before it enters the flaking station. For corn flakes, the goal is a pellet that is dense enough to hold together through the dryer yet porous enough to blister properly during roasting. Die hole diameter, land length and face angle are all specified against the buyer’s grain blend and target flake thickness. A mis-specified die will produce pellets that either collapse under the flaking rollers or refuse to flatten, sending them into the roaster as hard cylinders [NEED_CITE: twin-screw die land length and expansion ratio relationship].
Reading the Numbers Behind the Line
The twin-screw design gives a longer residence time compared to single-screw extruders of similar barrel diameter, which matters for cereal blends with mixed particle sizes. The PLC-controlled flaking station uses hydraulic pressure on double rollers driven by separate motors, so the gap and pressure stay consistent across the full roller width — this is what prevents thick-thin variation in the final flake. Hot air roasting with dual circulating fans and a cyclone dust removal device provides even heat distribution and pulls fine particulate out of the chamber, reducing scorch points. Output capacity is listed as 200–300 kg/hr, but this figure depends entirely on the raw material, moisture level and pellet format being run — always confirm against your own formulation during a trial.
The Hidden Cost of Skipping a Raw-Material Trial Run
When a buyer orders without sending a sample of their actual grain blend for a pre-shipment trial, the screw configuration is set on assumptions. The line arrives, the first production run shows poor expansion, and weeks pass while replacement screw elements are shipped. Flaking rollers set for one pellet density will crack or skip pellets of a different hardness. Throughput then drops because the dryer and roaster were sized for a nominal capacity the extruder cannot actually deliver on that material [NEED_CITE: extrusion line throughput mismatch between stations].
Why the Process Engineering Approach Matters Here
Screw configuration and die design are specified to the buyer’s raw material and target flake format — not pulled from a generic library. The in-house testing workshop allows trial runs on customer-supplied grain blends before the line ships, so adjustments happen in Jinan rather than on the buyer’s factory floor. Every station — mixing, extrusion, flaking, drying, roasting, coating and cooling — is sourced under one supply chain, which means throughput is balanced across the line rather than assembled from mismatched vendors. Pre-sales engineering covers layout and utility planning, and post-installation support includes operator training and a documented wear parts schedule.
Documentation & Verification
- Line layout and capacity calculation matched to your grain blend and target flake weight
- Screw and die configuration record tied to your specific raw material certificate
- Trial run report on your actual cereal formulation before shipment clearance
- Electrical schematic with voltage and frequency confirmation for your local grid
- Machinery test report and video outgoing-inspection provided before dispatch
- Operation and maintenance manual with lubrication intervals for the twin-screw gearbox
Installation, Commissioning & Support
- Foundation plan accounts for the full line footprint including roaster exhaust ducting
- Dedicated power circuit sized for 380V three-phase supply and extruder motor starting current
- Pre-assembled modules arrive labeled for sequenced installation from mixing through packing
- Commissioning includes barrel temperature profile calibration and PLC parameter setting for your recipe
- Operator training covers screw element inspection, roller gap adjustment and roaster fan balancing
- Wear parts list provided with recommended replacement intervals for screws, dies and roller surfaces
What to Include with Your Inquiry
Send your actual cereal formulation — grain types, particle size distribution and target moisture at the extruder feed. Specify whether the end product is natural, sugar-coated or frosted, and provide the target flake dimensions and bulk density your packaging line requires. Confirm your local voltage, frequency and preferred PLC language, along with available workshop floor space and ceiling height so the layout proposal accounts for roaster ventilation and cooling conveyor length.
Frequently Asked Questions
Q: How is screw configuration selected for different cereal grains like corn versus oat?
A: Each grain has a distinct starch gelatinisation temperature and fibre content that affects barrel friction and expansion. We run your specific blend in the testing workshop, measure pellet density and expansion ratio, then adjust screw element pitch, kneading block arrangement and die geometry until the output matches your target flake specification.
Q: How do you verify capacity on the buyer’s actual raw material?
A: Capacity figures in the catalog assume reference conditions. Before final quotation, we conduct a measured trial run using your grain blend at your specified moisture level, record actual throughput at the extruder discharge and confirm that downstream stations — flaker, dryer, roaster — can handle that volume without bottlenecking.
Q: What barrel profile and moisture range produce correct flake expansion?
A: The optimal range depends on grain composition, but generally the barrel zones progress from feed-section preheating through a controlled gelatinisation plateau and a short die-zone cooling stage. Moisture at the feed inlet is adjusted based on your grain blend’s absorption characteristics and is validated during the pre-shipment trial.
Q: How is throughput balanced between the extruder, flaker, dryer and roaster?
A: Each station’s rated capacity is calculated against the extruder’s verified output on your material. Dryer belt speed, roaster residence time and flaking roller feed rate are all specified so no single station creates a bottleneck or forces upstream equipment to idle.