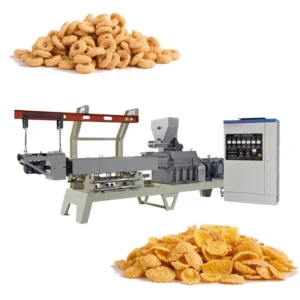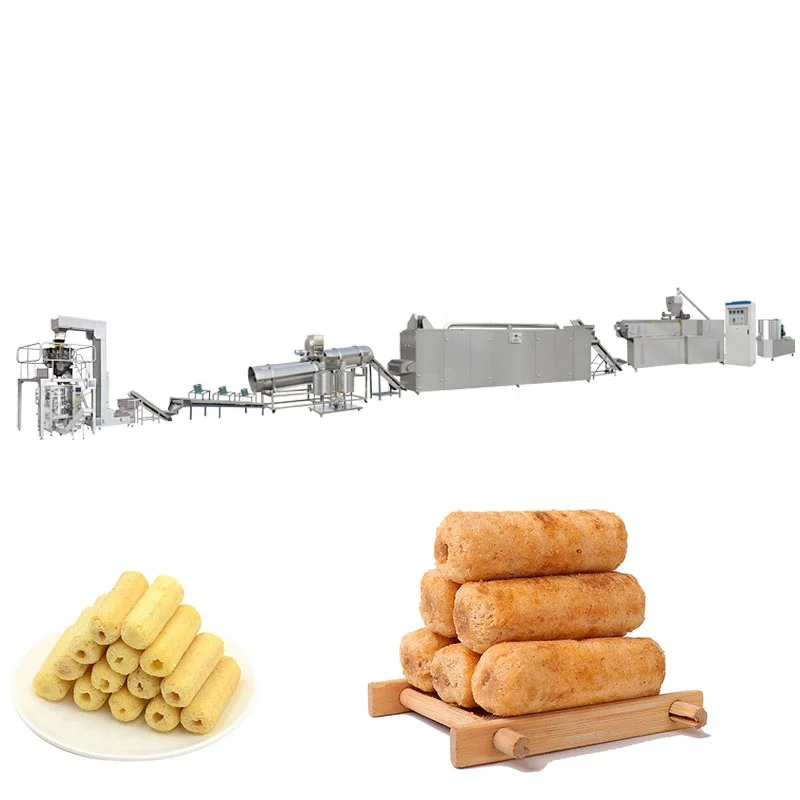
Custom Screw & Die Engineering — Every corn flakes extrusion line production line ships with screw profiles and die geometries matched to the buyer’s actual grain formulation, verified through in-house test runs before dispatch.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 (MT70 and MT85 also available) |
| Product Type | Twin Screw Corn Flakes Extrusion Line |
| Screw Type | Twin Screw |
| Installed Power | 210 kW (MT75); 160 kW (MT70); 190 kW (MT85) |
| Power Consumption | 150 kW (MT75); 120 kW (MT70); 140 kW (MT85) |
| Output Capacity | 300–500 kg/hr (MT75, basis not stated in source — confirm raw material, moisture, flake thickness); 150–200 kg/hr (MT70); 300–400 kg/hr (MT85) |
| Overall Dimensions | 45 × 1.5 × 3.5 m (MT75); 41 × 1.5 × 2.2 m (MT70); 43 × 1.5 × 3.2 m (MT85) |
| Control System | PLC on flaking unit; MCC and PLC across full line |
| Barrel Heating | Electric heating zones |
| Flaking Unit | Hydraulic double-roller, dual motor separate drive, infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric (configurable) |
| Roasting Oven | Hot air with conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Final Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (by die change) |
| Screw Feature | Special surface treatment for wear resistance, automatic lubrication and cooling |
| Assembly State | Complete turnkey corn flakes making machine line |
| Certifications | CE (since 2014); ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal packaging | Corn grits and corn flour at controlled moisture |
| Sugar-coated corn flakes and frosted cereal | Corn, rice, or wheat base with sugar spray coating |
| Multi-grain breakfast cereal rings and balls | Blends of oat, barley, wheat, and rice powder |
| Shaped cereal snacks (stars, wheels, fruit loops) | Corn or rice flour with die/mould change |
| Fortified nutritional cereal for institutional supply | Grain blends with added vitamin and mineral premix |
What "300–500 kg/hr" Actually Depends On
Capacity is a function of your raw material, not the nameplate.
When a corn flakes extrusion line production line is quoted at a nominal throughput, that figure assumes a specific grain type, moisture content, and flake thickness. I once commissioned a line in Jordan where the test runs used standard corn flour, but the buyer switched to a high-fiber local coarse grain on arrival. The extrudate came out thick and dense, expansion collapsed, and we spent two weeks rebuilding every process parameter from scratch. A turnkey corn flakes making machine only delivers its rated output when screw configuration, barrel temperature profile, and die geometry are matched to the exact flour you will run. [NEED_CITE: how raw material fiber content affects extrusion expansion and throughput]
How Barrel Temperature Profiling Shapes Flake Texture
The MT75 barrel uses multiple electric heating zones along its length, each independently controlled. In twin-screw extrusion of corn flakes, the temperature gradient from feed to die determines the degree of starch gelatinisation and the moisture profile of the extrudate. Too little heat in the compression zone and the starch granules remain partially raw, producing a brittle flake that cracks during rolling. Too much heat at the die face and the extrudate expands prematurely, making uniform flake thickness impossible. Getting this profile right for a specific corn variety is the reason in-house trial runs on the buyer’s actual raw material matter before the line ships.
Screw Configuration and Die Design for Grain Variability
Different grain bases behave fundamentally differently under shear and heat. Corn grits gelatinise at a different rate than oat flour, and wheat-based blends carry more gluten, which changes how the extrudate holds its shape after the die. The screw elements on this line are configured — in terms of conveying pitch, kneading block arrangement, and reverse element placement — to match the target raw material. The die geometry is specified alongside it. A generic screw build copied from a standard template will process corn adequately but fail when the buyer switches to a barley or multi-grain blend, producing either under-cooked or over-expanded extrudate that the flaking unit cannot handle consistently. [NEED_CITE: twin screw element configuration for varying starch and protein ratios]
Reading the Specs That Matter for Corn Flake Quality
The hydraulic double-roller flaking unit uses dual independent motors and infrared sensor temperature control. Independent drive means each roller can maintain surface speed even as flake thickness adjustments change the gap — this prevents the dragging and tearing that produce uneven flakes with ragged edges. Infrared monitoring catches roller surface temperature drift before it affects the sheet. The hot air roasting oven runs a conciliation burner with dual circulating fans and cyclone dust removal, which together control how blister forms on the flake surface. Blister size and distribution define the final crunch. The coating system — double tumble melting, elevator, drum, and spray nozzle — allows the line to switch between natural and sugar-coated production without major reconfiguration.
The Hidden Cost of Mismatched Line Stations
A common failure mode in breakfast cereal projects is an extruder that runs at full capacity while the dryer or roasting oven cannot keep up, forcing the operator to slow the entire line. When the flaking unit, dryer, and oven are sourced from separate vendors, each rated on its own nominal throughput, the bottleneck only appears during commissioning. The result is a turnkey corn flakes making machine that never reaches its quoted output. Throughput matching across every station — from mixing through extrusion, flaking, drying, roasting, cooling, and packing — is what separates a functional line from an expensive collection of individual machines. [NEED_CITE: throughput balancing in multi-station food extrusion lines]
Why Procurement Should Start With the Raw Material
Every corn flakes extrusion line production line leaving the Jinan factory is configured around the buyer’s confirmed raw material and target product specification. Screw elements and die plates are specified to the formulation, not pulled from a standard shelf build. The in-house testing workshop runs trial production on the buyer’s actual flour blend before shipment, generating a trial run report that documents real throughput, product density, and flake geometry under verified conditions. MCC and PLC controls are programmed to the confirmed voltage and frequency of the destination facility, and HMI language is set before the line crates. Complete documentation — from screw configuration records to electrical schematics — ships with the equipment, so commissioning starts from a known baseline rather than trial-and-error. The line is CE and ISO certified, meeting import requirements across regulated markets.
Documentation & Verification
- Screw and die configuration record matched to your grain formulation
- Trial run report on buyer-supplied raw material documenting output and flake density
- Electrical schematic with confirmed voltage, frequency, and PLC language
- Line layout drawing with throughput calculation across all stations
- Wear parts list covering screws, dies, and roller surfaces
- CE declaration of conformity and ISO certificate for customs clearance
Installation, Commissioning & Support
- Foundation plan accounts for 45 m line length and hydraulic flaking unit load
- Dedicated power circuit sized for 210 kW installed load on MT75 configuration
- Modular station assembly allows phased installation within existing workshop footprint
- First-run parameter setting covers barrel zones, roller gap, and oven temperature
- Operator training includes screw element changeover and die swap procedures
- Spare screw segments and die plates supplied with initial shipment
What We Need to Build Your Line
To configure a corn flakes extrusion line production line that matches your facility, share the grain types and flour specifications you plan to run, your target daily output, and whether you need natural, sugar-coated, or both product streams. Confirm your local voltage and frequency, preferred HMI language, and available workshop dimensions including ceiling height. If you can supply a sample of your raw material, we will run a trial in the testing workshop and include the results with the proposal.
Frequently Asked Questions
Q: What determines whether the line actually reaches its quoted capacity?
A: Throughput depends on raw material type, moisture content, and target flake thickness. Corn grits at standard moisture behave differently from high-fiber blends or oat-heavy mixes. The quoted range assumes a specific formulation. We verify real output during a trial run on your actual raw material before shipment, so the number in the report reflects your conditions, not generic benchmarks.
Q: How do you select screw and die configuration for different grains?
A: Corn, rice, wheat, oat, and barley each have different starch gelatinisation temperatures and protein structures. Screw element arrangement — conveying, kneading, and reverse sections — is adjusted to control shear and residence time for each blend. Die geometry is matched to the desired extrudate shape and expansion ratio. Configuration is documented in a record that ships with the line.
Q: What is involved in switching between natural and sugar-coated production?
A: The natural line runs mixing through extrusion, flaking, drying, roasting, cooling, and packing. Sugar-coated production adds a sugar spraying and coating stage between roasting and final drying. The double tumble melting system and coating drum are integrated into the line layout, so switching requires process parameter changes rather than physical reconfiguration.
Q: How does local voltage affect the line configuration?
A: Motor ratings, heating elements, and control cabinet components must match the destination facility’s voltage and frequency. A 50 Hz market requires different motor winding than a 60 Hz market. We confirm electrical specifications in writing before production begins, and all PLC and MCC panels are built to that confirmed standard. [NEED_CITE: voltage and frequency standards by export market]
Q: Can we send our raw material for a test run before the line ships?
A: Yes. The testing workshop runs your actual flour blend through the extruder and flaking unit, producing sample flakes under production conditions. The trial run report documents output rate, flake thickness, expansion behavior, and product density. This lets you validate the line configuration before it leaves the factory.