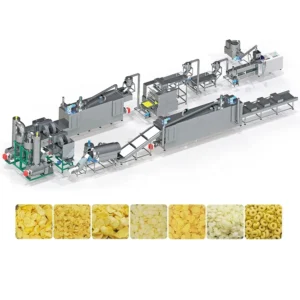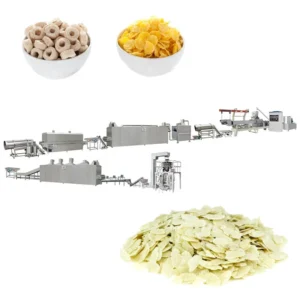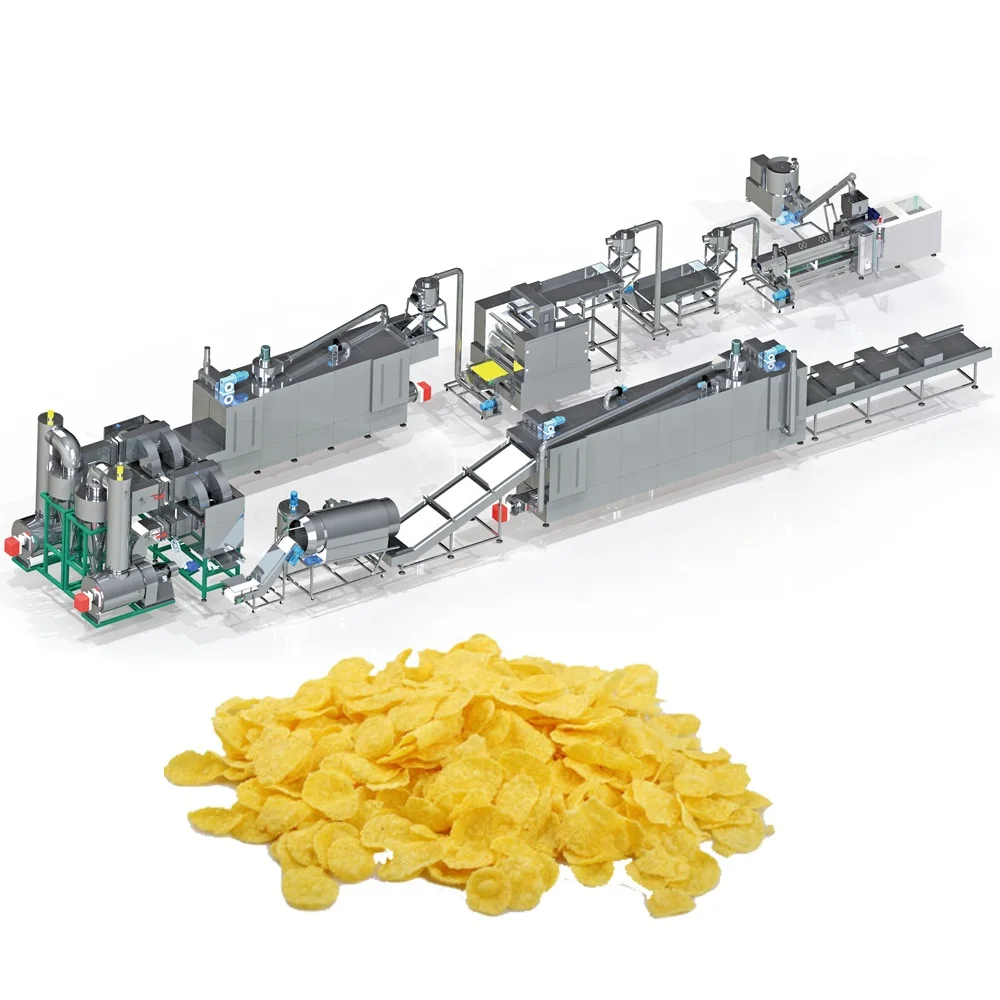
Screw Geometry Dictates Flake Density — twin-screw configuration and die land length are specified to your corn grit size and moisture window before the first trial run.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Output Capacity | 750 kg/hr (basis not stated in source — confirm raw material, moisture content, and product format) |
| Control System | Easy-to-operate interface (PLC / MCC not specified in source) |
| Product Scope | Natural corn flakes, sugar-coated flakes, various shaped breakfast cereals |
| Layout Customization | Engineered drawings tailored to specific factory sizes |
| Screw Type | Not stated in source (verify against manufacturer catalog) |
| Screw Diameter | Not stated in source (verify against manufacturer catalog) |
| L:D Ratio | Not stated in source (verify against manufacturer catalog) |
| Barrel Zones | Not stated in source (verify against manufacturer catalog) |
| Die Configuration | Not stated in source (verify against manufacturer catalog) |
| Moisture Range | Not stated in source (verify against manufacturer catalog) |
| Steam or Water Injection | Not stated in source (verify against manufacturer catalog) |
| Line Stations | Mixing, extrusion, drying, flaking, toasting, coating, packing (verify scope against supplier) |
| Certification | CE and ISO referenced in company profile; confirm line-specific declaration |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | Degerminated corn grits, standard moisture range |
| Sugar-coated breakfast cereal | Extruded corn pellets with syrup coating |
| Fortified cereal formats | Corn base blended with vitamin and mineral premix |
| Whole-grain variant trials | Coarse-ground corn with bran inclusion |
Why Your Corn Flake Density Misses the Bowl-Life Target
A bulk density that drifts outside the market specification is almost always traceable to the screw profile and die geometry decided before the line was shipped.
I have watched lines produce beautiful flakes during a factory test on standard corn grits, then deliver dense, hard pellets the moment the buyer switched to a coarser local variety with higher fibre content. The extrusion shear was set for a different particle size, and the starch gelatinisation window shifted. The result was flakes that cracked during toasting and sank in milk within seconds [NEED_CITE: starch gelatinisation and corn grit particle size relationship in twin-screw extrusion]. When the screw elements and die land are not matched to your actual raw material and target moisture, the corn flakes extrusion production line technology inside the barrel simply cannot hold the expansion ratio you need.
Shear, Temperature, and the Gelatinisation Window
Starch gelatinisation inside the barrel is the single event that determines whether your flakes will hold their structure through flaking and toasting. The barrel temperature profile must bring the corn grit above the gelatinisation threshold while maintaining enough moisture for the starch granules to swell. A barrel with too few heating zones cannot create the gradual ramp needed for whole-grain variants, and hot spots cause localized over-cooking that shows up as dark specks on the final flake.
Die Land Length and Flake Expansion Ratio
The die is where pressure drops and the cooked dough expands into the rope that will later be flaked. A shorter die land releases pressure quickly, giving high expansion and a lighter flake; a longer die land restrains expansion, yielding a denser product with longer bowl-life. Getting this wrong means either fragile flakes that shatter during coating or hard flakes that never soften in milk. Die geometry must be selected alongside the screw configuration, not treated as an independent choice [NEED_CITE: die design and expansion ratio in food extrusion].
Reading the Specs That Actually Matter
The L:D ratio determines how long the corn grit stays inside the barrel and therefore how completely the starch cooks. A short L:D ratio may leave under-gelatinised cores that become hard spots after flaking, while an excessively long ratio can over-shear the dough and collapse the cell structure needed for a crisp bite. Barrel zone count tells you how finely you can control the temperature ramp — critical when you move from standard degerminated corn to a whole-grain recipe that releases more fibre and alters viscosity. The moisture range specification, often tied to upstream steam or water injection, sets the envelope within which the extruder can hold stable output; drift outside that window and the torque load spikes, tripping the motor or producing inconsistent ropes that jam the flaker rolls.
The Cost of Skipping the Trial Run
When a line ships without a pre-shipment trial on the buyer’s own corn grits, the first commissioning week becomes an expensive experiment. Screw elements have to be swapped, barrel zones re-tuned, and the die replaced — all while the dryer and toaster sit idle waiting for stable feed. I have seen commissioning stretches from days into weeks because the extruder was configured for a generic build rather than the buyer’s actual raw material [NEED_CITE: cost of unplanned downtime during food line commissioning]. The downtime loss alone can outweigh any initial savings on the equipment purchase.
What Separates This Line from a Catalog Build
Every station from the mixer to the packer is sourced from one supplier, so throughput is balanced across extrusion, drying, flaking, toasting, and coating rather than assembled from separate vendors who each quote their own nominal capacity. The screw configuration and die design are specified to the buyer’s corn grit size, moisture, and target flake thickness — not copied from a generic template. An in-house testing workshop allows trial runs on the buyer’s actual raw material before shipment, producing a documented report rather than leaving product development to the commissioning phase. Electrical schematics and voltage are confirmed against the buyer’s factory supply before production starts, eliminating the delays that arise when a 380 V machine arrives at a 415 V site. The twin-screw expertise behind this line covers pet food, aquatic feed, snacks, cereals, starch, and protein applications, meaning the engineers have seen how different corn varieties behave under shear.
Documentation & Verification
- Screw and die configuration record tied to your corn grit particle size
- Trial run report on your raw material from the in-house testing workshop
- Line layout and capacity calculation balancing every station throughput
- Electrical schematic and voltage confirmation matched to your plant supply
- Operation and maintenance manual with wear parts list for extruder screws and dies
Installation, Commissioning & Support
- Foundation plan accounts for extruder weight and vibration isolation points
- Dedicated power circuit sized for the extruder motor rated load
- Extruder barrel segments arrive separated for site reassembly and alignment
- First-run parameter log captures screw speed, barrel temperatures, and die pressure
- Operator training covers screw element replacement and die cleaning intervals
- Wear parts inventory includes spare screw sections and die inserts for your configuration
Preparing Your Inquiry
Share your corn grit source, particle size distribution, and target moisture content so the screw profile can be matched before quotation. Confirm your local voltage, frequency, and preferred control language to avoid commissioning delays. Provide your available factory length and ceiling height so the line layout can route extrusion, drying, flaking, and toasting without bottlenecks.
Frequently Asked Questions
Q: How is the screw configuration chosen for different corn grit sizes?
A: The screw element sequence — conveying, kneading, and reverse-flight sections — is adjusted based on your grit particle size and fibre content. Coarser or whole-grain corn requires a different kneading intensity to reach full gelatinisation without over-shearing. The configuration is documented and can be reviewed before the trial run.
Q: What barrel temperature profile is needed to avoid over-expansion?
A: A gradual ramp across multiple barrel zones brings the dough through gelatinisation without sudden pressure release. Too sharp a rise causes the starch to puff prematurely inside the barrel, leading to unstable ropes at the die. The zone count and setpoints are matched to your specific corn variety and moisture level.
Q: How is flake density verified before the machine ships?
A: A trial run on your actual corn grit produces sample flakes that are measured for bulk density, expansion ratio, and bowl-life in milk. The results are compared against your target specification and documented in the trial run report, so adjustments to the die or screw can be made before dispatch.
Q: What steam or water injection parameters matter upstream?
A: Moisture added before the extruder must be consistent and well-mixed into the grit. Uneven moisture creates zones of under-cooked and over-cooked dough inside the barrel, causing density variation in the final flake. The injection system capacity and mixer residence time are sized to match the extruder throughput.
Q: How does extruder throughput align with the dryer and toaster?
A: Each downstream station is specified to handle the extruder output at the confirmed moisture and product format. If the dryer cannot remove moisture fast enough, the flakes arrive at the flaker too soft and tear instead of pressing flat. Throughput matching is shown in the line layout and capacity calculation.