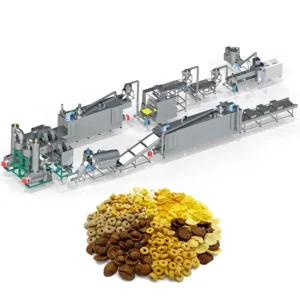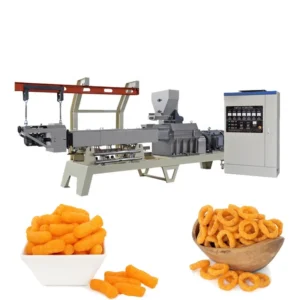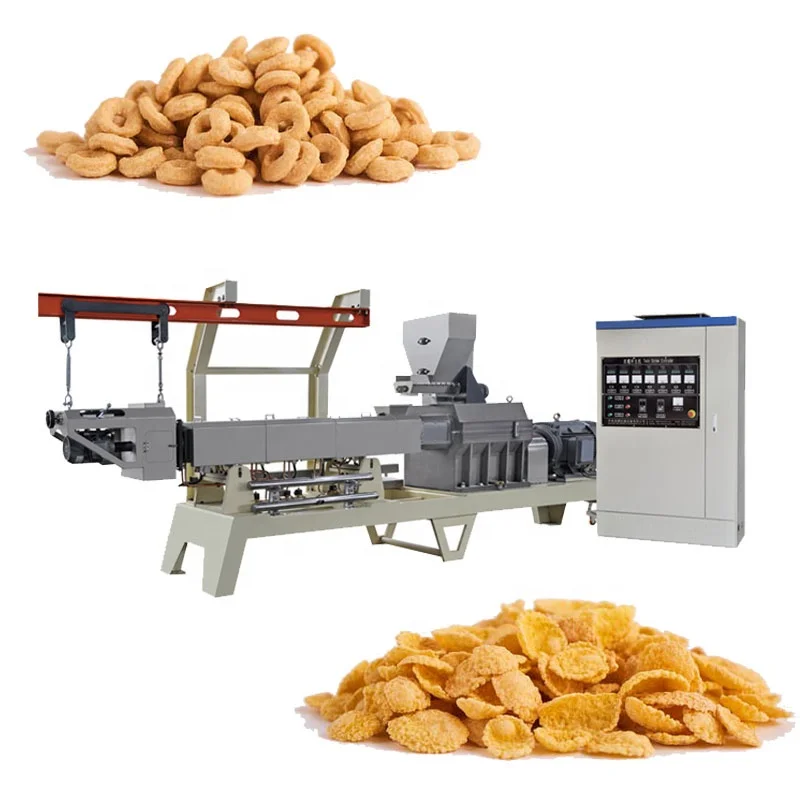
Process-Matched Extrusion Lines — screw configuration and barrel temperature zones are dialed in on your actual corn grits or flour blend during an in-house trial run before the line ships, not copied from a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-65 (MT-70, MT-75, MT-85 also available) |
| Product Type | Corn Flakes Production Line with Twin Screw Extruder |
| Screw Type | Co-rotating twin screw with sectional modules |
| Installed Power (MT-65) | 84 kW |
| Real Power Consumption (MT-65) | 59 kW |
| Output Capacity (MT-65) | 120–150 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Mixer Tank Size | φ600×500 mm |
| Corn Flakes Press Roller | 510×310×1050 mm |
| High-Temperature Oven Heating | Gas-fired, dual-side baking |
| Sugar Spraying Roller Size | φ600×2700 mm |
| Overall Dimensions (MT-65 Line) | 12000×1200×2200 mm |
| Control System | PLC (source value — verify against manufacturer catalog) |
| Warranty | 1 year complete with lifetime maintenance |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional toasted corn flakes | De-germed corn grits |
| Multi-grain breakfast flakes | Blends of corn flour, rice flour, and wheat flour |
| Sweetened or coated cereal flakes | Corn base with sugar or syrup coating |
| Fortified breakfast cereals | Grain blends with added nutritional premix |
Why Copied Screw Profiles Sink Corn Flake Density
A corn flakes extrusion technology production line that runs generic screw elements will fail the moment your raw material deviates from the standard de-germed corn grits profile.
I learned this the hard way in Mexico. We were commissioning a line using a standard screw build validated on low-fat corn flour. The buyer switched to high-fat whole corn without telling us until we arrived. The extrudate came out dense, the flakes collapsed after pressing, and two full batches of raw material went to waste. We spent a week re-tuning barrel temperatures, moisture injection, and screw element sequencing before the line held spec. [NEED_CITE: effect of lipid content on starch gelatinisation in twin-screw extrusion]
That failure changed how I approach every breakfast cereal project. Before any quotation goes out, I need the buyer’s actual raw material in our testing workshop. We run it through the extruder, press it, bake it, and measure the final flake density and bowl life. Only then do we lock in the screw configuration record.
Barrel Temperature Profiling for Controlled Gelatinisation
The barrel on this twin-screw extruder is divided into multiple heating and cooling zones. Each zone is controlled independently, which matters because corn starch gelatinisation is not a single-temperature event — it progresses through hydration, granule swelling, and melt-phase transition as the material moves from feed to die. The corn flakes extrusion technology production line relies on this gradient to build the right dough viscosity before the material reaches the die plate.
Die Geometry and Expansion Behaviour
The die opening shape and land length directly control how the extrudate expands as it exits the barrel. For corn flakes, you want limited radial expansion so the rope can be cut and pressed into a uniform flake. Too much expansion and the press roller crushes an air pocket instead of flattening a solid sheet. The die design is matched to your target flake thickness and the moisture content leaving the barrel. [NEED_CITE: die land length effect on extrudate expansion in cereal processing]
Reading the Specs That Matter
The co-rotating twin screw with sectional modules lets the screw profile be rearranged — kneading blocks, reverse elements, and conveying sections are positioned based on your specific flour blend and moisture target. The installed power of 84 kW on the MT-65 with a real draw of 59 kW indicates the motor is sized with headroom for viscous doughs without running at thermal limits. The large-diameter press roller at 510 mm gives a wide nip zone, which means the extrudate rope is flattened gradually rather than smashed — critical for maintaining internal structure before the oven sets it. Gas-fired dual-side baking in the 4.5-meter oven provides the rapid surface drying needed to lock in crispness without case-hardening the flake core.
What Happens When Stations Are Mismatched
An extruder that pushes more output than the press can flatten creates a pile-up of hot extrudate that cools and stiffens before it reaches the roller nip. The result is uneven flake thickness and a texture that shatters in the bowl instead of holding its crunch. The same problem repeats downstream if the oven cannot dry the flakes at the rate the press delivers them — moisture trapped inside the flake causes sogginess within minutes of packaging. [NEED_CITE: throughput balancing across extrusion, flaking and drying stations]
Why Buyers Source This Line Here
The screw and die configuration is specified to your raw material, not pulled from a template — every build starts with your flour or grits sample running in the testing workshop. Throughput is matched across all six stations from mixer through sugar coating, so the rated output is a line figure, not just an extruder figure. The PLC-controlled barrel zones allow real-time temperature adjustment during commissioning to fine-tune gelatinisation on your shop floor. Wear parts such as screw elements and die inserts are documented with exact module sequencing, so reordering does not require a new round of trial and error.
Documentation & Verification
- Line layout drawing with station-by-station throughput calculation for your target capacity
- Screw and die configuration record showing exact module positions for your raw material
- Trial run report on your corn grits or flour blend documenting flake density and expansion
- Electrical schematic with voltage and frequency confirmed for your facility before production
- Factory test record with photographic evidence of flake output before crating
Installation, Commissioning & Support
- Line footprint of 12000×1200×2200 mm requires level concrete floor with anchor points at each station
- 84 kW installed power demands dedicated circuit with voltage confirmed before electrical panel build
- Stations ship as separate modules and are bolted and aligned on-site during commissioning
- Barrel temperature zones and press roller gap are calibrated using your raw material on first run
- Operator training covers screw element handling, die cleaning, and oven burner maintenance
- Wear parts list identifies every screw module and die insert for accurate reordering
Before You Send an Inquiry
To configure the corn flakes extrusion technology production line correctly, share your raw material type and supplier spec sheet, your target flake density and bowl-life expectation, and your facility voltage and frequency. If you have an existing dryer or coating drum you plan to integrate, include its throughput rating so we can match the extruder and press output accordingly.
Frequently Asked Questions
Q: How is screw configuration determined for my specific corn grits or flour blend, and can I see a trial run before shipment?
A: We run your raw material in our testing workshop before finalising the build. The screw elements — conveying, kneading, and reverse sections — are arranged based on the gelatinisation behaviour we observe. You receive a trial run report showing flake density and expansion data before the line ships.
Q: What barrel temperature profile and moisture level are needed to achieve the target flake expansion and crispness?
A: The profile varies by raw material. De-germed corn grits typically need a rising gradient through the barrel zones with controlled steam or water injection. We set these values during the workshop trial and document them so your operators can replicate the result on your floor.
Q: How is throughput balanced between the extruder, flaking press and oven so the line holds its rated output?
A: Each station is sized so its maximum throughput exceeds the extruder output by a margin. The press roller width and speed, oven belt length and residence time, and coating drum volume are all calculated against the extruder capacity to prevent bottlenecks.
Q: What documentation is provided for screw and die configuration so I can reorder wear parts accurately?
A: You receive a configuration record listing every screw module type, its position on the shaft, and the die insert geometry. This lets you reorder identical replacements without guessing or sending worn parts back for measurement.
Q: Can the extrusion parameters be adjusted on-site during commissioning to fine-tune flake density and texture?
A: Yes. The PLC-controlled barrel zones allow temperature adjustments per zone, and the press roller gap is adjustable. During commissioning we run your material and tweak these settings until the flake density and crispness match your market specification.