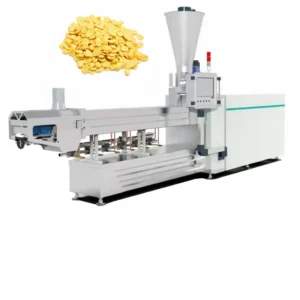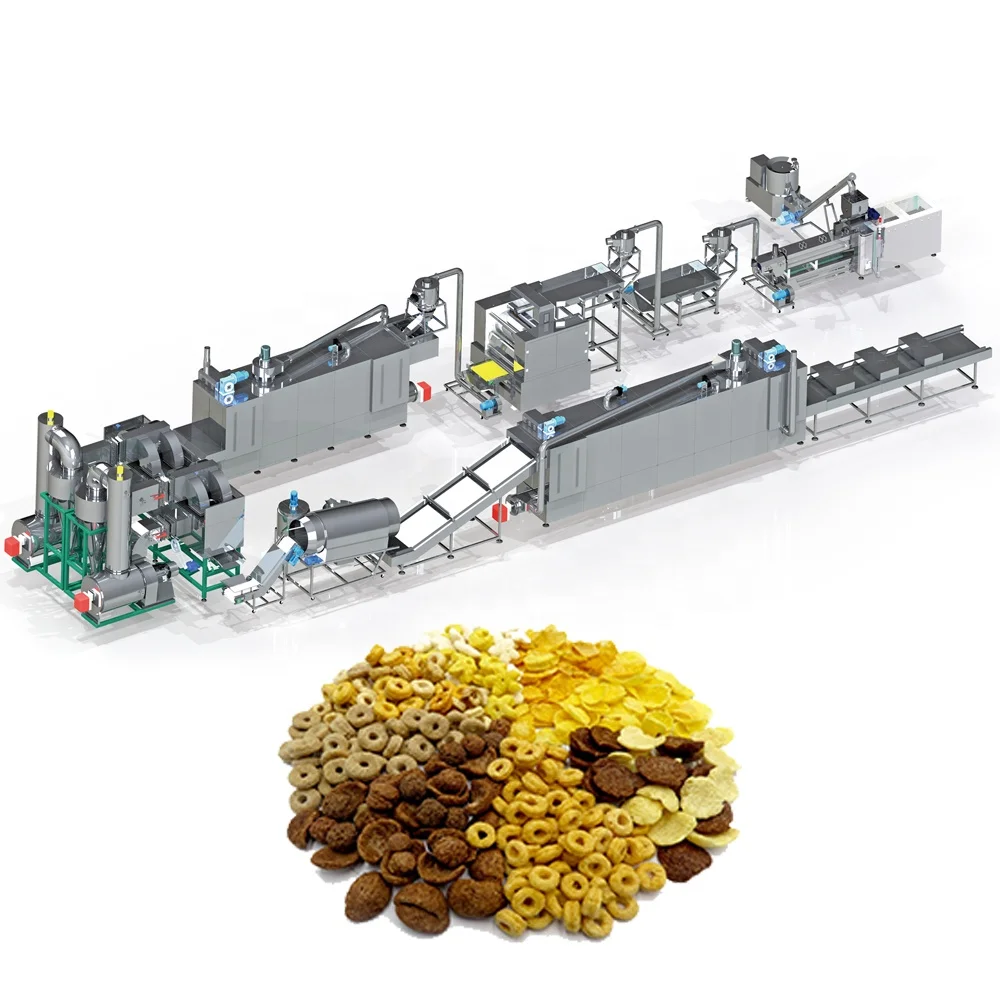
Screw Geometry Dictates Density — Sectional co-rotating modules let us dial starch gelatinisation and expansion precisely to the corn variety and flake thickness the buyer specifies, not a generic catalog build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-65 / MT-70 / MT-75 / MT-85 |
| Product Type | Corn Flakes Production Line |
| Extruder Type | Twin-screw, co-rotating, sectional screw modules |
| MT-65 Installed Power | 84 kW |
| MT-65 Real Power | 59 kW |
| MT-65 Output Capacity | 120–150 kg/h (basis to be confirmed) |
| MT-65 Dimension | 12000 × 1200 × 2200 mm |
| MT-70 Installed Power | 132 kW |
| MT-70 Real Power | 92 kW |
| MT-70 Output Capacity | 200–250 kg/h (basis to be confirmed) |
| MT-70 Dimension | 23000 × 1500 × 2200 mm |
| MT-75 Installed Power | 186 kW |
| MT-75 Real Power | 140 kW |
| MT-75 Output Capacity | 300–400 kg/h (basis to be confirmed) |
| MT-75 Dimension | 24000 × 1500 × 2800 mm |
| MT-85 Installed Power | 239 kW |
| MT-85 Real Power | 167 kW |
| MT-85 Output Capacity | 400–500 kg/h (basis to be confirmed) |
| MT-85 Dimension | 28000 × 1500 × 2800 mm |
| Mixer Power / Tank Size | 4 kW / φ600 × 500 mm |
| Screw Conveyor Power | 0.75 kW |
| Corn Flakes Press Machine Power | 16.12 kW |
| Press Roller Size | 510 × 310 × 1050 mm |
| High-Temperature Oven | Gas-fired, dual-side baking, 4.5 × 1.4 × 1.8 m |
| Sugar Spraying System Power | 28.75 kW |
| Control System | PLC and MCC |
| Contact Materials | Food-grade stainless steel |
| Key Features | Self-cleaning barrel, forced gearbox lubrication, non-stop cutting |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional corn flakes breakfast cereal | Corn grits, corn flour |
| Fortified breakfast cereal | Corn, rice, wheat flour blends with vitamin premix |
| Sugar-coated and chocolate-coated flakes | Corn base with sugar syrup or chocolate spray |
| Puffed corn snack variants | Corn, rice, soya bean, peanut, walnut blends |
| Multi-grain flake cereal | Corn, wheat, oat composite formulations |
What "Rated Output" Hides About Corn Flake Extrusion
The number on the nameplate means nothing until you test the buyer’s actual corn grits at production moisture.
I spent a full week on a client’s floor recalibrating screw elements and die gaps because their corn flour particle size didn’t match the sample we trialed. The flakes came out uneven in thickness, and after baking the breakage rate made the product unsaleable. That line was rated for a capacity that simply did not hold on their raw material. Every corn flakes extrusion production line must be validated against the specific grit granularity, moisture content, and starch composition the buyer will actually run day after day. [NEED_CITE: effect of particle size distribution on twin-screw extrusion consistency]
Barrel Temperature Profiling and Starch Gelatinisation
Corn flakes demand a precise degree of starch gelatinisation — too little and the dough won’t hold together through the press rollers; too much and the extrudate sticks, producing ragged edges that shatter during baking. The twin-screw co-rotating design on the MT series allows independent barrel heating zones so that temperature ramps gradually from the feed section through the metering and cooking sections. This staged heat input, combined with controlled steam or water injection at the mixer, gives the operator authority over the gelatinisation window rather than forcing a single thermal compromise across the entire barrel length.
Die Geometry and Flake Expansion Control
The die plate determines how the extrudate strand exits the barrel — its orifice diameter, land length, and face angle all influence the expansion ratio and surface skin formation. For corn flakes, a controlled low-expansion profile is essential because the strand must pass through the flaking rollers without collapsing or ballooning. Our die design process starts with the buyer’s target flake thickness and bulk density, then works backward to specify the land length and orifice geometry. This is where a generic die copied from another product format produces flakes that either puff too much in the oven or come out hard and glassy. [NEED_CITE: relationship between die land length and extrudate expansion ratio in cereal processing]
Reading the Power and Dimension Data
The installed power versus real power gap across the MT-65 through MT-85 range reflects motor sizing for peak startup torque rather than continuous draw — this distinction matters when sizing your transformer and dedicated circuit. The physical length difference between the MT-65 at 12 meters and the MT-85 at 28 meters is driven by barrel section count and downstream conveyor integration, which directly affects the residence time of the dough inside the extruder. Longer barrels allow more gradual shear and heat input, giving better control over starch conversion in high-throughput runs. The press roller width of 510 mm sets the maximum strand width that can be flattened in a single pass, which in turn determines how many extruder strands the press can handle simultaneously.
When the Wrong Configuration Costs You a Production Run
A screw profile designed for puffed snacks pushes high expansion and low density — the exact opposite of what corn flakes require. Run that configuration on a flake line and the extrudate balloons before it reaches the press, producing thin, brittle flakes that powder in the packaging. Similarly, if the flaking roller gap isn’t matched to the extrudate diameter and moisture level, you get either unflattened pellets or over-compressed sheets that won’t crisp properly in the oven. These mismatches rarely show up during a short factory acceptance test. They surface three days into continuous production when the raw material batch changes slightly and the process window collapses. [NEED_CITE: common failure modes in cereal flake extrusion from screw mismatch]
Why Source This Corn Flakes Extrusion Production Line Here
The screw configuration and die design are specified to the buyer’s raw material formulation and target flake density, not pulled from a standard library. An in-house testing workshop allows trial runs on the customer’s actual corn grits before the line ships, so expansion ratio and flake texture are confirmed in advance. Throughput is matched across every station — mixer, extruder, press, oven, and coating drum — under one supplier, eliminating the bottleneck that appears when stations are assembled from separate vendors. The PLC and MCC control architecture is confirmed for the buyer’s voltage, frequency, and operator language before production begins. Pre-sales consultation extends through on-site installation, commissioning, and ongoing wear part supply for screws and dies.
Documentation & Verification
- Line layout with capacity calculation matched to your corn grit specification
- Screw and die configuration record tied to your target flake density
- Trial run report on your raw material before shipment
- Electrical schematic with confirmed voltage and frequency
- Operation and maintenance manual with wear parts list
- CE declaration of conformity and ISO certificate
Installation, Commissioning & Support
- MT-85 requires a 28-meter linear floor space with level concrete foundation
- Dedicated power circuit sized to installed kilowatt rating per model
- Extruder ships in modular barrel sections for field assembly
- First-run parameter setting includes barrel zone temperatures and roller gap
- Operator training covers screw element replacement and self-cleaning procedure
- Wear parts inventory list for screws, dies, and press roller bearings
- Gas oven commissioning includes burner calibration and dual-side heat verification
What We Need to Move Forward
Send us your corn grit or flour specification sheet including particle size distribution, moisture range, and any vitamin or mineral premix additions. Tell us your target flake thickness, bulk density, and whether you plan to run sugar-coated or plain variants. We also need your facility voltage and frequency, plus available floor length and ceiling height so the line layout fits your building on the first drawing.
Frequently Asked Questions
Q: How is screw configuration specified to my raw material and target flake density?
A: We start with your corn grit particle size, starch content, and moisture level, then select screw element types — conveying, kneading, and reverse-pitch — to achieve the gelatinisation degree your flake requires. The configuration is documented and can be adjusted if your raw material source changes.
Q: What barrel temperature profile is needed for proper starch gelatinisation in corn flakes?
A: Corn flakes typically need a gradual temperature ramp across multiple barrel zones, starting moderate at the feed section and rising through the cooking zones. The exact setpoints depend on your corn variety and moisture content, which we validate during the pre-shipment trial run.
Q: How do you match extruder output with press capacity and oven throughput?
A: Every station is sized so the press roller speed, oven belt length, and coating drum volume all align with the extruder’s real output on your material. This prevents the bottleneck that occurs when one station runs faster than the next can handle.
Q: Can I run a trial with my own raw material before the line ships?
A: Yes. Our testing workshop accepts your corn grits or flour blend for a production trial. We measure expansion ratio, flake density, and surface texture against your specification, and adjust screw elements or die geometry before the extruder leaves the factory.