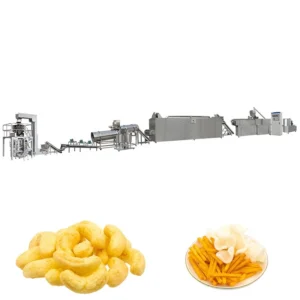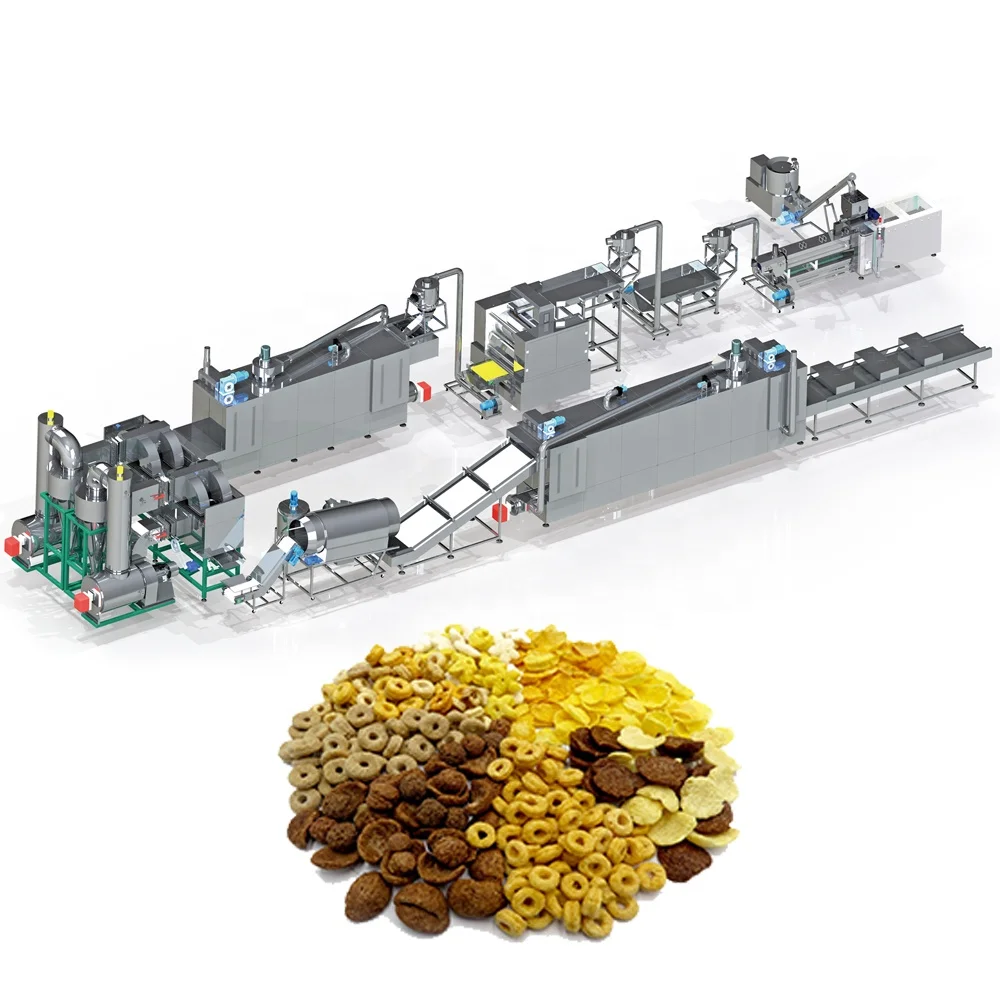
Screw Geometry Engineering — Every MT-65 / MT-70 / MT-75 / MT-85 corn flakes extrusion line ships with screw modules arranged specifically for the buyer’s grain formulation, not copied from a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line / Breakfast Cereal Extrusion Line |
| Screw Type | Twin-screw, co-rotating, sectional modules |
| Output Capacity (MT-65) | 120–150 kg/h (basis not stated in source — confirm raw material, moisture and flake thickness) |
| Output Capacity (MT-70) | 200–250 kg/h (basis not stated in source — confirm raw material, moisture and flake thickness) |
| Output Capacity (MT-75) | 300–400 kg/h (basis not stated in source — confirm raw material, moisture and flake thickness) |
| Output Capacity (MT-85) | 400–500 kg/h (basis not stated in source — confirm raw material, moisture and flake thickness) |
| Installed Power (MT-65) | 84 kW (Real: 59 kW) |
| Installed Power (MT-70) | 132 kW (Real: 92 kW) |
| Installed Power (MT-75) | 186 kW (Real: 140 kW) |
| Installed Power (MT-85) | 239 kW (Real: 167 kW) |
| Overall Dimensions (MT-65) | 12000 × 1200 × 2200 mm |
| Overall Dimensions (MT-70) | 23000 × 1500 × 2200 mm |
| Overall Dimensions (MT-75) | 24000 × 1500 × 2800 mm |
| Overall Dimensions (MT-85) | 28000 × 1500 × 2800 mm |
| Gear Box Lubrication | Oil forced automatic lubrication system |
| Extruder Self-Cleaning | Yes |
| Cutting System | Non-stop cutting |
| Flaking Roller | Large-diameter roller with cooling system; adjustable gap |
| Oven Type | High-temperature gas oven, dual-side baking |
| Sugar Coating | Spraying system with melting tank, temperature-keeping roller |
| Control System | PLC and MCC available |
| Certification | CE, ISO |
| Warranty | 1 year complete; life-time maintenance service |
Application Suitability
| Application | Material or Output |
|---|---|
| Standard corn flakes | Corn grits, corn flour at controlled moisture |
| Sugar-coated corn flakes | Corn grits with sugar syrup coating downstream |
| Multi-grain breakfast flakes | Blends of rice flour, wheat flour, soya bean |
| Fortified cereal flakes | Grain base with vitamin-mineral premix introduced during extrusion |
| Corn puff snacks (alternate die) | Corn, rice, wheat flour with varied die shapes |
What a Generic Screw Build Really Costs You in Bowl-Life
Flake density and crispness retention depend entirely on matching screw geometry to the grain you actually run.
I once stood in a Colombian plant watching a brand-new line push out corn flakes that snapped like glass shards instead of crunching. The factory had stocked high-amylose corn, but the extruder arrived configured for standard dent corn — the gelatinisation window was completely off. Three days of reprofiling barrel zones and adjusting die clearance later, the line finally produced flakes that held up in milk. That gap between what a catalogue promises and what a specific raw material demands is where most corn flakes extrusion line projects quietly fail. [NEED_CITE: starch gelatinisation behaviour across amylose content ranges]
Barrel Temperature Profiling for Starch Control
The MT corn flakes extrusion line uses independently heated barrel zones that let you build a temperature curve matching the exact gelatinisation onset of your grain blend. Corn with higher amylose content requires a steeper ramp in the mid-barrel cooking section, while rice-heavy blends need gentler heating to avoid premature melt fracture. Getting this curve wrong means either undercooked pellets that shatter at the flaking roller or over-gelatinised melt that sticks to the die face.
Die Geometry and Expansion Behaviour
Die orifice diameter and land length determine the expansion ratio of the extrudate rope as it exits the barrel. For corn flakes, you want minimal radial expansion and controlled axial growth so the pellet flattens uniformly between the rollers. The sectional screw modules allow reconfiguration of the final metering section — adjusting the balance between forward-transport elements and restrictive kneading blocks — to dial in the melt pressure the die needs. [NEED_CITE: twin-screw die land length and melt pressure relationship]
Reading the Specs That Actually Matter
The co-rotating twin-screw design with sectional modules is the engineering core here. Each module — whether a conveying element, kneading block, or reverse-screw segment — can be swapped to alter residence time and shear intensity across the barrel length. The oil forced automatic lubrication system keeps the gearbox stable during long shifts of high-shear cooking, preventing torque spikes that would otherwise degrade screw engagement. The large-diameter flaking roller with integrated cooling is equally critical: it sets flake thickness while chilling the pellet surface, which stabilises moisture distribution before the high-temperature gas oven takes over for dual-side baking.
When the Wrong Flaking Roller Gap Wrecks Your Entire Batch
A flaking gap set too wide leaves pellets under-compressed, producing thick flakes that bake unevenly and go soggy within seconds of hitting milk. Set it too narrow and the pellet fractures instead of flattening, generating fines that burn in the oven and foul the sugar coating drum. I have seen entire production runs scrapped because the roller gap was calibrated for a different corn variety than what the buyer’s silo actually held. Without a trial run on the real raw material, these settings remain guesswork. [NEED_CITE: flake thickness impact on bowl-life in breakfast cereal testing]
Why the Engineering Conversation Starts Here
The screw configuration and die design are specified to the buyer’s actual grain formulation, not borrowed from a standard template. An in-house testing workshop runs your raw material through the line before shipment, generating a trial report that documents the barrel temperature profile, screw arrangement, and resulting flake density. The PLC and MCC control architecture is confirmed against your plant voltage and frequency before the panel is wired. Throughput is calculated across every station — extruder, flaking press, oven, sugar spraying — so no single unit bottlenecks the line. CE and ISO certification is maintained across the build, with full documentation provided at delivery.
Documentation & Verification
- Screw and die configuration record matching your grain formulation at time of build
- Trial run report on your raw material documenting barrel profile and flake density
- Line layout and capacity calculation balancing throughput across all stations
- Electrical schematic with voltage and frequency confirmed to your plant utility
- Machine specification sheet covering every station from mixer to sugar coating
- Operation and maintenance manual with wear parts list for screws, dies, and rollers
Installation, Commissioning & Support
- Foundation and utility planning based on the specific line footprint (MT-65 through MT-85)
- Dedicated power circuit sized to installed kW rating with voltage and frequency matched
- On-site assembly of flaking roller, oven, and sugar coating stations by MT engineers
- First-run parameter tuning: barrel zones, screw speed, die clearance, roller gap
- Operator training covering formulation changeover and self-cleaning procedure
- Wear parts supply for screws, dies, and flaking roller surfaces with ongoing maintenance
What We Need from You to Configure the Line
Share the specific grain or grain blend you plan to extrude, including amylose content if available, along with your target flake thickness and whether you need sugar coating downstream. We also need your plant voltage, frequency, and control language preference so the PLC and MCC panel arrives ready for commissioning. If you can send a sample of your raw material, we will run it in the testing workshop and include the trial report with the quotation.
Frequently Asked Questions
Q: How is screw configuration selected for different grain formulations?
A: The sectional co-rotating twin-screw modules are rearranged based on your grain’s starch composition and target gelatinisation degree. High-amylose corn requires more kneading blocks in the cooking zone, while rice-dominant blends use gentler conveying elements. The exact module sequence is documented in your configuration record for future replication.
Q: What barrel temperature zones are available and how do they affect gelatinisation?
A: Multiple independently controlled heating zones run along the barrel length, each set to a specific temperature to build a profile matching your grain’s gelatinisation window. Too aggressive a ramp causes melt fracture at the die; too gradual a ramp leaves starch under-cooked, producing brittle flakes.
Q: How does the flaking roller gap and cooling system influence final density?
A: The adjustable roller gap sets flake thickness directly, while the internal cooling circuit stabilises the pellet surface temperature before oven baking. Thinner flakes bake faster and achieve greater crispness, but require precise gap control to avoid fracture during pressing.
Q: Can a trial run be performed on my own raw material before shipment?
A: Yes. The in-house testing workshop runs your actual grain blend through the extruder, flaking press, and oven at production-relevant settings. You receive a trial run report documenting screw configuration, barrel temperature profile, die selection, and the resulting flake texture and density.
Q: How are die design and moisture injection calibrated for target expansion?
A: Die orifice diameter and land length are selected to control radial expansion of the extrudate rope. Moisture content at the barrel inlet is adjusted alongside screw speed to set the melt viscosity entering the die, balancing expansion against the pellet integrity needed for clean flaking.