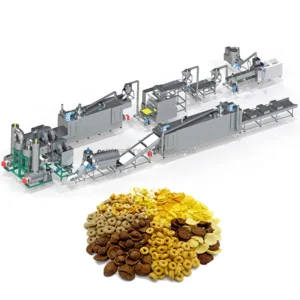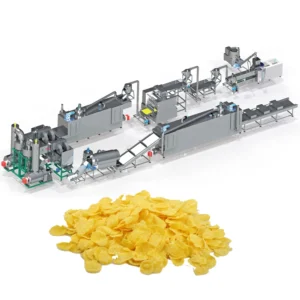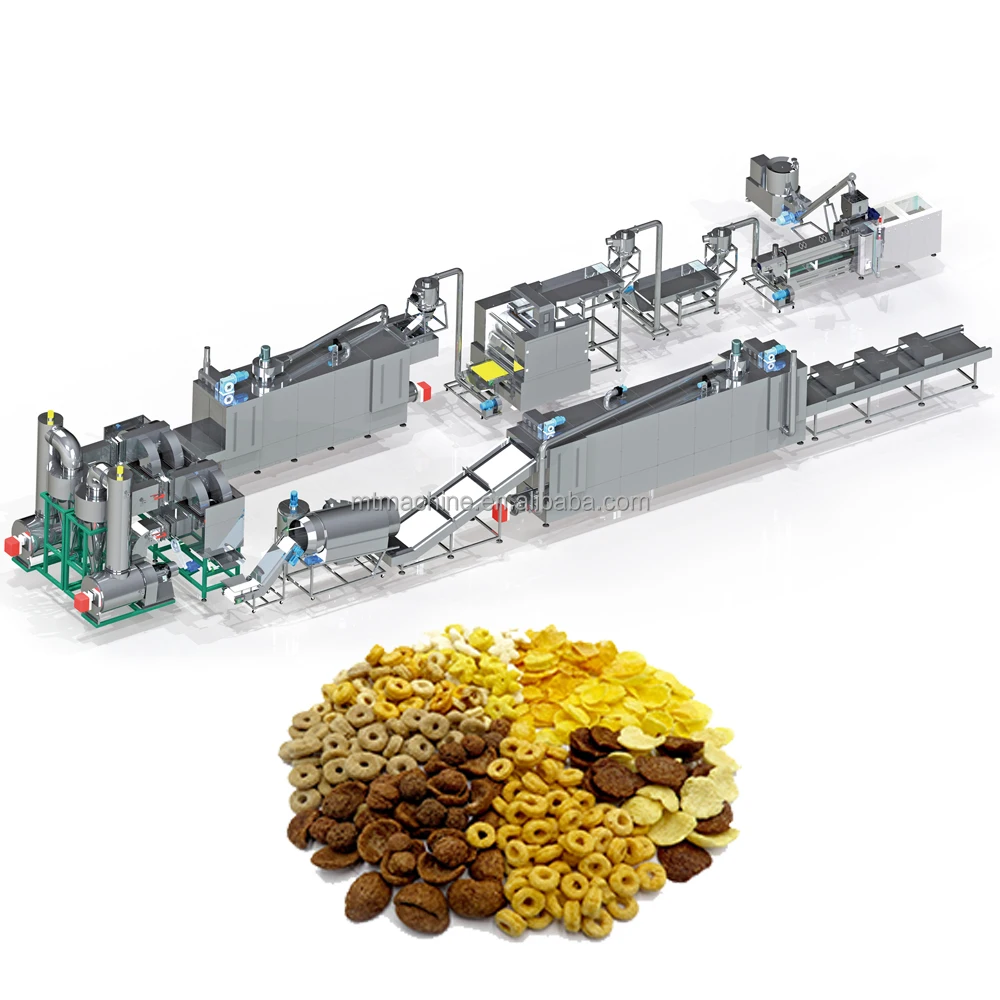
Precision-Matched Extrusion — screw configuration and barrel temperature profile are set against the buyer’s actual grain powder before the line ships, ensuring starch gelatinisation holds across every production run.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line with Twin Screw Extruder |
| Model Options | MT70 / MT75 / MT85 |
| Screw Type | Twin-screw |
| Installed Power | MT70: 160 kW; MT75: 210 kW; MT85: 190 kW |
| Power Consumption | MT70: 120 kW; MT75: 150 kW; MT85: 140 kW |
| Output Capacity | MT70: 150–200 kg/h (basis to be confirmed); MT75: 300–500 kg/h (basis to be confirmed); MT85: 300–400 kg/h (basis to be confirmed) |
| Overall Dimensions (L×W×H) | MT70: 41 × 1.5 × 2.2 m; MT75: 45 × 1.5 × 3.5 m; MT85: 43 × 1.5 × 3.2 m |
| Control System | PLC and MCC (extruder); PLC with hydraulic system (flaking unit) |
| Flaking Machine Drive | Double motors for separate roller driving; hydraulic system for double rollers |
| Flaking Temperature Control | Infrared sensor for even pipe temperature |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air roasting with vibrating pan, high-temperature spraying tubes, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Standards | CE (since 2014), ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn powder with controlled moisture and starch profile |
| Sugar-coated corn flakes | Corn, rice, or wheat base with sugar spraying and coating stages |
| Shaped breakfast cereals | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart via die adjustment |
| Multi-grain flake production | Blends of oat, barley, wheat, and rice powder |
| Fortified cereal flakes | Grain powder blended with nutritional premix |
What "Nominal Capacity" Means When Your Grain Does Not Cooperate
A corn flakes extrusion production line rated at 400 kg/h on one corn variety may deliver far less on yours if screw configuration and barrel zones were never matched to it.
Every corn flakes extrusion production line specifications how to choose decision starts with a capacity number on a quote. I spent years on the buyer side reviewing those numbers, then moved to the seller side and discovered why they often fail on site. A line built for Shandong yellow corn with a fixed barrel profile will behave differently when the buyer switches to local white corn in Southeast Asia or Africa — starch gelatinisation temperature shifts, moisture absorption changes, and the flakes come out uneven in thickness with mottled colour after roasting [NEED_CITE: starch gelatinisation temperature variance across corn cultivars]. The capacity figure on paper assumes a raw material that was never tested. Before any throughput claim is meaningful, the screw combination and die design must be validated against the specific grain powder the buyer will actually run.
Barrel Temperature Zones and Starch Gelatinisation Control
Twin-screw extrusion gives process engineers independent control over shear, residence time, and heat input across multiple barrel zones. For corn flakes, the goal is partial gelatinisation — enough to bind the dough sheet but not so much that the flake loses its structural bite. When the corn flakes extrusion production line specifications how to choose discussion skips barrel profiling, the line may over-gelatinise the dough, producing flakes that shatter during roasting or stick to the flaking rollers.
Screw Configuration Against Grain Variability
Different corn varieties carry different amylose-to-amylopectin ratios, and that ratio determines how the starch responds to heat and shear inside the barrel. A screw combination designed for high-amylose corn will under-process a waxy variety, leaving hard centres that refuse to flatten evenly on the flaking unit. Matching screw elements — kneading blocks, reverse elements, and conveying sections — to the buyer’s actual grain powder is the single most consequential step before the machine leaves the factory [NEED_CITE: screw element configuration impact on extrudate texture in cereal processing].
Reading the Numbers That Actually Matter
The installed power across the MT-series ranges from 160 kW to 210 kW, and power consumption sits between 120 kW and 150 kW depending on model. These figures determine the thermal and mechanical energy available inside the barrel — higher installed power supports the sustained shear needed for denser grain blends or higher-moisture formulations. The PLC and MCC control system logs barrel zone temperatures and screw speed continuously, so process engineers can reproduce a validated recipe batch after batch. On the flaking unit, the infrared sensor monitors roller surface temperature in real time, preventing the dough sheet from cooling unevenly between passes. The hydraulic double-roller system with separate motor drives applies consistent pressure across the full roller width, which directly governs final flake thickness uniformity.
When Mismatched Stations Create Invisible Bottlenecks
A line where the extruder runs at full output but the dryer cannot keep up forces the operator to slow the entire system down, silently cutting real throughput below the quoted figure. I have watched a roasting oven with a single circulating fan fail to maintain uniform temperature across a wide vibrating pan, leaving some flakes under-toasted while others scorch [NEED_CITE: airflow uniformity requirements in cereal roasting ovens]. The dual circulating fans and cyclone dust removal on the MT-series roasting oven address this, but only if the oven capacity was calculated against the extruder’s actual output on the buyer’s material — not a generic line drawing.
Why Engineering Validation Before Shipment Changes Outcomes
The testing workshop exists so that screw configuration, die selection, and barrel profiles are proven on the buyer’s grain before the line ships, not debugged on a factory floor thousands of kilometres away. Each MT-series line leaves with a screw and die configuration record tied to a specific raw material and target flake density. The trial run report documents moisture content, barrel zone settings, screw speed, and flake thickness achieved during that test. This is the difference between arriving on site and producing saleable flakes on day one versus spending weeks adjusting parameters while raw material goes to waste.
Documentation & Verification
- Line layout and capacity calculation matched to your grain powder and target flake density
- Screw and die configuration record specifying element arrangement for your raw material
- Trial run report on your actual grain powder from the in-house testing workshop
- Electrical schematic with voltage and frequency confirmed to your facility specification
- CE declaration of conformity and ISO certificate included with shipping documentation
- Operation and maintenance manual with wear parts list for screws, dies, and rollers
Installation, Commissioning & Support
- Foundation plan sized to the line footprint (up to 45 m length for MT75) and vibration load from extruder and roasting oven
- Dedicated power circuit rated to 210 kW installed capacity with voltage and frequency matched to local grid
- Line arrives in modular sections for sequential assembly — extruder, flaking unit, dryer, roasting oven, coating system
- On-site commissioning includes barrel zone calibration and screw speed tuning against your production grain
- Operator training covers PLC interface navigation, recipe storage, and hydraulic flaking pressure adjustment
- Wear parts list identifies screw elements, die plates, and flaking roller surfaces with replacement intervals
Preparing Your Inquiry
To move from a general corn flakes extrusion production line specifications how to choose conversation into a firm line configuration, share your primary grain type and any blend ratios, your target hourly output on that specific material, and the moisture range of your incoming flour. Include your facility voltage, frequency, and preferred control language. If you plan to produce both natural and sugar-coated variants, confirm that upfront so the coating and secondary drying stations are sized into the layout from the start.
Frequently Asked Questions
Q: How is extruder screw configuration specified to a buyer’s grain powder?
A: The screw combination — kneading blocks, reverse elements, and conveying sections — is selected based on the buyer’s grain type, amylose content, and target flake density. A configuration record is generated documenting element arrangement and die specification tied to the validated recipe. This record ships with the line so settings remain reproducible across production runs.
Q: What does the in-house trial run cover before shipment?
A: The buyer’s actual raw material is run through the extruder, flaking unit, and dryer in the testing workshop. The trial documents barrel zone temperatures, screw speed, moisture profile, and resulting flake thickness and texture. A full report is provided, confirming that the line produces the target corn flakes extrusion production line specifications how to choose outcome on that specific grain.
Q: How do barrel zones and moisture control affect starch gelatinisation?
A: Each barrel zone is independently heated, allowing the process engineer to stage gelatinisation gradually. Moisture is introduced at controlled points to modulate shear and heat transfer. Too much gelatinisation makes flakes brittle during roasting; too little leaves hard centres. The PLC logs all zone settings for batch-to-batch repeatability.
Q: How is throughput balanced across extrusion, flaking, drying, and roasting?
A: Line layout and capacity calculation ensure each station handles the extruder’s actual output on the buyer’s material. The roasting oven uses dual circulating fans for uniform heat distribution, and the dryer is sized to match moisture removal requirements. A bottleneck at any station reduces real output below the extruder’s nominal rate.
Q: What documentation accompanies the line at delivery?
A: The package includes the screw and die configuration record, electrical schematic with confirmed voltage and frequency, trial run report on buyer’s raw material, CE declaration, ISO certificate, factory test record, and an operation manual with a complete wear parts list for ongoing maintenance planning.