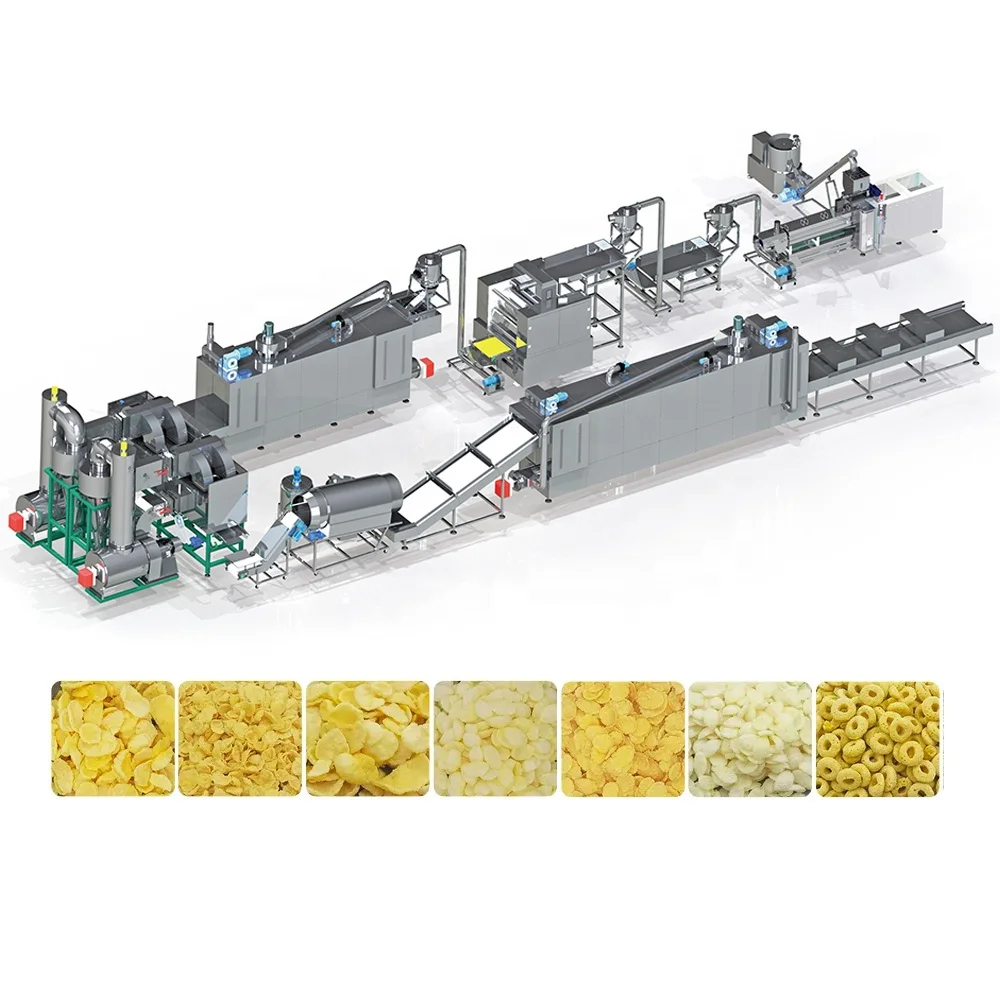
Sectional Screw Modules — Each MT-75 barrel section is matched to your grain blend’s gelatinisation curve, eliminating the guesswork that turns a promising cereal recipe into dense, unsaleable output.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-75 |
| Product Type | Twin Screw Extruder Breakfast Cereal Production Line |
| Screw Type | Co-rotating twin screw, sectional modules |
| Extruder Function | Continuous gelatinisation, mixing, de-gassing, cooking, forming |
| Mixer Output | 10–30 kg per load |
| Mixer Power | 4 kW |
| Mixer Tank Size | φ600 × 500 mm |
| Mixer Dimensions | 1000 × 800 × 1200 mm |
| Screw Conveyor Power | 0.75 kW |
| Corn Flakes Press Power | 16.12 kW |
| Corn Flakes Press Roller | 510 × 310 × 1050 mm |
| Corn Flakes Press Features | Adjustable roller gap, integrated cooling system |
| High-Temperature Oven Dimensions | 4.5 × 1.4 × 1.8 m |
| Oven Heating Method | Gas-fired, both-side baking |
| Sugar Spraying System Power | 28.75 kW |
| Sugar Spraying Roller | φ600 × 2700 mm |
| Sugar Spraying Features | Melting tank, temperature-keeping roller, conveyor feed |
| Die Configuration | Interchangeable moulds: ring, ball, star, stick and custom shapes |
| Contact Material | Stainless steel on all food-contact parts |
| Control System | Separate controller box (PLC or MCC available on request) |
| Voltage Options | Configurable per market, e.g. 3ph 380V 50Hz, 3ph 415V 60Hz, 3ph 220V 60Hz |
| Certification | CE (since 2014); ISO certified |
| Output Capacity | Basis to be confirmed against buyer’s raw material, moisture and product shape |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional corn flakes | Corn grits and corn flour, pressed and baked to a crisp sheet |
| Chocolate-flavoured hoops (Choco Hoops) | Corn flour blended with cocoa powder and whole wheat |
| Fruit loop cereal rings | Multi-coloured grain doughs with fruit flavouring added post-extrusion |
| Fortified breakfast cereals | Grain blends supplemented with vitamin and mineral premixes |
| Sugar- or honey-coated cereal snacks | Any extruded ring, ball or star shape finished through the sugar spraying system |
What "Rated Capacity" Means When Your Grain Blend Changes
A line is only as fast as its slowest matched station — and capacity shifts the moment you alter moisture, fat or protein in the recipe.
I once watched a Middle East plant switch from a standard corn flour recipe to a whole wheat and cocoa blend for Choco Hoops. Die pressure spiked within the first hour, and the rings came out hard enough to chip a tooth. The extruder was rated for the nominal output on corn flour, but nobody had mapped the new starch behaviour through the barrel zones. The fix was not a bigger motor — it was rebuilding the barrel temperature curve and redefining the moisture window from scratch on site. [NEED_CITE: how raw material moisture and composition affect twin-screw extrusion throughput]
That is the gap this twin screw extruder breakfast cereal production line is built to close. Before the line ships, your actual grain blend runs through the in-house testing workshop so screw profile, die selection and temperature settings are documented — not assumed.
Barrel Temperature Profiling Across the Cooking Zones
The MT-75 extruder uses sectional screw modules inside a multi-zone barrel. Each zone can be heated or cooled independently, which matters when a cereal recipe demands rapid gelatinisation in one section and gentle de-gassing in the next. A single-screw unit would push material through with less shear control, making it difficult to achieve the open cell structure that keeps corn flakes crisp after milk is poured on.
Co-rotating twin screws intermesh to create a self-wiping action. This keeps sticky doughs — especially those containing sugar, cocoa or oat flour — from building up on the flight surfaces and causing burn spots that discolour the final product.
Die Geometry and Product Density Control
The interchangeable die plates determine not just shape but also expansion ratio. A ring die with a thin wall produces a lighter, faster-expanding hoop; a solid ball die holds more moisture inside and requires longer drying. On the twin screw extruder breakfast cereal production line, die selection is recorded against your recipe during the pre-shipment trial so that switching between corn flakes and Choco Hoops is a documented changeover, not a day of trial and error on the factory floor. [NEED_CITE: relationship between die land length and extrudate expansion in cereal processing]
Reading the Specs That Actually Matter
The mixer delivers 10–30 kg per load, which sets the batching rhythm for the entire line. If your shift plan calls for shorter cycles, the mixer becomes the pacing station rather than the extruder. The corn flakes press uses a 510 × 310 × 1050 mm roller pair with adjustable gap and an integrated cooling circuit; this combination controls flake thickness and prevents the sheeted pellet from sticking to the roller surface at high line speeds. Downstream, the gas-fired oven measures 4.5 m in length with both-side baking — long enough for the moisture gradient inside a flake to equalise, short enough to avoid over-browning the surface before the core is dry. The sugar spraying system’s φ600 × 2700 mm temperature-keeping roller ensures the syrup stays fluid long enough to coat evenly without crystallising on contact.
When Downstream Stations Cannot Keep Up
A frequent complaint on poorly matched lines is the extruder running at full output while the dryer or coating drum creates a backlog. Pellets pile up on the conveyor, cool unevenly and develop surface cracks that show up as broken flakes in the packing station. On this line, every station from the screw conveyor through the vibrating spreader to the cooling conveyor is throughput-matched during the layout phase so the bottleneck stays where it belongs — at the extruder, where you control it through screw speed and feed rate. [NEED_CITE: common bottlenecks in extruded breakfast cereal lines]
Why Buyers Choose This Line Configuration
Complete throughput matching from batching to packing under one supplier means you avoid the finger-pointing that happens when separate vendors blame each other for a line that will not hold its quoted output. Screw and die configurations are specified to your grain formulation, not copied from a generic build. Every line goes through a pre-shipment trial on your raw material in the in-house testing workshop, so the trial run report travels with the machine rather than starting after installation. Voltage, frequency and control language are confirmed before production begins, avoiding the commissioning delays that arise when a 50 Hz motor lands in a 60 Hz plant. CE and ISO certification are maintained across the build, which simplifies customs clearance and local authority sign-off in regulated markets.
Documentation & Verification
- Line layout drawing with throughput calculation matched to your grain blend and target cereal shape
- Screw and die configuration record specific to your recipe, including barrel zone temperature settings
- Trial run report on your raw material produced in the testing workshop before shipment
- Electrical schematic with confirmed voltage, frequency and control language for your market
- CE declaration of conformity and ISO certificate for customs and local compliance
- Operation and maintenance manual covering daily cleaning and screw module changeover
Installation, Commissioning & Support
- Foundation plan accounts for the 4.5 m oven length and vibrating spreader footprint
- Dedicated circuit sizing based on the 28.75 kW sugar spraying system and 16.12 kW press loads
- Pre-assembled modules reduce on-site mechanical assembly time
- First-run parameter setting covers barrel temperature curve and moisture window for your recipe
- Operator training includes screw module swap procedures and die changeover sequence
- Wear parts list identifies screw elements and die plates with reorder specifications
What to Include With Your Inquiry
To size the twin screw extruder breakfast cereal production line correctly, share your primary grain blend and any secondary ingredients such as cocoa, oat or vitamin premix. Specify the cereal formats you plan to run — flakes, hoops, rings or a combination — and the target hourly output at your intended moisture level. Confirm the voltage, frequency and preferred control language at your facility, along with available workshop length and ceiling height so the layout can be drafted without assumptions.
Frequently Asked Questions
Q: How is line capacity verified against my specific grain blend and moisture content?
A: Your raw material is run through the in-house testing workshop before shipment. The trial records actual throughput, expansion ratio and moisture loss across each station. You receive a test report with the documented screw profile, barrel temperature curve and die selection so the installed line matches the proven setup.
Q: Can the extruder produce both flakes and ring shapes on one line?
A: Yes. The MT-75 accepts interchangeable die plates for ring, ball, star and stick shapes. For flakes, extruded pellets pass through the corn flake press with its adjustable roller gap. Switching formats requires a die change and, where needed, a revised barrel temperature profile — both documented during the pre-shipment trial.
Q: How do you confirm voltage, frequency and control language before shipment?
A: During the specification confirmation stage, you provide your local supply details and preferred interface language. The electrical schematic is updated accordingly, and the factory test runs on the correct voltage configuration. This prevents commissioning delays caused by mismatched motors or unreadable HMI screens on arrival.
Q: What happens during the in-house trial run, and do I receive the test report?
A: Your grain blend is batched in the mixer, extruded through the configured screw profile, and processed through the downstream stations that mirror the full line. The trial run report documents throughput, product density, moisture at each stage and final texture. This report ships with the equipment.
Q: How are downstream stations throughput-matched to the extruder output?
A: Each station — dryer, oven, sugar spraying system, cooling conveyor — is selected during the layout phase based on the extruder’s proven output on your recipe. The line capacity calculation document shows the dwell time and belt speed at every station, so no single unit creates a bottleneck under normal operating conditions.