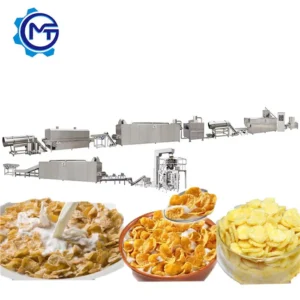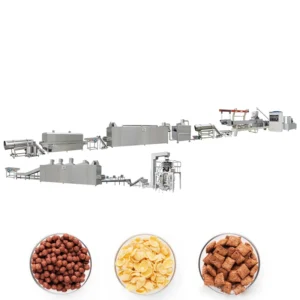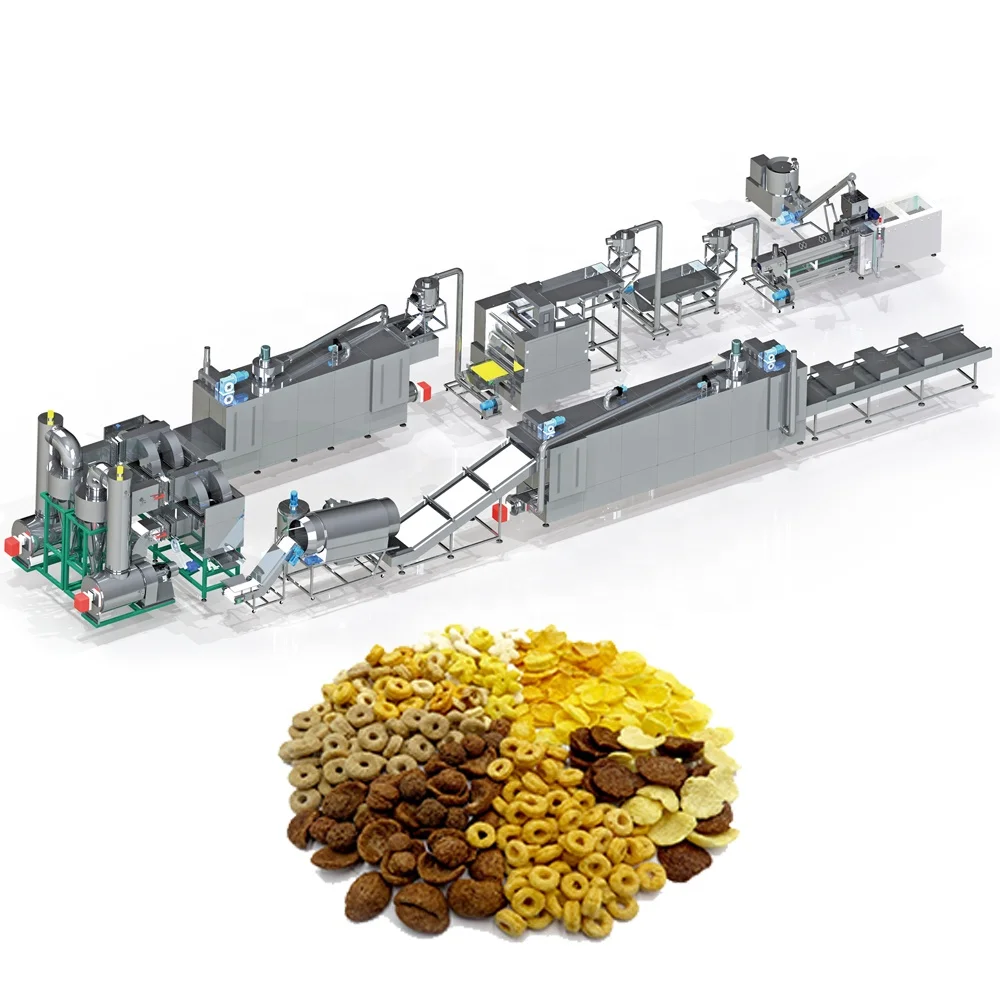
Precision Extrusion Engineering — screw configuration and die geometry specified to your grain formulation, validated through in-house trial runs on actual customer raw material before any line is cleared for shipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-65 |
| Product Type | Twin-Screw Extrusion Corn Flakes Production Line |
| Screw Type | Co-rotating twin-screw, sectional modules |
| Mixer Output | 10–30 kg/load |
| Mixer Power | 4 kW |
| Mixer Tank Size | φ600 × 500 mm |
| Screw Conveyor Power | 0.75 kW |
| Corn Flakes Press Machine Power | 16.12 kW |
| Press Roller Size | 510 × 310 × 1050 mm |
| Press Roller Adjustment | Adjustable roller distance for flake thickness control |
| Oven Dimensions | 4.5 × 1.4 × 1.8 m (basis to be confirmed) |
| Oven Heating Source | Gas-fired, both-side baking |
| Sugar Spraying System Power | 28.75 kW |
| Sugar Spraying Roller Size | approx. φ600 × 2700 mm |
| Contact Material | Stainless steel (food-grade) |
| Control System | Separate controller box for press machine; PLC/MCC availability to be confirmed |
| Voltage & Frequency | Customizable (e.g., 3ph 380V/50Hz, 3ph 415V/60Hz, 3ph 220V/60Hz) |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Plain corn flakes for retail breakfast cereal packaging | Corn grits and corn flour |
| Multi-grain breakfast flakes | Blends of corn, rice, and oat powders |
| Sugar-coated or honey-coated cereal flakes | Grain pellets with sugar or honey spray coating |
| Alternative cereal shapes (rings, balls, stars, sticks) | Grain formulations with interchangeable die moulds |
| Nutritional breakfast cereals | Grain base with incorporated vitamin and mineral premixes |
Why Starch Gelatinisation Defines Your Corn Flake — Not Just the Recipe
A flake that shatters in the bowl or turns to mush in milk is a process design failure, not a flour problem.
I spent the better part of a week in a humid Jakarta plant watching corn flakes come off the press looking like broken glass. The recipe was correct. The brand-new line was rated for the target throughput. What nobody had checked was whether the screw profile matched the high-fat local corn variety — the starch never fully gelatinised inside the barrel, so the pellet left the die undercooked. When it hit the flaking rollers, it cracked instead of flattening. That is the difference corn flakes extrusion line technology makes when the thermal and mechanical profile inside the barrel is engineered to the specific raw material, rather than borrowed from a generic build [NEED_CITE: starch gelatinisation temperature thresholds for maize varieties].
Barrel Temperature Zones and the Gelatinisation Window
The co-rotating twin-screw design on the MT-65 uses sectional modules, meaning each barrel zone can be set to a different thermal target. Starch gelatinisation in corn typically begins around 62–72 °C, but the exact window shifts depending on fat content, particle size, and moisture. The corn flakes extrusion line technology here relies on matching those zones to the buyer’s specific formulation, so the pellet exits the die at the correct degree of cook — pliable enough to flatten under the press rollers without tearing, yet structured enough to hold its shape through the oven.
Die Geometry and Pellet Density Control
The die plate determines the cross-section of the extruded pellet before it reaches the flaking station. A die with too large an orifice produces a pellet that spreads unevenly under the rollers, creating thin edges that burn during baking and thick centres that stay doughy. The die design must be specified alongside the screw configuration so that expansion ratio, moisture content, and pellet density all converge at the target values the market expects for retail-grade corn flakes [NEED_CITE: die land length effects on extrudate density in cereal processing].
Reading the Press and Oven Parameters
The press machine runs at 16.12 kW with a 510 × 310 × 1050 mm roller set and adjustable roller distance — this is where flake thickness is physically determined. Thickness directly influences bowl-life: thinner flakes absorb milk faster, thicker flakes stay crunchy longer. Downstream, the gas-fired both-side oven at 4.5 m length provides the uniform radiant heat needed to develop crispness without case-hardening the surface. A single-source dryer would leave the underside under-baked, which is why both-side baking matters for consistent flake texture across the full tray width. The sugar spraying system, with its φ600 × 2700 mm roller, handles coating application after the primary drying stage, allowing the same platform to switch between plain and coated variants.
What Happens When Extrusion Parameters Are Guesswork
When the screw profile is not matched to the raw material, the consequences show up downstream. Undercooked pellets shatter at the press, producing fines that clog the dryer trays and reduce saleable yield. Overcooked pellets emerge from the die with excessive expansion, creating flakes that are too fragile for packing and shipping. Either scenario means the line is running, but the product does not meet the specification the buyer committed to their retail customer. I have seen entire first production runs scrapped because the extrusion parameters were set to a default profile that assumed a standard dent corn, while the buyer was running a waxy variety with a completely different gelatinisation curve [NEED_CITE: raw material variability impact on extruded cereal quality].
Why Procurement Should Start With a Trial Run
The MT-65 line is built around complete throughput matching from the flour mixer through the screw elevator, twin-screw extruder, dryer, press, coating line, and cooling conveyor — every station sized so that no single unit bottlenecks the next. Screw configuration and die design are specified to the buyer’s raw material and target flake density, not pulled from a generic library. Before shipment, the line runs a trial on the customer’s actual raw material in the in-house testing workshop, producing a trial run report that documents the exact screw profile, barrel temperatures, and press settings that achieved the target flake specification. This is how corn flakes extrusion line technology translates from a machine catalogue into a working production asset. The control system is confirmed for the destination market’s voltage, frequency, and operator language before the electrical schematic is finalised, so commissioning starts with the correct parameters already loaded.
Documentation & Verification
- Line layout and capacity calculation showing throughput balance across mixer, extruder, press, dryer, and coating stations
- Screw and die configuration record matched to your specific grain formulation and target flake density
- Trial run report on your raw material documenting barrel temperatures, moisture, and press settings
- Electrical schematic with voltage, frequency, and control language confirmed for your facility
- CE declaration of conformity and ISO certificate included with shipment documentation
- Operation and maintenance manual with wear parts list for screws, dies, and press rollers
Installation, Commissioning & Support
- Foundation planning accounts for the 4.5 m oven length and full line footprint including cooler conveyor
- Electrical supply sized for total connected load including 28.75 kW sugar spraying system and gas supply for oven
- Equipment ships in sectional modules for containerised transport and reassembly at your facility
- Commissioning includes first-run parameter tuning on your raw material with MT engineer on site
- Operator training covers screw module changes, press roller gap adjustment, and oven temperature profiling
- Wear parts list supplied at delivery covering screws, die plates, and press roller surfaces
What to Share When You Enquire
To configure the line accurately, we need your grain formulation details — base material, fat and moisture content, and any vitamin or mineral premixes you plan to incorporate. Your target flake thickness and whether you will run plain, sugar-coated, or both variants on the same line. The voltage and frequency at your facility, along with the control language your operators require. If you have existing upstream milling or downstream packing equipment, share the interface specifications so the line layout accounts for the connection points.
Frequently Asked Questions
Q: How do screw configuration and barrel temperature profile affect starch gelatinisation and final flake density?
A: The sectional screw modules allow zone-specific shear and residence time, while barrel temperature zones control the thermal profile. Together they determine the degree of starch gelatinisation inside the barrel. Under-gelatinised starch produces dense, hard pellets that crack at the press. Over-gelatinised starch creates excessive expansion and fragile flakes. The correct profile is matched to your specific grain variety and moisture content through pre-shipment trial runs.
Q: What determines whether corn flakes achieve proper expansion versus becoming too dense or too fragile?
A: Expansion is controlled by the interplay of moisture content at the die, barrel temperature at the final zone, and die orifice geometry. Higher moisture and temperature increase steam-driven expansion at the die exit. The die land length provides back-pressure that regulates how much the pellet expands before it is cut. Getting these three variables right for your specific formulation is what separates a flake with good bowl-life from one that dissolves or shatters.
Q: How is flake thickness controlled at the press station, and what is typical for retail-grade corn flakes?
A: The press machine features an adjustable roller distance mechanism that sets the gap between the two flaking rollers. The pellet is fed between them and flattened to the set thickness. Retail corn flakes typically fall within a range that balances crispness with milk absorption rate. The exact target depends on your market positioning and whether the flakes will be sold plain or coated.
Q: Can the same extrusion platform process multi-grain formulations like corn-rice-oat blends?
A: Yes, the co-rotating twin-screw design with interchangeable sectional modules allows the screw profile to be reconfigured for different starch systems. Rice starch gelatinises at a different temperature than corn, and oat introduces fat and fibre that change the rheology inside the barrel. Each blend requires its own documented screw configuration and temperature profile, established through trial runs on the actual formulation.
Q: How does gas-fired both-side baking differ from single-source drying for flake crispness?
A: Both-side baking applies radiant heat from above and below the flake layer simultaneously, which drives moisture out evenly through the full flake thickness. Single-source drying tends to case-harden the top surface while the underside retains moisture, creating a flake that feels crisp initially but softens quickly in the bowl. Uniform baking is essential for the consistent crunch that retail consumers expect from breakfast cereal corn flakes.