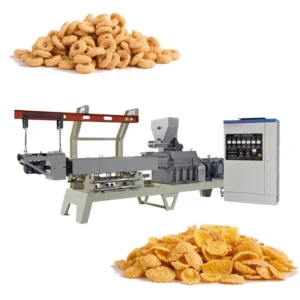
Customized Extrusion Geometry — screw configuration and die design specified to the buyer’s grain blend and target flake thickness, validated through in-house trial runs before shipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Breakfast Cereal Production Line |
| Screw Type | Twin Screw |
| Control System | PLC (flaking machinery section); MCC available per project scope |
| MT70 Installed Power | 160 kW |
| MT70 Power Consumption | 120 kW |
| MT70 Output Capacity | 150–200 kg/hr (basis not stated in source — confirm raw material, moisture content, and target flake specification) |
| MT70 Overall Dimensions | 41 × 1.5 × 2.2 m |
| MT85 Installed Power | 190 kW |
| MT85 Power Consumption | 140 kW |
| MT85 Output Capacity | 300–400 kg/hr (basis not stated in source — confirm raw material, moisture content, and target flake specification) |
| MT85 Overall Dimensions | 43 × 1.5 × 3.2 m |
| MT75 Installed Power | 210 kW |
| MT75 Power Consumption | 150 kW |
| MT75 Output Capacity | 300–500 kg/hr (basis not stated in source — confirm raw material, moisture content, and target flake specification) |
| MT75 Overall Dimensions | 45 × 1.5 × 3.5 m |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Voltage & Frequency | Configurable (commonly 415 V 50/60 Hz, 440 V 50/60 Hz, 220 V 60 Hz) |
| Flaking Drive | Double motors with independent roller drive; hydraulic system; infrared sensor temperature control |
| Roasting Oven | Vibrating pan, high-temperature spraying tubes, dual circulating fans, cyclone dust removal, conciliation burner |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits and corn flour blends |
| Sugar-coated breakfast cereal flakes | Corn, rice, or multi-grain base with sugar syrup coating |
| Multi-grain cereal shapes | Rice, wheat, oat, barley powder blends (ball, tube, stick, ring, fruit loop, star, wheel, flower, heart via die adjustment) |
| Instant porridge and nutritional cereal | Pre-gelatinised grain formulations |
Why "Rated Capacity" on Corn Flake Lines Misses the Real Story
Output means nothing when the flake density, blister pattern, and bowl-life crispness don’t match what your market expects.
I spent years flying out to fix lines that technically ran at their quoted throughput but produced flakes that either sank in milk within seconds or shattered during the coating drum. The problem was almost never the motor size. It was the screw configuration and barrel profile — set up for a generic corn recipe while the buyer was running a multi-grain blend with different starch behaviour. That mismatch only shows up once the line is installed and running your actual material. [NEED_CITE: starch gelatinisation behaviour across different grain blends in twin-screw extrusion]
How Screw Geometry Dictates Flake Texture
The twin-screw configuration in these models allows precise control over shear intensity and residence time inside the barrel. For corn flakes, the degree of starch gelatinisation directly governs whether the final flake achieves the dense, glassy structure needed for crispness after roasting. Corn flakes extrusion production line technology depends on matching screw element arrangement — conveying, kneading, and reverse elements — to the specific grain formulation and moisture level entering the barrel.
Barrel Temperature Profile and Moisture Management
Gelatinisation requires both heat and water. The barrel zones are heated independently, and the temperature gradient across those zones determines how completely the starch granules break down before the material exits the die. Too little gelatinisation leaves a raw centre that won’t crisp properly in the roasting oven. Too much breaks the structure down entirely, producing a flake that turns to mush in the bowl. [NEED_CITE: barrel temperature profiling for starch-based extrusion processes] Getting this right for a corn-only recipe versus an oat-barley blend requires fundamentally different thermal profiles, and that’s where the corn flakes extrusion production line technology must be configured to the buyer’s exact formulation rather than a default setting.
What the Parameter Sheet Actually Tells You
The installed power ratings across the MT70, MT85, and MT75 models reflect different throughput classes, but power alone doesn’t predict product quality. The twin-screw design across all three means each can handle viscous, high-starch doughs that would stall a single-screw extruder. The flaking station uses double motors with independent roller drive, so roller gap and surface speed can be adjusted separately — essential for maintaining uniform flake thickness when switching between natural and sugar-coated production runs. The hydraulic system on the rollers provides consistent pressure even as the rollers heat up and expand during extended runs. Infrared sensor temperature control on the flaking machinery prevents the dough sheet from sticking or tearing at the nip point. The roasting oven’s dual circulating fans and cyclone dust removal system manage the moisture evacuation rate, which governs surface blister formation — those small bubbles on a corn flake’s surface that define its visual identity and crunch character.
The Hidden Cost of Skipping Configuration Work
A line assembled from catalog defaults rather than configured to your grain blend will run. It will produce flakes. But the flakes will lack the density specification your packaging declares, the blister pattern will be inconsistent, and sugar coating will adhere unevenly because the surface porosity is wrong. I’ve seen buyers discover these problems three months after commissioning, when retail buyers start rejecting shipments. Re-configuring screw elements and re-profiling barrel zones after installation costs multiples of what proper specification work would have cost before the machine left the factory. [NEED_CITE: post-installation reconfiguration costs in food extrusion lines]
Why Source the Line from One Supplier
Matching extruder output to flaking capacity to roasting throughput eliminates the bottleneck problem that arises when stations are sourced from separate vendors with incompatible speed ranges. The screw configuration and die design are specified to your raw material and target flake geometry, not copied from a generic build. An in-house testing workshop allows trial runs on your actual grain blend before shipment, so flake density, blister pattern, and crispness are validated against your specification — not discovered for the first time during commissioning. Voltage, frequency, and control language are confirmed before production begins, preventing the delays that occur when a 415 V machine arrives at a 440 V facility. Twin-screw expertise across breakfast cereal applications means the corn flakes extrusion production line technology is applied from experience with real formulations, not adapted from unrelated extrusion processes.
Documentation & Verification
- Line layout and capacity calculation showing throughput balance across extrusion, flaking, drying, and roasting
- Screw and die configuration record documenting exact geometry for your grain blend
- Trial run report on your raw material verifying flake density and blister pattern before dispatch
- Electrical schematic with voltage and frequency confirmed to your facility supply
- Operation and maintenance manual covering roller gap adjustment and barrel zone calibration
- Wear parts list specifying screw elements, die plates, and roller surfaces with replacement intervals
Installation, Commissioning & Support
- Foundation requirements mapped to the MT75’s 45 m line length and 3.5 m headroom clearance
- Dedicated power circuit sized to the selected model’s installed power rating up to 210 kW
- PLC and MCC control interfaces configured to local operator language before arrival
- Flaking station roller alignment and hydraulic pressure calibrated during on-site commissioning
- Roasting oven burner tuning and fan balance verified against target flake moisture content
- Spare screw elements, die plates, and flaking roller sleeves stocked with initial delivery
What to Include in Your Inquiry
To configure the line correctly, share your grain formulation — whether pure corn or a multi-grain blend — along with the target flake thickness and density specification. Confirm your facility voltage, frequency, and preferred control language. If you’re running sugar-coated product, specify the coating ratio and syrup composition so the coating drum and drying stages are sized accordingly.
Frequently Asked Questions
Q: How is screw configuration and die design specified to my grain blend and target flake thickness?
A: The screw element arrangement and die geometry are selected based on your raw material composition, moisture content, and the flake density your market requires. A trial run on your actual grain blend is conducted in the testing workshop before shipment to validate the configuration.
Q: What extrusion parameters control starch gelatinisation degree and final flake density?
A: Barrel temperature profile, moisture addition rate, screw speed, and die geometry collectively govern gelatinisation. Higher gelatinisation yields a denser, crisper flake. These parameters are tuned to your specific formulation during the pre-shipment trial run.
Q: How is throughput matched between extruder, flaking rolls, dryer, and roasting oven to avoid bottlenecks?
A: Each station’s capacity is calculated against the line’s target output so material flow remains continuous. The flaking station’s dual-motor drive and the roasting oven’s dual circulating fans are sized to handle the extruder’s actual discharge rate without accumulation or starvation.
Q: Can a trial run on my raw material be conducted before shipment to validate flake quality?
A: Yes. The in-house testing workshop runs your grain blend through the configured extruder, flaking, and roasting stages. Flake density, blister pattern, and crispness are measured against your specification, and adjustments are made before the line ships.
Q: What voltage, frequency, and control language options are confirmed before commissioning?
A: Voltage and frequency are confirmed to match your facility power supply — commonly 415 V, 440 V, or 220 V at 50 or 60 Hz. Control language for the PLC interface and MCC panels is specified during the quotation stage to avoid delays during on-site commissioning.