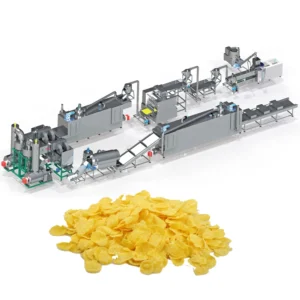
Screw configuration matched to your grain recipe — we trial-run every corn flake line on the buyer’s actual raw material before shipment, validating expansion and density rather than quoting generic throughput.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-75 Twin Screw Extruder |
| Product Type | Corn Flakes Production Line |
| Screw Type | Twin-screw |
| Output Capacity | 200–300 kg/hr (basis not stated in source — confirm raw material, moisture, product format) |
| Line Stations | Mixing — Extruding — Flaking — Drying — Hot Air Roasting — Sugar Spraying — Sugar Coating — Drying — Cooling — Packing |
| Control System | PLC control system (flaking machinery) |
| Voltage & Frequency | 220V / 380V (frequency to be confirmed per destination market) |
| Heating Source (Dryer / Roasting) | Gas or Electric, configurable |
| Flaking Machinery Drive | Double motors for separate roller driving; hydraulic system for double rollers |
| Temperature Control | Infrared sensor for even temperature pipe control (flaking machinery) |
| Hot Air Roasting Oven | Vibrating pan with high-temperature spraying tubes; two separate circulating fans; cyclone dust removal; reconciliation burner in combustion chamber |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Warranty | 1 Year (core component: Gearbox) |
| Machinery Test Report | Provided |
| Video Outgoing Inspection | Provided |
| Certification Standards | CE, ISO (specific certificates confirmed per shipment) |
Application Suitability
| Application | Material or Output |
|---|---|
| Plain corn flakes for breakfast cereal retail | Corn grits or corn flour base |
| Sugar-coated and frosted corn flakes | Corn base with sugar spray and coating stages |
| Multi-grain breakfast cereal flakes | Blends of corn, rice, wheat, oat, barley |
| Extruded puffed snack shapes | Corn, rice, wheat flour via die swap on the same extrusion platform |
What "200–300 kg/hr" Leaves Out About Corn Flake Extrusion
A capacity number means nothing until you know which grain blend, moisture level, and flake density it was measured against.
I learned this the hard way. Years back I helped specify a breakfast cereal line for a Southeast Asian buyer based on a nominal capacity figure. The buyer’s local corn grits had a coarser particle size and different starch behaviour than our test material. Actual throughput fell well short, and the flakes went soggy in milk far too quickly. The corn flakes extrusion technology twin-screw process is unforgiving in this way — screw profile, die geometry, and barrel temperature zones all interact with your specific grain recipe. A generic build copied from a catalogue simply will not deliver [NEED_CITE: how raw material particle size and moisture affect extruder throughput and product texture].
Screw Configuration and Die Geometry Define Flake Density
The twin-screw arrangement gives operators control over shear intensity and residence time across each barrel zone. For corn flakes, the screw elements must generate enough shear to gelatinise starch fully without over-working the dough into a dense mass that refuses to expand at the die face. Die orifice diameter and land length then govern how much the extrudate swells as it exits — a critical factor because the subsequent flaking rollers can only compress the pellet within a narrow thickness window. When corn flakes extrusion technology twin-screw parameters are tuned correctly, the pellet arrives at the flaking station with the right internal porosity for a crisp final product.
Barrel Temperature Profile and Moisture Across Zones
Each barrel section has independent heating and cooling, allowing a staged temperature curve from feed inlet to die plate. Starch gelatinisation in corn typically begins around a specific thermal threshold and must progress steadily as the dough moves through successive zones [NEED_CITE: starch gelatinisation temperature ranges for corn and multi-grain blends]. Moisture injected at controlled points softens the dough just enough to promote expansion without collapsing the cell structure. Too little moisture and the flakes emerge brittle; too much and they turn leathery, losing the bowl-life that breakfast cereal consumers expect.
Reading the Specs That Actually Matter
The MT-75 designation covers the extruder itself, but corn flake quality depends on every station downstream. The hydraulic flaking rollers with double-motor separate drive ensure that both rolls turn at precisely matched speeds, preventing shear tearing on the flake surface. Infrared temperature monitoring on the flaking machinery keeps roll surface heat uniform, which is essential because uneven roll temperature produces flakes that are thick on one edge and paper-thin on the other. The hot air roasting oven uses two independent circulating fans plus a cyclone dust removal device — the dual fans eliminate dead spots inside the chamber, while the cyclone pulls fine particulate out before it can scorch and contaminate the product. Gas or electric heating is selectable at order stage, letting buyers align the roasting energy source with local utility costs.
The Hidden Cost of a Mismatched Line
An extruder sized without matching dryer and roasting capacity creates a bottleneck that surfaces only after commissioning. I have watched producers run the extruder at half speed because the oven could not keep up — effectively paying for capacity they could never use. Voltage and frequency confirmed too late can delay commissioning by weeks while control panels are rewired [NEED_CITE: electrical standard variations across export markets]. Screw and die sets specified for generic corn flour may fail entirely when the buyer switches to a multi-grain recipe with oat or barley, whose lipid content changes dough rheology and demands different compression ratios.
Why Buyers Specify This Line Here
Every station from batching to packing is sourced from a single supplier, so throughput is matched across the extruder, flaking rolls, dryer, roasting oven, and coating drum before the line ships. Screw configuration and die design are specified to the buyer’s actual grain blend and target flake density — not copied from a generic build. Our in-house testing workshop runs the buyer’s own raw material to validate expansion ratio, flake thickness, and roasting profile before any equipment leaves the factory. The PLC control architecture allows recipe storage for different cereal formats, so producers can switch between plain corn flakes, sugar-coated variants, and multi-grain runs with documented parameter sets. Twin-screw expertise extends across pet food, aquatic feed, snacks, and breakfast cereals, meaning the engineering team understands how starch and protein behave under extrusion conditions regardless of the end product.
Documentation & Verification
- Line layout drawing showing station-by-station throughput balance for your target flake output
- Screw and die configuration record matched to your grain recipe and density specification
- Trial run report on your raw material documenting expansion ratio and flake thickness
- Electrical schematic with voltage, frequency, and HMI language confirmed before production
- CE declaration of conformity and ISO certificate included with each shipment
- Wear parts list covering screws, dies, and flaking roller consumables
Installation, Commissioning & Support
- Foundation plan provided matching the full line footprint from mixer to packing station
- Power supply schedule listing circuit requirements for the 380V extruder motor and roasting oven heating elements
- Assembly guidance covering extruder barrel alignment and hydraulic flaking roller calibration on site
- First-run commissioning includes barrel temperature profile tuning and die swap trials for your recipe
- Operator training covers PLC recipe management, screw wear inspection, and flaking roller gap adjustment
- Spare screw elements and die plates shipped with initial order to cover the first replacement cycle
Before You Request a Quote
To configure the line accurately, share your primary grain type and any secondary grains in the recipe, target flake thickness, and the daily output volume you need from the roasting oven onward. Confirm the available voltage and frequency at your facility, along with preferred control language for the PLC interface. If you can send a sample of your raw material, we will run it in the testing workshop and include the trial parameters with the proposal.
Frequently Asked Questions
Q: How do you verify extruder output capacity against my specific grain recipe and moisture content?
A: We run your actual raw material in our testing workshop before shipment. The trial documents extrusion temperature, screw speed, moisture addition rate, expansion ratio, and resulting flake density. Those figures — not a catalogue number — become the capacity baseline quoted in your proposal.
Q: How are screw configuration and die design selected for corn versus multi-grain flake formulations?
A: Corn, rice, wheat, oat, and barley each differ in starch content, lipid level, and particle hardness. We select screw element pitch, kneading block arrangement, and die land length to match those properties, ensuring correct gelatinisation and expansion for each formulation.
Q: What barrel temperature profile and moisture range produce crispy flakes that hold in milk?
A: The barrel zones are staged to bring starch through gelatinisation progressively while moisture is added at controlled points. The exact temperatures and moisture percentages depend on your grain blend and are validated during the pre-shipment trial run, then stored as a recipe in the PLC.
Q: How is flake thickness uniformity maintained across the hydraulic flaking rollers during continuous production?
A: Double motors drive each roller independently at matched speed, while the hydraulic system maintains consistent roll gap pressure. An infrared sensor monitors roll surface temperature in real time, preventing uneven thermal expansion that would cause thickness variation across the flake width.
Q: Can I run a trial with my own raw material in the testing workshop before the line ships?
A: Yes. Sending your raw material allows us to validate screw configuration, die selection, barrel temperatures, flaking gap, and roasting profile. The trial report accompanies the shipment so your team starts production with proven parameters rather than conducting development from scratch after installation.