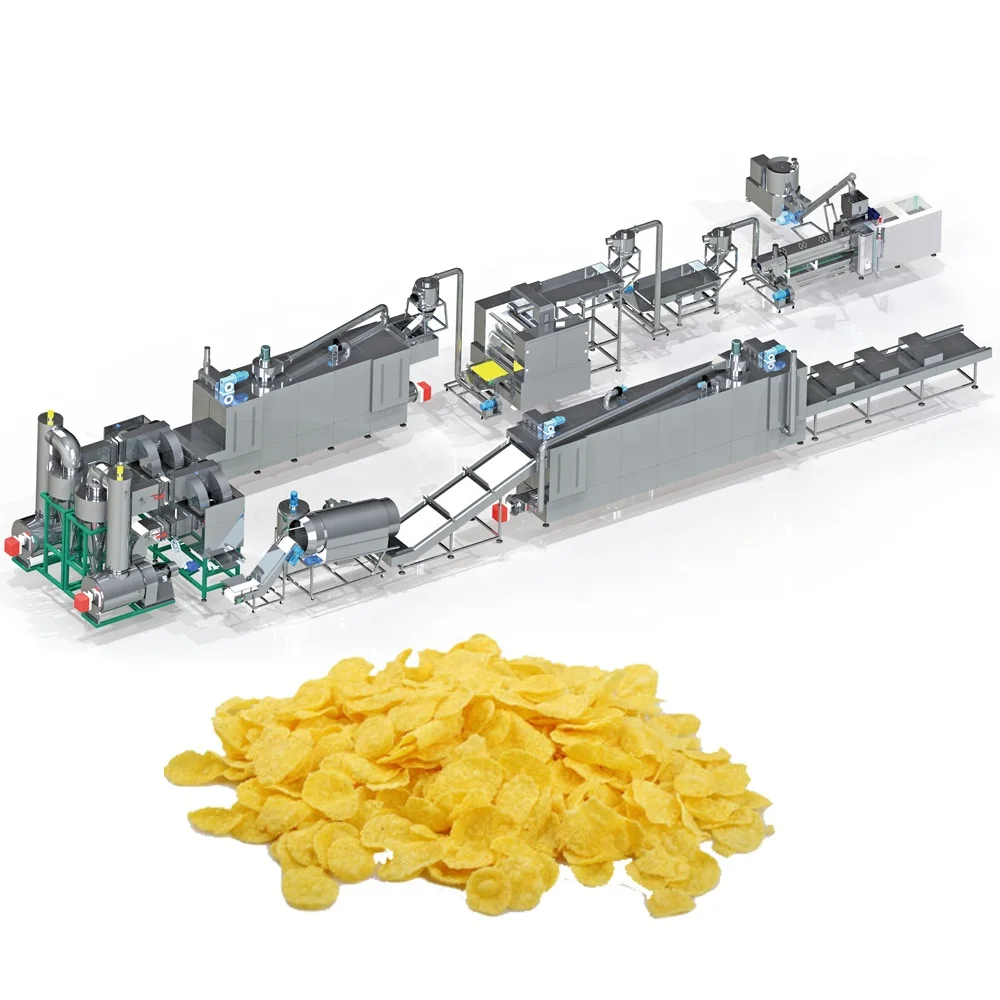
Precision-Engineered Extrusion Parameters — Screw geometry, die aperture and barrel thermal zones configured around your specific corn formulation to deliver consistent flake density and bowl-life.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line / Breakfast Cereal Processing Line |
| Output Capacity | 750 kg/hr (basis not stated in source — confirm raw material type, moisture content, and flake thickness) |
| Target Products | Natural corn flakes, sugar-coated flakes, various shaped breakfast cereals |
| Control System | Easy-to-operate interface (PLC / MCC configuration to be confirmed) |
| Line Configuration | Customizable layout with engineered drawings tailored to factory size |
| Motor Specification | Robust drive system (rated power kW to be confirmed) |
| Electrical Supply | Voltage and frequency configurable to destination market (specify before commissioning) |
| Certification | CE (per company profile, confirm specific directive compliance) |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | De-germed corn grits, whole corn meal |
| Sugar-coated and frosted flakes | Corn base with sugar, malt, honey, vitamin slurries |
| Multi-grain breakfast cereals | Wheat, rice, oat, and barley blends |
| Alternative grain reformulation | Quinoa, sorghum, and gluten-free grain matrices |
| Pilot to full-scale cereal production | Scaling throughput while maintaining target flake density |
When "Rated Capacity" Misses Your Raw Material Reality
A line’s nameplate output means little if the screw and die configuration was never validated against your actual corn grits or grain blend.
I have seen breakfast cereal installations where a corn flakes extrusion production line ran well below its documented throughput simply because the corn flour particle size from a local mill differed from the standard test material. The screw pitch, barrel temperature profile, and moisture conditioning all needed adjustment before the expansion ratio met specification. When extrusion parameters are copied from a generic build, the result is often flakes that either sink in milk or fracture during packaging [NEED_CITE: starch gelatinisation and particle size effects on extrusion].
Barrel Temperature Profiling and Starch Gelatinisation
Achieving the correct gelatinisation degree requires precise thermal control across multiple barrel zones. A corn flakes extrusion production line must manage the transition from raw starch granules to a fully gelatinised dough mass without introducing excessive shear that damages the polymer structure. Each zone’s temperature set-point directly influences the melt viscosity entering the die, which in turn governs how the extrudate expands or densifies during subsequent flaking and drying stages.
Shear, Moisture and the Expansion Window
The balance between mechanical shear from screw rotation and the injected moisture level determines the expansion ratio at the die exit. Too much shear with insufficient moisture creates a brittle extrudate that shatters under the flaking rolls. Too little shear leaves uncooked starch cores that produce hard, unpalatable flakes. The operating window is narrow, and screw element sequencing—conveying, kneading, and reverse-screw sections—must be arranged specifically for your grain formulation [NEED_CITE: twin-screw element configuration for cereal extrusion].
Interpreting the Configuration Against Your Production Targets
The control system interface allows operators to monitor and adjust barrel zone temperatures, screw speed, and feed rate in real time. For a breakfast cereal producer, this level of process visibility is essential when switching between natural corn flake runs and sugar-coated variants, as the sugar slurry coating changes the thermal load on the downstream dryer. The line’s customisable layout ensures that the extruder, flaking rolls, dryer, and coating drum are positioned to maintain a continuous material flow without intermediate bottlenecks. Capacity figures should always be interpreted against the specific grain type, incoming moisture, and target flake thickness you intend to produce.
The Cost of an Unverified Screw and Die Setup
When the screw configuration is not matched to your raw material before shipment, the first weeks of production become an expensive trial-and-error exercise. You consume raw material, energy, and labour while the process team adjusts kneading block angles and die apertures to find a stable operating point. During this period, flake density drifts outside specification, and downstream drying times must be constantly revised. In some cases, entirely new screw elements must be sourced and shipped before the line can hold a consistent output [NEED_CITE: extrusion commissioning delays from incorrect screw configuration].
Engineering the Process Around Your Grain Source
Every corn flakes extrusion production line we configure begins with your raw material sample and your target flake specification. The screw element sequence and die geometry are designed to achieve the gelatinisation degree and expansion behaviour your market expects. Our in-house testing workshop runs your actual corn grits or grain blend before the equipment leaves the factory, producing a trial run report that documents the validated screw configuration and barrel temperature profile. Throughput across the extruder, flaking station, dryer, and coating drum is calculated and matched so that no single station restricts the line. We provide the screw and die configuration record, electrical schematic with your confirmed voltage and frequency, and a complete line layout drawing showing utility connection points and maintenance access clearances.
Documentation & Verification
- Screw and die configuration record matched to your corn grits or grain blend
- Trial run report on your raw material documenting achieved flake density and expansion
- Line layout and capacity calculation with throughput matched across every station
- Barrel zone temperature profile range and L:D ratio on machine specification sheet
- Electrical schematic with confirmed voltage, frequency, and control language
Installation, Commissioning & Support
- Foundation and utility planning based on customised line layout and extruder footprint
- Electrical connection to local voltage and frequency confirmed before dispatch
- Barrel zone thermocouples and heating elements verified during on-site commissioning
- Screw element sequence and die aperture validated with your raw material at start-up
- Operator training on control interface for temperature, screw speed, and feed rate adjustment
- Wear parts list covering screw elements, die inserts, and flaking roll surfaces
What We Need to Specify Your Line
To engineer a corn flakes extrusion production line that performs against your actual production targets, we need your corn or grain type, incoming moisture content, and particle size distribution. Share your target flake thickness, final product density, and the coating formulation if you produce sugar-coated or frosted variants. Your facility’s available floor space, ceiling height, and local electrical supply specifications allow us to deliver a layout that fits without compromise.
Frequently Asked Questions
Q: How is screw configuration and die design matched to a specific corn or grain formulation?
A: We analyse your raw material sample for particle size, starch content, and moisture level, then select conveying, kneading, and reverse-screw elements to achieve the target gelatinisation degree. Die aperture and land length are calculated to produce the expansion ratio your flake specification requires. The configuration is documented and can be replicated for consistent batch-to-batch results.
Q: What barrel temperature profile is needed to achieve target starch gelatinisation without over-shear?
A: The profile typically progresses from moderate heat in the feed zone to peak temperatures in the cooking zones, then cools slightly before the die. Each zone is set based on your grain’s gelatinisation onset temperature and the screw speed in use, ensuring complete starch conversion while preventing mechanical degradation of the starch polymer chains.
Q: How do you verify output capacity on my actual raw material before shipment?
A: Your raw material is run through the extruder in our testing workshop under the configured screw and die setup. We measure throughput, extrudate expansion, moisture loss, and flake density after rolling and drying. The trial run report documents these values so you know the line’s performance before it arrives at your facility.
Q: What moisture and shear parameters control the expansion and density of the final flake?
A: Injected moisture softens starch granules and lowers melt viscosity, while screw kneading blocks provide the shear energy for gelatinisation. Higher moisture with moderate shear typically yields denser, tougher flakes suitable for extended bowl-life. Lower moisture with higher shear produces greater expansion and lighter texture, which may require adjusted drying times downstream.
Q: How is the extruder’s throughput matched to downstream drying and flaking stations to avoid bottlenecking?
A: We calculate the extruder’s mass output at your confirmed screw speed and feed rate, then size the flaking roll width, dryer belt length, and coating drum volume to handle that flow with a margin for product changeover. The line layout shows material transfer points and buffer capacities so that no station restricts overall throughput.