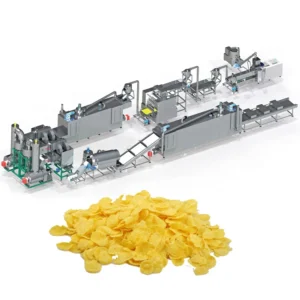
Screw configuration matched to grain — We run your exact corn blend in our testing workshop before shipping the MT-75 Twin Screw Extruder, so screw profile and die geometry are set to your moisture and starch levels, not copied from a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-75 Twin Screw Extruder |
| Product Type | Corn Flakes Production Line |
| Screw Type | Twin-screw |
| Output Capacity | 200-300 kg/hr (basis not stated in source — confirm raw material, moisture content and flake specification) |
| Extruder Control | PLC control system |
| Voltage Options | 220V / 380V (frequency to be confirmed against target market standard) |
| Flaking Roller Drive | Double motors, separate roller driving |
| Flaking Pressure System | Hydraulic system for double rollers |
| Flaking Temperature Control | Infrared sensor |
| Dryer Heating Source | Gas / Electric |
| Hot Air Roasting Oven | Vibrating pan with high temperature spraying tubes, conciliation burner, two separate circulating fans, cyclone dust removal |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Core Components | Gearbox |
| Core Components Warranty | 1 Year |
| Machinery Test Report | Provided |
| Video Outgoing Inspection | Provided |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Plain corn flakes | Corn grits or corn flour |
| Sugar-coated corn flakes | Corn, sugar syrup or honey coating |
| Multi-grain breakfast flakes | Rice, wheat, oat, barley blends |
| Alternative cereal shapes | Grain-based dough with adjusted die and cutting station |
What the Rated Capacity Figure Hides About Corn Flakes Lines
A capacity number without the grain specification and moisture profile behind it is not a capacity number at all.
I spent years on the buyer side sourcing breakfast cereal equipment before moving to the supplier side, and one pattern shows up again and again. A corn flakes extrusion production line arrives at the factory, the nameplate says 300 kg/hr, but the buyer is running degerminated corn with a different starch-to-fibre ratio than the test material. The flakes come out soft, blistering is uneven, and four days of on-site parameter adjustment follow [NEED_CITE: raw material variability in grain extrusion]. The screw configuration that worked on one corn source produces a completely different dough rheology on another. This is why a corn flakes making machine must be specified against the actual raw material the buyer will run, not a benchmark flour the supplier happens to have in stock.
Barrel Temperature Profile and Starch Gelatinisation
A twin-screw extruder processes grain through distinct barrel zones, each contributing a different thermal and mechanical input. For corn flakes, starch must reach full gelatinisation inside the barrel without premature expansion at the die face. The barrel temperature profile on the MT-75 is set after reviewing the buyer’s grain composition and target moisture, so that the dough exits at the right viscosity for downstream flaking. Incorrect zone settings lead to either under-cooked centres or over-expanded material that shatters under the flaking rollers.
Shear, Moisture, and Expansion Control at the Die
The relationship between screw speed, moisture injection, and die geometry determines how much the extrudate expands as it leaves the barrel. In a corn flakes extrusion production line, the goal is minimal expansion — the material should exit as a dense, flat rope that the flaking rollers can press into uniform sheets. The die design on the MT-75 is specified to the buyer’s formulation, controlling back-pressure and exit velocity. Too much shear generates internal steam pockets that cause the flake to blister unevenly during roasting [NEED_CITE: die design principles in food extrusion].
How Flaking and Roasting Hardware Affects Final Texture
The flaking station uses a hydraulic pressure system with independent dual-motor drive to maintain consistent roller gap across the full sheet width. Infrared sensors monitor roller surface temperature so the dough sheet does not stick or tear during pressing. Downstream, the hot air roasting oven uses a vibrating pan with high-temperature spraying tubes and two separate circulating fans to deliver even surface blistering. The cyclone dust removal device captures fine particulate generated during roasting, keeping the oven interior and product surface clean. Together, these stations determine whether the final flake meets the crispness and density that retail and foodservice markets expect.
The Hidden Cost of a Mismatched Dryer or Coating Station
An extruder that outpaces its dryer creates a bottleneck where partially dried flakes pile up, absorbing ambient moisture and losing the texture the roasting oven is meant to set. I have seen lines where the extruder was sized correctly but the dryer and roasting oven were spec’d for a lower throughput, forcing the operator to run the screw at reduced speed. The same applies to sugar coating — if the coating drum volume does not match the roaster output, flakes cool below the syrup adhesion temperature before tumbling is complete [NEED_CITE: throughput matching in food processing lines]. The result is uneven sugar coverage and product that does not meet specification.
Why Sourcing the Full Line from One Supplier Matters
The MT-75 corn flakes extrusion production line is configured from batching through packing under one engineering team, so throughput is balanced at every station rather than assembled from independent vendors. Screw configuration and die design are specified to the buyer’s actual grain blend, not pulled from a standard catalogue. The in-house testing workshop runs the buyer’s raw material before shipment, producing a trial run report that documents screw profile, barrel settings, and flake density. Electrical schematics confirm voltage and frequency for the destination market before the control panel is wired. The PLC system is programmed in the operator’s language, reducing commissioning time on site.
Documentation & Verification
- Line layout and capacity calculation matched to your grain formulation and target flake density
- Screw and die configuration record for your specific corn or multi-grain blend
- Electrical schematic with voltage and frequency confirmed for your facility
- Trial run report on your actual raw material before shipment
- Factory test record covering extruder, flaking, and roasting stations
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Foundation and floor space plan based on the full line layout from mixer to packing station
- Dedicated electrical circuit sized to the MT-75 extruder motor and roasting oven heater load
- Assembly sequence for flaking roller and roasting oven modules delivered in shipping configuration
- First-run parameter tuning on your grain supply with PLC screen calibration
- Operator training covering screw wear inspection and hydraulic roller pressure adjustment
- Wear parts list including spare screws and dies with reorder intervals
What We Need to Configure Your Line
Provide the grain type and particle size you intend to run, along with moisture content at the mixer inlet. Share your target daily output in finished flake weight and whether the line will produce plain, sugar-coated, or both formats. Confirm the voltage and frequency at your facility and the control language your operators require.
Frequently Asked Questions
Q: How is screw configuration and die design specified to a particular grain blend?
A: We review the buyer’s grain certificate of analysis — protein, starch, fibre, and moisture — then select screw element spacing and die orifice diameter accordingly. A trial run on the buyer’s actual raw material in our testing workshop confirms the configuration before shipment. The resulting screw and die record ships with the line.
Q: How is flake density controlled through the barrel temperature profile?
A: Each barrel zone contributes heat and shear to the dough. By adjusting zone temperatures and screw speed, we control the degree of starch gelatinisation and the amount of steam generated before the die. Less expansion at the die face produces a denser rope, which the flaking rollers then press to the target thickness.
Q: What raw material preparation is needed before the extruder?
A: Grain must be milled to a consistent particle size and conditioned to a target moisture level at the mixing station. The batching system on the MT-75 line meters grain, water, and any minor ingredients so the extruder receives a uniform feed. Inconsistent particle size leads to uneven gelatinisation.
Q: How are dryer and roasting oven capacities matched to extruder throughput?
A: We calculate the moisture removal load from the extruder output and specify dryer belt length and roasting oven volume to handle that load continuously. The line layout document shows throughput at each station so no single unit becomes a bottleneck during steady-state production.
Q: What does the pre-shipment trial run report cover?
A: The report documents screw configuration, barrel temperature settings, moisture addition rate, flake thickness after the rollers, roasting temperature and time, and final flake density and crispness measurements. It is generated using the buyer’s own raw material and shared before the line is crated for dispatch.