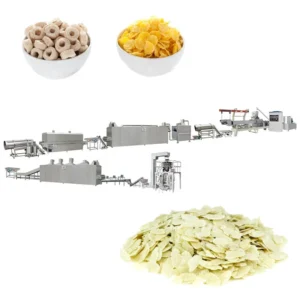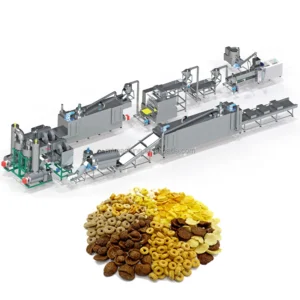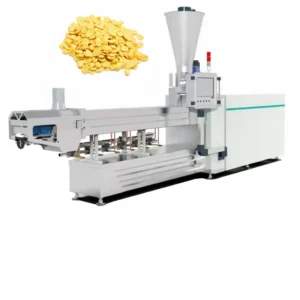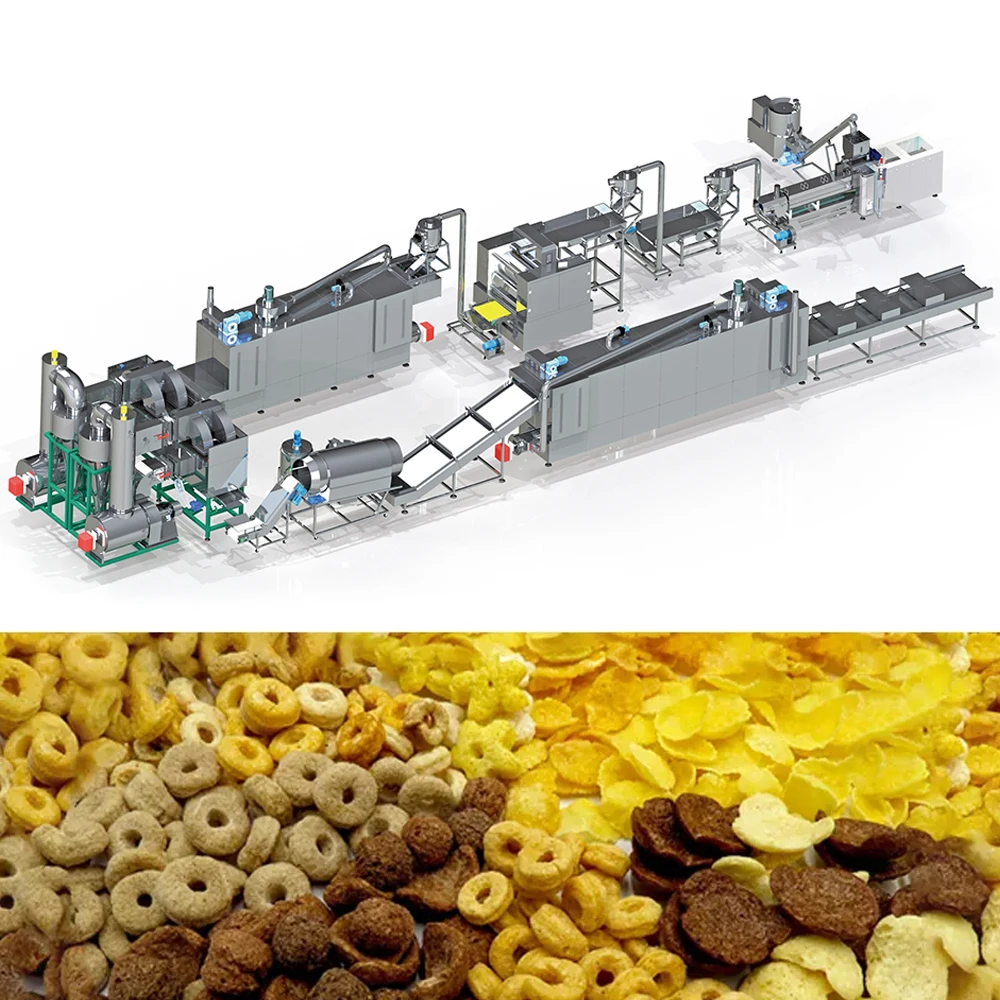
Screw Geometry Tuned to Your Grain — MT75 barrel sections and die apertures are matched to your specific corn, wheat, or multi-grain formulation before build, so gelatinisation and expansion align with the flake density your market expects.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Twin Screw Extruder for Breakfast Cereals and Corn Flakes Processing Line |
| Screw Type | Twin screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/h (basis not stated in source — confirm raw material type, moisture content and product format) |
| Overall Dimensions (Line) | 45 × 1.5 × 3.5 m |
| Control System | PLC and MCC control; infrared sensor temperature control on flaking rollers |
| Flaking Machinery | Hydraulic double-roller system with double motors for separate roller driving |
| Dryer Heating Source | Gas or electric |
| Roasting Oven | Hot air roasting with vibrating pan, high-temperature spraying tubes, conciliation burner, two separate circulating fans and cyclone dust removal |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Voltage & Frequency | Customized to buyer’s requirement (commonly 415V 50/60Hz, 440V 50/60Hz, 220V 60Hz) |
| Screw Material | Wear-resistant alloy (exact grade to be confirmed) |
| Lubrication | Automatic lubricating and cooling function |
| Line Stations | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Sugar Spraying / Coating (optional) → Drying → Cooling → Packing |
| Standards | CE (since 2014); ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal market | Corn grits and corn flour |
| Sugar-coated corn flakes | Corn base with sugar syrup coating |
| Multi-grain breakfast cereals | Wheat, oat, barley, and rice powder blends |
| Shaped cereal formats (rings, balls, fruit loops, stars) | Corn and grain blends with die adjustments |
| Instant breakfast cereal processing | Grain powder formulations for food manufacturers expanding cereal production |
What "300–500 kg/h" Actually Depends On
Extruder throughput on cereal lines is a function of raw material moisture, particle size, and screw speed — not a nameplate promise.
I have watched a breakfast cereal line stall at half its quoted output because the buyer’s corn grits carried two percentage points more moisture than the supplier assumed, and the screw configuration was never adjusted for it. The twin screw extrusion technology breakfast cereals corn flakes processors rely on must be validated against the grain you will actually run. A capacity figure without a stated moisture range, particle size distribution, and target flake density is a number waiting to disappoint [NEED_CITE: typical moisture variance in milled corn grits across harvest seasons].
Barrel Zone Profiling for Starch Gelatinisation
Corn starch gelatinises within a narrow temperature window, and the barrel must deliver that heat progressively. The MT75 barrel is segmented into multiple heating and cooling zones, each independently controlled through the PLC. Early zones hydrate the grain mix gently, while mid-barrel zones raise temperature into the gelatinisation range under shear from the twin-screw elements. Getting this profile wrong means either under-cooked dough that tears at the flaking rollers or over-cooked mass that exits the die too stiff to expand.
Die Aperture and Flake Density Control
The die plate is where extrusion geometry meets your target product specification. Aperture diameter, land length, and face pattern determine how much the dough expands before it hits the flaking rollers. For a thin, crisp corn flake that holds bowl-life, the die must produce a rope with the right internal void structure. Twin screw extrusion technology breakfast cereals corn flakes producers need dies matched not to a generic catalogue shape, but to the exact bulk density and thickness their packaging line and market expect [NEED_CITE: relationship between die land length and extrudate expansion ratio in cereal processing].
Reading the Specs That Matter
The MT75 draws 210 kW installed and consumes approximately 150 kW during steady-state operation — that gap accounts for motor start-up surge and heater cycling across the barrel zones. The hydraulic double-roller flaking system with separate motor drives allows independent speed adjustment on each roller, which directly affects flake thickness uniformity across the web. Infrared sensors on the rollers close the temperature loop, preventing the surface chilling that causes flake cracking downstream. The 45-metre line footprint includes every station from batching through packing, so throughput is balanced across mixing cycles, extruder output, dryer residence time, and roasting oven capacity rather than assembled from mismatched standalone units. The PLC records process parameters per batch, giving you traceability on every run.
The Cost of Skipping the Trial Run
When a cereal line ships without a test run on the buyer’s actual grain, the first weeks of production become an expensive experiment. Screw elements get swapped, barrel temperatures drift outside safe gelatinisation ranges, and flaking rollers produce flakes that shatter or clump. Operators burn through raw material chasing a stable process window, and the roasting oven cannot compensate for extrusion errors upstream. Every hour of unplanned troubleshooting is an hour of lost saleable output, and the market does not wait for your line to stabilise [NEED_CITE: cost of unplanned downtime in continuous food processing operations].
Why Procure This Line Here
The screw configuration and die design are specified to your raw material formulation and target flake density before the build begins, not copied from a generic reference build. An in-house testing workshop runs your actual corn, wheat, or multi-grain blend through the extruder before shipment, producing a trial run report that documents the process window. The complete line from batching to packing is supplied under one responsibility, so dryer capacity, roasting oven throughput, and coating drum volume are matched to extruder output rather than sourced separately. Voltage, frequency, and control language are confirmed against your facility specifications before production starts. CE and ISO documentation is provided as standard, and the screw and die configuration record travels with the machine for future reference and replication.
Documentation & Verification
- Line layout and capacity calculation matched to your grain formulation and target output
- Screw and die configuration record documenting element arrangement and die aperture for your product
- Trial run report on your actual raw material conducted in the testing workshop before shipment
- Electrical schematic with voltage and frequency confirmation for your facility’s power supply
- Operation and maintenance manual with wear parts list specific to the MT75 configuration
- CE declaration of conformity and ISO certificate included with shipment documentation
Installation, Commissioning & Support
- 45-metre line footprint requires level concrete floor with utility trenches for gas or electric dryer supply
- 210 kW installed load needs dedicated circuit with correct voltage and frequency confirmed before energisation
- PLC and MCC panels arrive pre-wired; commissioning includes I/O checks and control language verification
- First production run supervised on-site with process parameters recorded for your standard operating procedure
- Operator training covers screw element inspection, die changeover, and flaking roller gap adjustment
- Wear parts list with reorder codes for screws, dies, and roller surfaces provided at handover
Before You Request a Quote
Provide the grain type or blend you intend to run, including particle size distribution and typical moisture content. Specify your target flake thickness, bulk density, and whether the end product is natural or sugar-coated. Confirm your facility voltage, frequency, and preferred control language so electrical and PLC configuration are locked before production. If you have existing upstream milling or downstream packing equipment, share the interface requirements so the line layout accounts for connection points.
Frequently Asked Questions
Q: How is screw configuration determined for different cereal raw materials such as corn versus wheat?
A: Corn, wheat, oat, and barley each have different starch composition, protein content, and fibre levels that affect how they behave under shear and heat. The screw element sequence — conveying, kneading, and reverse elements — is arranged to match the gelatinisation temperature and residence time your specific grain requires. This configuration is documented in the screw record that ships with the machine.
Q: What barrel temperature profile and moisture range are needed for proper starch gelatinisation in corn flakes?
A: Corn starch typically gelatinises between specific temperature thresholds depending on moisture presence. The MT75 barrel zones are set to progressively raise temperature through the hydration, gelatinisation, and metering stages. Moisture content at the feed point must fall within a range validated during the pre-shipment trial run on your actual grain, and that range is recorded in the trial report.
Q: How do you verify extrusion density and expansion before the line ships?
A: Your raw material is run through the MT75 in the testing workshop before dispatch. The trial produces actual flakes that are measured for thickness, bulk density, and bowl-life behaviour. Results are documented in a trial run report so you can confirm the line meets your product specification before it leaves the factory.
Q: Can the die be changed to produce different cereal shapes on the same extruder?
A: Yes. The die plate is interchangeable, and different apertures produce rings, balls, tubes, stars, and other formats. Each shape requires a specific die and may need adjustments to screw configuration and moisture profile. The changeover procedure and compatible die catalogue are covered during operator training at commissioning.