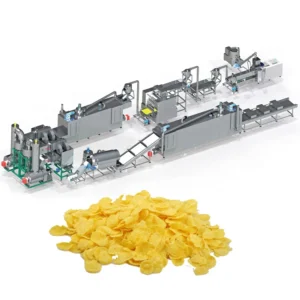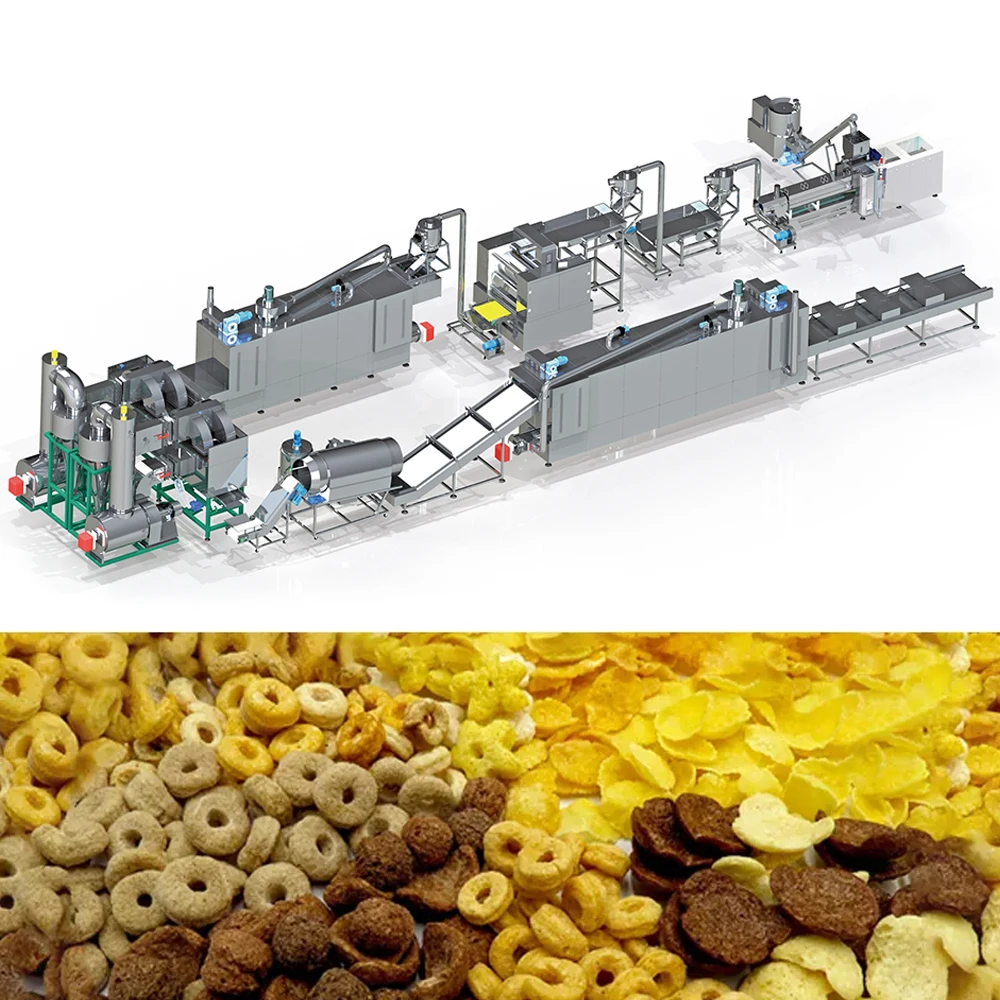
Engineered screw profiles — Every corn flakes extrusion line screw configuration is matched to the buyer’s actual raw material and validated through in-house trial runs before the machine leaves our Jinan workshop.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Production Line |
| Screw Type | Twin Screw |
| Installed Power | MT70 160 kW; MT85 190 kW; MT75 210 kW |
| Power Consumption | MT70 120 kW; MT85 140 kW; MT75 150 kW |
| Capacity | MT70 150–200 kg/h (basis not stated in source); MT85 300–400 kg/h (basis not stated in source); MT75 300–500 kg/h (basis not stated in source) |
| Overall Dimensions (L×W×H) | MT70 41×1.5×2.2 m; MT85 43×1.5×3.2 m; MT75 45×1.5×3.5 m |
| Control System | PLC |
| Flaking Machine Drive | Double motors, separate roller driving |
| Flaking Pressure Control | Hydraulic system for double rollers |
| Flaking Temperature Control | Infrared sensor |
| Dryer Heating Source | Gas / Electric |
| Roasting Oven | Hot air roasting with vibrating pan, dual circulating fans, cyclone dust removal, conciliation burner |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Line Stations | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Cooling → Packing |
| Automation | Automatic lubricating and cooling function |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Final Product Shapes | Natural corn flakes, coated corn flakes, ball, tube, stick, ring, fruit loop, star, wheel, flower, heart |
| Voltage Options | 415V 50/60Hz; 440V 50/60Hz; 220V 60Hz (customizable) |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal brands | Whole corn grits or de-germed corn flour |
| Sugar-coated and honey-glazed corn flakes | Corn, rice, or multi-grain base with sugar or syrup coating |
| Multi-grain flake formats | Wheat, oat, barley blends with corn |
| Shaped cereal snacks (rings, balls, loops) | Corn, rice, or oat flour via die and mould adjustments |
What "300 kg/h" Actually Means for Corn Flake Extrusion
Nominal capacity means nothing if the screw profile cannot handle your specific corn variety and moisture level.
I once had a breakfast cereal customer who ordered a line rated for a given throughput on whole corn flour. When production started with de-germed corn powder, the viscosity and starch gelatinisation behaviour were completely different. The extruded sheet came out thick and dense, and the flaking rollers could not press it into anything resembling a crisp flake. Two days of re-configuring the screw elements and adjusting feed moisture inside the workshop followed before we reached the target expansion and flake geometry [NEED_CITE: starch gelatinisation behaviour differences between whole and de-germed corn flour]. That is why every corn flakes extrusion line screw configuration we ship is first tested on the buyer’s own raw material.
Barrel Temperature Zones and Starch Gelatinisation Control
The MT70, MT85, and MT75 extruders use a multi-zone barrel with PLC-controlled heating and cooling. Each zone is set to a specific temperature to manage the rate of starch gelatinisation as the corn dough travels through the barrel. Too much heat too early causes premature expansion inside the barrel; too little leaves uncooked starch that produces a gritty, under-processed flake. The corn flakes extrusion line screw configuration determines how long the material stays in each zone and how much mechanical shear it receives, directly controlling the degree of cook.
Screw Element Arrangement and Shear Profile
Twin-screw geometry on these models is not a fixed catalogue build. The screw elements — conveying sections, kneading blocks, and reverse-flight segments — are arranged based on the fat content, particle size, and moisture of the incoming corn or multi-grain blend. A high-fat formulation requires a different kneading block sequence than a lean corn grit to achieve the same dough consistency at the die face. Getting this wrong shows up immediately as uneven flake thickness after the hydraulic rollers [NEED_CITE: twin-screw element arrangement principles for high-starch food extrusion].
Specifying the Flaking and Roasting Stations
The hydraulic double-roller flaking machine uses an infrared sensor to monitor roller surface temperature in real time. This matters because corn dough sheets that enter the nip too hot stick to the rollers and tear, while sheets that enter too cold crack instead of flattening. Downstream, the hot air roasting oven runs two independent circulating fans with a cyclone dust removal device. Separate fan circuits allow the operator to control the top and bottom heat balance, which governs how the flake surface blisters and how much moisture is driven off during the final roast.
Reading the Power and Dimension Data Correctly
The installed power figures — 160 kW on the MT70 up to 210 kW on the MT75 — reflect the total connected load across all motors, heaters, and control panels. Actual consumption runs lower, between 120 kW and 150 kW, because heaters cycle and the extruder main motor rarely runs at full amperage once the barrel reaches steady-state temperature. The overall line length stretches from 41 m to 45 m depending on model, which includes every station from the mixer to the packing conveyor. Buyers need to confirm ceiling height as well, since the MT75 stands at 3.5 m at its tallest point, typically the dryer or roasting oven exhaust duct.
When a Generic Build Becomes a Production Problem
A copied screw-and-die setup might produce acceptable flakes on one corn source and fail entirely on another. The symptom is rarely dramatic — it is usually a gradual drift in flake density, a slightly higher breakage rate at the packing station, or a bowl-life that falls short of what the brand promised. By the time the buyer notices, several tons of off-spec product have already run through the line [NEED_CITE: effect of die geometry on cereal flake density and bowl-life]. Matching the corn flakes extrusion line screw configuration to the raw material up front avoids that slow bleed.
Why Purchase This Line From Meiteng
Every station on this corn flakes line — mixing, extruding, flaking, drying, roasting, cooling, and optional sugar coating — is sized and supplied by one builder, so throughput is balanced rather than assembled from mismatched vendors. The screw profile and die geometry are specified against the buyer’s own raw material and target flake density, not pulled from a generic library. Before shipment, the complete line runs a trial in our in-house testing workshop on the customer’s actual corn or grain blend, producing real flakes that can be measured for thickness, density, and bowl-life. Electrical schematics are reviewed and voltage is confirmed against the buyer’s facility before production begins, preventing the commissioning delays that happen when a 415V machine arrives at a 440V plant. Pre-sales engineering, on-site installation, commissioning, operator training, and ongoing wear-part supply are all handled by the same team that built the line.
Documentation & Verification
- Line layout and capacity calculation matched to your corn variety and target flake output
- Screw and die configuration record documenting element arrangement for your raw material
- Trial run report on your actual corn or grain blend before shipment
- Electrical schematic with voltage and frequency confirmed to your facility specification
- CE declaration of conformity and ISO certificate included with every line
- Operation and maintenance manual with wear parts list in your preferred language
Installation, Commissioning & Support
- Foundation plan provided for the full 41–45 m line length, including anchor bolt layout for extruder and flaking stations
- Dedicated power circuit sizing based on confirmed voltage (415V, 440V, or 220V) and total connected load up to 210 kW
- PLC and HMI configured to operator language before dispatch to reduce commissioning time on site
- First-run parameter setting covers barrel zone temperatures, screw speed, feed moisture, and hydraulic roller pressure
- Wear parts list with screw elements, die plates, and flaking roller surfaces identified for initial spare stock
- Routine lubrication and cooling system maintenance intervals documented in the operation manual
Planning Your Line Inquiry
To configure a corn flakes extrusion line screw configuration that actually matches your production needs, share the following with your inquiry. Provide the specific corn or grain type — whole grits, de-germed flour, or a multi-grain blend — along with a representative sample for trial runs. Confirm your target daily output in kilograms of finished flake, your available workshop length and ceiling height, and the local voltage and frequency at your facility.
Frequently Asked Questions
Q: How is the screw configuration matched to my raw material?
A: We run your actual corn or grain sample in our testing workshop, adjusting screw element arrangement, kneading block sequence, and barrel zone temperatures until the extrudate reaches the target expansion and dough consistency for flaking. The final configuration is recorded and shipped with the machine.
Q: What trial runs are performed before shipment?
A: A full trial on your raw material is conducted in our in-house testing workshop. The extruder, flaking rollers, and dryer are operated together to produce sample flakes that are measured for thickness, density, and moisture before the line is packed for dispatch.
Q: How do barrel temperature zones affect the final flake?
A: Each barrel zone controls a specific stage of starch gelatinisation. The PLC maintains independent set points so the corn dough reaches the correct cook level at the die. Incorrect profiling leads to under-cooked grit or premature expansion, both of which ruin flake texture.
Q: How is throughput balanced across the whole line?
A: Every station — extruder, flaking machine, dryer, roasting oven, and coating drum — is selected and sized so that none becomes a bottleneck. The line layout and capacity calculation document this balance before production starts.
Q: What electrical details are confirmed before production?
A: Voltage, frequency, plug type, and control language are confirmed against your facility specification. An electrical schematic is provided for review, and the PLC and HMI are configured to your requirements before the machine is built.