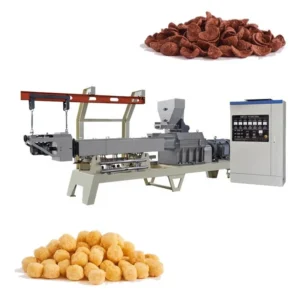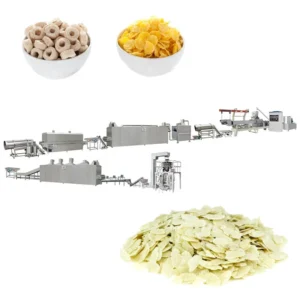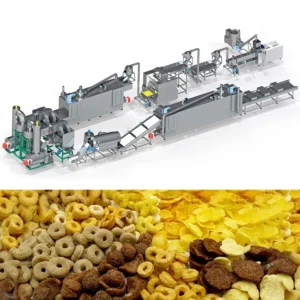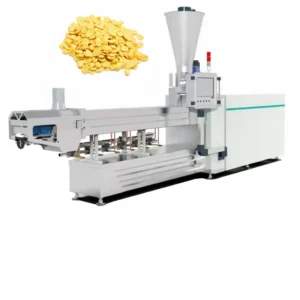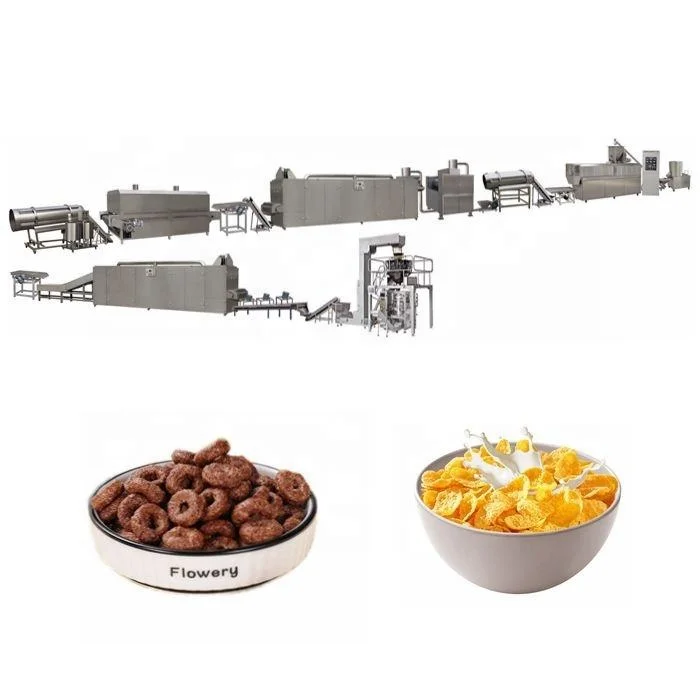
Matched Throughput Across Stations — The MT75 line is built so extruder output, flaker pressure, and roaster heat profile align to your grain blend rather than forcing you to accept mismatched vendor specs.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Twin Screw Corn Flakes Extrusion Line |
| Screw Type | Twin-screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300-500 kg/h (basis not stated in source — confirm raw material / moisture content) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC for flaking machinery; MCC available for line |
| Flaking Machinery Drive | Double motors for separate roller driving; hydraulic system for double rollers |
| Temperature Control (Flaking) | Infrared sensor for even pipe temperature |
| Heating Source (Dryer) | Gas / Electric |
| Roasting Oven | Hot air with conciliation burner, two circulating fans, cyclone dust removal, vibrating pan with high-temperature spraying tubes |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Lubrication | Automatic lubricating and cooling function on extruder |
| Shape Capability | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | Corn, rice, wheat, oat, barley powder |
| Sugar-coated breakfast cereals | Corn flour blends with sugar glazing |
| Multi-grain flake formats | Blended oat, wheat, and barley formulations |
| Fortified cereal projects | Vitamin-mineral premix added at batching stage |
Why Generic Screw Builds Ruin Flake Density
Corn flakes live or die by the expansion that happens inside the barrel, and that expansion depends entirely on how well the screw profile matches your flour blend.
I once watched a Middle Eastern buyer lose an entire batch of corn flakes because the line was shipped with a screw combination copied from a standard snack build. The flakes came out dense, hard in the bowl, and with almost no surface blister. The problem was not the machine — it was that nobody asked what his corn grits looked like or what moisture content his dryer could hold [NEED_CITE: corn gelatinisation thresholds for extrusion processing]. When corn flakes extrusion line technology is treated as a catalogue order instead of a material-specific process, the result is product that the market rejects on the first spoonful.
Barrel Zones and Starch Gelatinisation
Twin-screw extrusion cooks the cereal dough through shear and heat across multiple barrel zones. The corn flakes extrusion line technology in the MT75 uses a screw configuration that is specified after reviewing the buyer’s raw material sample, not pulled from a generic template. Each barrel zone is set to a target temperature so that starch gelatinisation completes before the dough reaches the die face. If the corn blend has higher fibre or protein, the residence time and shear profile must shift accordingly.
Die Design and Flake Expansion Control
The die opening determines how much the dough expands as it exits the barrel and pressure drops to atmospheric. For natural corn flakes, the goal is a flat, dense pellet that will later be flattened by the flaking rollers and blistered in the roasting oven. A die that is too wide produces a pellet that cracks during flaking; one that is too narrow gives a pellet that is too hard to flatten evenly [NEED_CITE: die geometry effects on extruded cereal pellet integrity]. The MT75 die is matched to the target flake thickness the buyer specifies.
Flaking Roller Pressure and Surface Uniformity
After extrusion, the pellets pass through a hydraulic flaking station with double-motor separate roller drive. The hydraulic system holds consistent gap pressure so every pellet is flattened to the same thickness. Infrared sensors monitor roller surface temperature in real time. Uneven thickness means some flakes over-roast while others stay soft inside, and the consumer notices immediately when half the bowl is crunchy and half is chewy.
What Happens When Process Parameters Are Ignored
When the extruder is shipped with an unverified screw build, the pellets may exit the die under-cooked, meaning starch has not fully gelatinised. These pellets shatter under the flaking rollers instead of flattening, producing dust and broken pieces that the roasting oven cannot salvage. Alternatively, over-cooked pellets emerge too expanded and too soft, collapsing into thin flakes that burn before achieving the target crunch. Both outcomes waste raw material and force the buyer to restart product development from scratch [NEED_CITE: troubleshooting extruded cereal flake breakage and density defects].
Why Procurement Should Start With Your Raw Material
The MT75 line is configured only after a trial run on the buyer’s actual corn or multi-grain flour in our testing workshop. The screw and die configuration record documents the exact build, and the trial run report confirms flake density and blister pattern before the machine ships. The PLC-controlled flaking station and MCC line management keep every process parameter logged and repeatable across production runs. Hot-air roasting with a conciliation burner and dual circulating fans gives precise surface blistering. The line layout and capacity calculation match throughput from extruder through flaker, dryer, and roaster so no single station bottlenecks the rest.
Documentation & Verification
- Screw and die configuration record matched to your cereal flour blend
- Trial run report on your raw material confirming flake density and blister pattern
- Electrical schematic with voltage and frequency confirmed to your site conditions
- Line layout showing throughput balance across extruder, flaker, dryer, and roaster
- CE declaration of conformity and ISO certificate for export compliance
Installation, Commissioning & Support
- Foundation plan sized to the 45 m line length with utility trench locations
- Power supply matched to the 210 kW installed load with dedicated breaker sizing
- Assembly of flaking station with hydraulic system calibration on your shop floor
- PLC programming and MCC wiring verified against your local voltage and frequency
- Operator training on screw changeover, roller gap adjustment, and roasting oven profile
- Wear parts list covering screws, dies, and flaking roller surfaces with reorder lead times
Before You Request a Quote
Tell us your cereal formulation — corn, oat, wheat, or a multi-grain blend — along with the moisture content of your flour at the batching stage. Confirm your target daily output and the shift pattern your facility runs. Share your local voltage and frequency, the control language your operators need, and whether you want a trial run on your material before the line ships.
Frequently Asked Questions
Q: How is screw and die configuration matched to my specific cereal flour blend?
A: We run a trial on your actual raw material in our testing workshop before shipment. The screw elements and die opening are selected based on your flour composition, moisture level, and target flake density. A configuration record documenting the exact build ships with the line so you can replicate results on every production run.
Q: What barrel temperature profile produces correct flake expansion?
A: Barrel zones are set to achieve full starch gelatinisation before the dough reaches the die. For natural corn flakes the profile keeps expansion low so the pellet stays dense enough for flaking. For sugar-coated output the profile may shift slightly to alter surface texture for better glaze adhesion. Exact zone settings are confirmed during the trial run.
Q: Can the line handle oat, wheat, or multi-grain formulations?
A: Yes. The twin-screw design allows screw element changes to accommodate different grain blends. Oat and wheat have different starch and fibre profiles than corn, so the screw combination and barrel temperature settings are adjusted accordingly. Each new formulation is validated in the testing workshop before production parameters are locked in.
Q: How do I verify flaking roller pressure before shipment?
A: During the factory trial run, the hydraulic flaking system is tested on pellets made from your raw material. Roller gap, pressure, and infrared temperature readings are logged. The trial run report includes flake thickness measurements and photographs so you can confirm uniformity before the line leaves our workshop.
Q: What process data is logged during the factory trial run?
A: We record barrel zone temperatures, screw speed, moisture content at the mixer, roller gap and pressure at the flaking station, roasting oven temperature, and final flake density. All data is included in the trial run report along with the screw and die configuration record for your reference during commissioning.