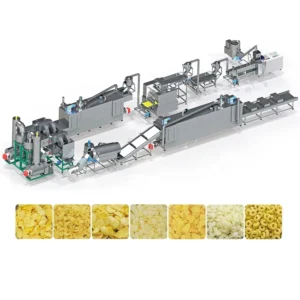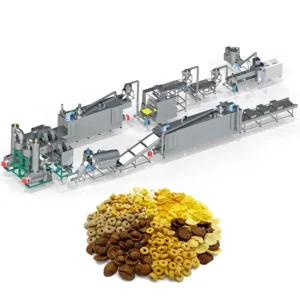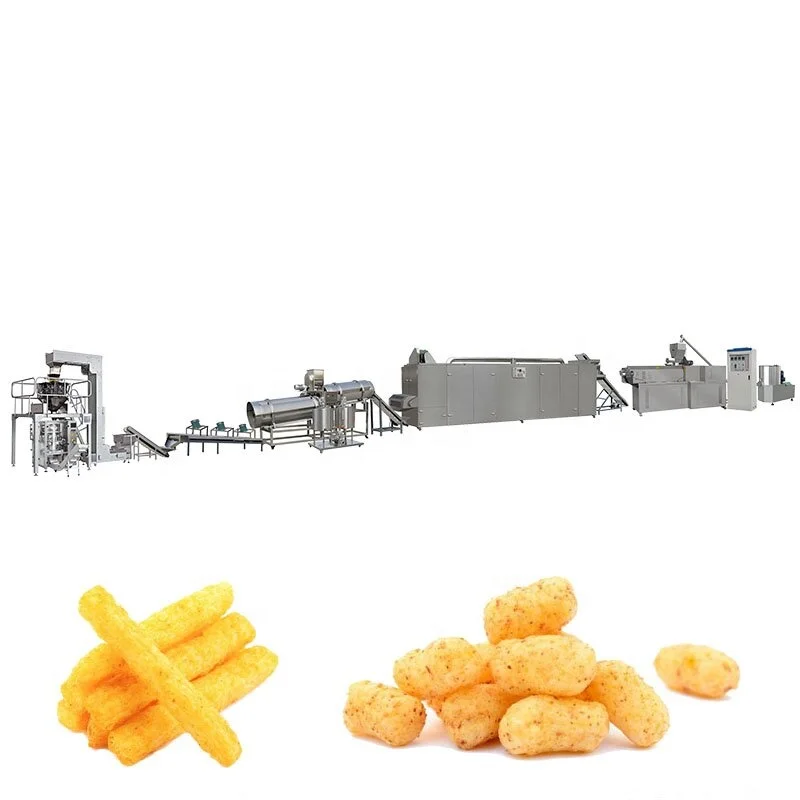
Line Throughput Matched Across Every Station — the batching, extruding, flaking, drying and packing segments on this corn flakes extruder production line are sized together, so one segment does not bottleneck another when running your actual grain blend.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 |
| Product Type | Corn Flakes Extruder Production Line |
| Extruder Type | Twin Screw |
| Installed Power | 160 kW (MT70) |
| Power Consumption | 120 kW (MT70) |
| Output Capacity | 150–200 kg/h (MT70, basis not stated in source — confirm raw material and moisture content) |
| Overall Dimensions | 41 × 1.5 × 2.2 m (MT70) |
| Control System | PLC and MCC available |
| Heating Source (Dryer) | Gas or Electric |
| Flaking Machinery | Hydraulic double-roller system, separate motor drive per roller, infrared temperature sensing |
| Hot Air Roasting Oven | Vibrating pan, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Basic Material Compatibility | Corn, rice, wheat, oat, barley powder |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits or corn flour at controlled moisture |
| Sugar-coated corn flakes | Corn base with sugar syrup coating stage |
| Multi-grain breakfast cereals | Blends of rice, wheat, oat and barley flour |
| Shaped cereal snacks | Ball, tube, ring, star, wheel and heart profiles via die change |
What "Rated Capacity" Actually Means on a Corn Flake Line
Output figures only matter when tied to the exact grain blend, particle size and moisture you plan to run.
I spent two days in a customer’s plant recalibrating a corn flakes extruder production line after their corn flour arrived at double the particle size we used during trial runs. The flakes came out uneven in thickness and hardened after roasting — an entire batch scrapped. Nominal capacity printed on a quotation tells you nothing about how the machine behaves on your material [NEED_CITE: material particle size influence on extrusion throughput]. When the screw configuration and die geometry are not matched to your specific flour blend, the line may physically run but produce flakes that fall outside the density and texture your market expects.
Barrel Temperature Zones and Starch Gelatinisation
Twin-screw extrusion for corn flakes depends on a precise barrel temperature profile across multiple heating zones. Each zone controls how quickly starch granules absorb moisture and gelatinise inside the barrel. Too much heat too early causes premature expansion; too little leaves raw starch that produces a dense, hard flake after roasting. The corn flakes extruder production line extrusion technology used here manages these zones independently through the PLC system, allowing operators to adjust the profile when switching between corn, rice or oat-based formulations.
Moisture Input, Shear Force and Expansion Control
Water injection rate and screw speed together determine the shear force applied to the grain matrix. Higher shear with controlled moisture produces a uniform gel that expands predictably when it exits the die. The screw configuration — the arrangement of conveying, kneading and reverse elements — is selected based on the buyer’s raw material and target flake density. This is where generic builds fail: a screw stack designed for high-expansion puffed snacks will produce the wrong texture when used for corn flakes that need a dense, crisp bite [NEED_CITE: twin-screw extrusion screw element configuration for breakfast cereals].
Reading the Specification Sheet Beyond the Headline Numbers
The installed power of 160 kW on the MT70 drives the main extruder motor, but actual power consumption sits around 120 kW during steady-state operation — the difference matters for your electrical infrastructure planning. The flaking machinery uses a hydraulic double-roller system with separate motors per roller, which allows independent speed adjustment to control flake thickness. Infrared sensors monitor roller surface temperature to prevent sticking and ensure even pressing. The hot air roasting oven relies on a conciliation burner with dual circulating fans, and the cyclone dust removal device captures fine particulate before it can settle back onto the flakes. These details determine whether your line produces consistent surface bubbling and crispness or generates scorched edges and uneven colour.
The Cost of Skipping a Trial Run
Lines shipped without a trial run on the buyer’s actual raw material arrive at the factory as untested assemblies. Commissioning then becomes product development — engineers adjusting screw combinations, moisture rates and temperature profiles on your floor while production schedules slip. I have watched operators cycle through multiple screw configurations over several days before finding a stable setting, generating waste material and delaying market launch [NEED_CITE: pre-shipment trial run benefits for food extrusion equipment]. When floating feed sinks or kibble density misses the specification, the root cause is almost always a configuration copied from a generic build rather than matched to the buyer’s material.
Why This Line Is Configured Differently
Complete line throughput is matched from batching through extrusion, flaking, drying, roasting and packing under one supplier, so no single station creates a bottleneck. Screw configuration and die design are specified to the buyer’s grain blend and target flake density, not pulled from a standard library. The in-house testing workshop runs trial production on your actual raw material before the line ships, generating a documented test report. Twin-screw expertise covers corn, rice, wheat, oat and barley formulations across both natural and sugar-coated variants. Pre-sales engineering includes line layout design matched to your factory footprint, followed by on-site installation, commissioning and operator training.
Documentation & Verification
- Line layout and capacity calculation matched to your grain blend and target output
- Screw and die configuration record documenting the element stack selected for your material
- Trial run report from in-house testing on your raw material before shipment
- Electrical schematic with voltage and frequency confirmed for your local grid
- CE declaration of conformity and ISO certificate included with shipping documentation
Installation, Commissioning & Support
- Foundation and floor space planning based on the 41 × 1.5 × 2.2 m MT70 line footprint
- Dedicated electrical circuit sized for 160 kW installed power with confirmed local voltage
- Assembled line stations arrive in sections for sequential installation per the engineered layout
- First-run parameter setting covering barrel temperatures, moisture rates and roller pressure
- Operator training on PLC interface, screw changeover and flaking roller adjustment
- Wear parts list covering screws, dies and roller surfaces with recommended replacement intervals
What We Need to Configure Your Line
Share your grain formulation — whether straight corn flour or a multi-grain blend — along with the particle size distribution and target moisture content. Confirm your local voltage and frequency, the control language your operators require, and the daily output you need to meet. If you have existing upstream mixing or downstream packing equipment, provide the interface specifications so the line integrates without gaps.
Frequently Asked Questions
Q: How is screw configuration and die design selected for my specific grain blend?
A: The screw element stack — conveying, kneading and reverse elements — is arranged based on your grain type, particle size and target flake density. Die geometry controls the pellet shape before flaking. We select both using trial data from your raw material, not from a generic template.
Q: What barrel temperature profile controls starch gelatinisation?
A: Multiple independent heating zones along the barrel manage starch gelatinisation progressively. The PLC system lets operators adjust each zone when switching formulations. Correct profiling prevents premature expansion or under-cooked starch that produces hard, dense flakes after roasting.
Q: How is output capacity verified before the line ships?
A: We run your actual raw material in our in-house testing workshop and document the results. The trial run report records stable output rate, flake density, texture and moisture content, confirming the line performs on your material before it leaves our factory.
Q: Can the same line produce both natural and sugar-coated corn flakes?
A: Yes. The sugar-coated variant adds a spraying and coating drum stage after hot air roasting. The base extrusion, flaking and drying stations remain the same, with the coating system activated or bypassed depending on the product run.