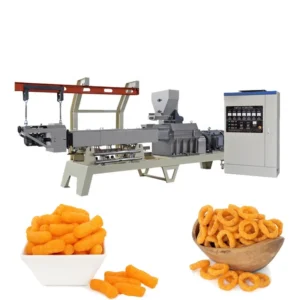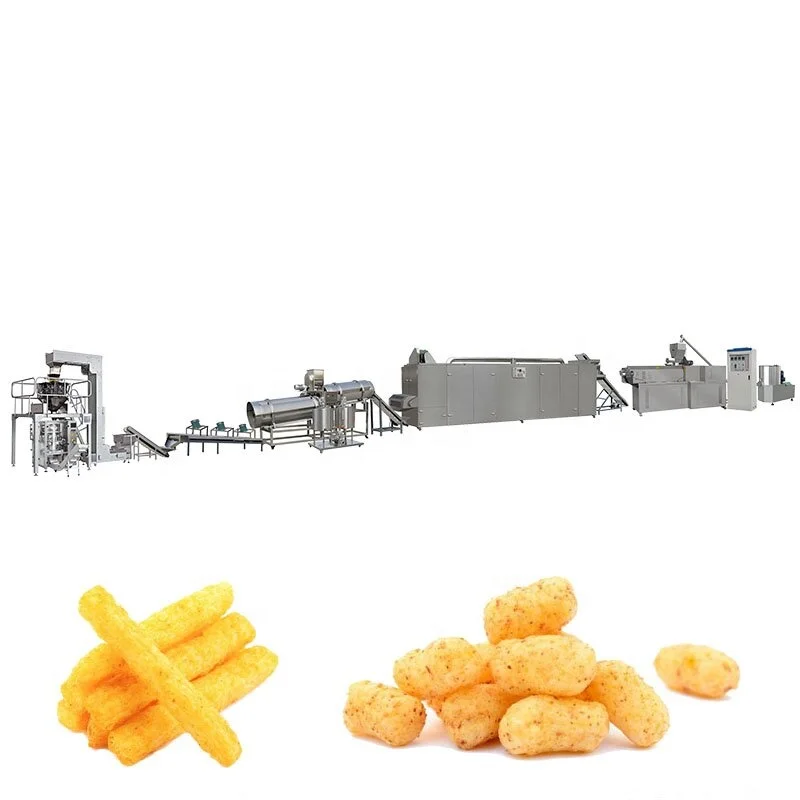
Matched Screw Geometry — Every barrel zone and die orifice is specified against the buyer’s actual grain blend, preventing the density drift that generic builds cause on non-standard moisture or particle size.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Extruder Production Line |
| Screw Type | Twin-screw |
| Installed Power (MT70) | 160 kW |
| Power Consumption (MT70) | 120 kW |
| Output Capacity (MT70) | 150–200 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| Overall Dimensions (MT70) | 41 × 1.5 × 2.2 m |
| Installed Power (MT85) | 190 kW |
| Power Consumption (MT85) | 140 kW |
| Output Capacity (MT85) | 300–400 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| Overall Dimensions (MT85) | 43 × 1.5 × 3.2 m |
| Installed Power (MT75) | 210 kW |
| Power Consumption (MT75) | 150 kW |
| Output Capacity (MT75) | 300–500 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| Overall Dimensions (MT75) | 45 × 1.5 × 3.5 m |
| Control System | PLC automated line control |
| Flaking Machine Drive | Double motors, separate roller driving, hydraulic system |
| Flaking Temperature Control | Infrared sensor |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air roasting, vibrating pan, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Lubrication | Automatic lubricating system on extruder |
| Screw Material | Wear-resistant alloy |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn, rice, wheat, oat, barley powder |
| Sugar-coated breakfast cereals | Grain flour blends with sugar glaze coating |
| Multi-shape puffed cereal snacks | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart shapes via die change |
| Fortified breakfast cereal lines | Grain base with nutritional premix integration |
What Nominal Capacity Figures Leave Out About Corn Flakes Extrusion Technology
A capacity number without a raw material baseline is a guess, not a guarantee.
I have watched buyers commit to a line based on a brochure figure, only to discover that their local corn grits — different particle size, different moisture — caused the extruder to surge and starve, leaving the baking oven idle half the shift. The corn flakes extrusion technology that holds steady throughput depends on screw pitch, barrel zone temperatures, and die geometry being configured for the specific grain blend entering the hopper, not a laboratory reference sample [NEED_CITE: starch gelatinisation behaviour across different corn grit particle sizes]. When those parameters are misaligned, the line produces flakes that shatter during roasting or turn dense and chewy in the bowl.
How Screw Configuration Controls Flake Density and Bowl Life
The twin-screw arrangement generates shear and residence time that determine the degree of starch gelatinisation inside the barrel. For corn flakes, incomplete gelatinisation leaves a hard, glassy core that the flaking rollers cannot flatten evenly; over-gelatinisation produces a sticky melt that clings to the die face and collapses after cutting. Screw element sequencing — forward conveying, kneading blocks, and reverse elements — is adjusted zone by zone so that corn flakes extrusion technology reaches the target melt viscosity exactly at the die exit.
Barrel Temperature Profile and the Moisture-Shear Balance
Each barrel zone has independent heating and cooling, allowing the operator to build a temperature ramp that matches the moisture content of the incoming blend. Higher moisture requires more energy input in the early zones to bring the starch past its gelatinisation threshold, while lower moisture demands tighter temperature control to avoid scorching. The balance between thermal input and mechanical shear is what keeps expansion ratio consistent across a long production run [NEED_CITE: barrel zone temperature ramping for cereal extrusion]. Infrared sensors on the downstream flaking station monitor sheet temperature in real time, feeding back to the PLC so roller gap and speed stay synchronised with extruder output.
Reading the Specs: What the Numbers Mean for Your Floor
The installed power figures — ranging across the MT70, MT85, and MT75 models — reflect motor capacity available for screw drive, not continuous draw; actual power consumption sits lower under typical running conditions. Overall line length extends beyond the extruder itself: mixing, flaking, drying, hot air roasting, sugar coating, and cooling stations must all fit within the stated footprint envelope, so workshop length and ceiling height need to accommodate the full layout. The hydraulic double-roller flaking system demands a stable supply pressure to maintain uniform flake thickness, and the roasting oven’s dual circulating fans with cyclone dust removal require ducting clearance above the vibrating pan. PLC control centralises these stations into one interface, reducing the operator count needed to monitor the full sequence from batching to packing.
The Hidden Cost of Skipping the Trial Run
Lines shipped without a material-specific trial often arrive with screw and die settings calibrated to a generic corn flour standard. When the buyer’s actual raw material has higher fibre content or a wider particle distribution, the extruder’s feed section cannot meter consistently, causing pressure pulses that show up as thickness variation in the flaked sheet. These pulses carry through to the roasting oven, where thinner flakes over-brown and thicker flakes remain under-toasted, producing a mixed batch that fails bowl-life testing [NEED_CITE: flake thickness uniformity and bowl-life correlation]. The cost is not a single rejected shipment — it is weeks of line downtime while screw elements are re-profiled and new dies are machined and shipped.
Why the Extrusion Technology Angle Matters Here
Screw configuration and die design are specified against the buyer’s submitted raw material, not copied from a reference build, so starch behaviour in the barrel matches the target flake texture. The in-house testing workshop runs the buyer’s own grain blend through the extruder before shipment, generating a trial run report that documents throughput, melt temperature, and flake density under real conditions. Line layout calculations balance throughput at every station — mixing, flaking, drying, roasting, coating — so no single point bottlenecks the sequence. Electrical schematics confirm voltage, frequency, and control language for the destination market before the control panel is wired, avoiding commissioning delays on site.
Documentation & Verification
- Screw and die configuration record matched to your submitted grain blend
- Trial run report on your raw material documenting throughput and flake density
- Line layout with throughput calculation across every station
- Electrical schematic confirming voltage, frequency, and PLC language
- CE declaration of conformity and ISO certificate
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Foundation plan accounts for full line length up to 45 m depending on model selected
- Dedicated power circuit sized to installed power rating with voltage and frequency confirmed for local grid
- Extruder, flaking station, and roasting oven shipped as separate modules for workshop door clearance
- PLC parameter sets loaded from trial run data, then fine-tuned during on-site commissioning
- Operator training covers screw element inspection intervals and hydraulic roller pressure adjustment
- Wear parts list identifies screw segments, die inserts, and flaking roller surfaces with replacement cycle guidance
Preparing Your Inquiry
To move from a general capacity range to a firm line configuration, share the grain blend composition, particle size distribution, and moisture content of the raw material you intend to process. Specify the target flake format — natural or sugar-coated — along with any additional cereal shapes you plan to run on the same extruder via die changes. Confirm the workshop floor dimensions, ceiling height, and the local voltage and frequency standard so the layout and electrical package can be finalised before production begins.
Frequently Asked Questions
Q: How is screw configuration matched to my specific grain blend?
A: We review your raw material’s particle size, moisture, and starch content, then select screw element geometry and sequence for each barrel zone. A trial run on your actual material in the testing workshop confirms melt behaviour and flake density before the configuration is locked.
Q: What extrusion parameters control whether the flake meets crunch specification?
A: Moisture content at the die exit, barrel temperature ramp, and screw shear intensity together determine expansion ratio and cell structure. Adjusting any one of these shifts the balance between surface blistering during roasting and internal crispness after cooling.
Q: Can the extruder produce shapes beyond corn flakes?
A: Yes. Swapping the die plate allows production of rings, balls, tubes, stars, and other puffed cereal shapes. The screw configuration may need adjustment for different expansion ratios, which is evaluated during the pre-shipment trial.
Q: How is line throughput verified before shipment?
A: Your raw material is run through the extruder in the testing workshop, and output is measured over a sustained period. The trial run report records actual throughput, power draw, and flake quality metrics against the capacity target.
Q: What is the starch gelatinisation profile across the barrel zones?
A: Temperature and shear are staged from the feed zone through the melt zone so that starch conversion completes before the material reaches the die. The profile is adjusted based on your grain composition, which may include corn, rice, wheat, oat, or barley blends.