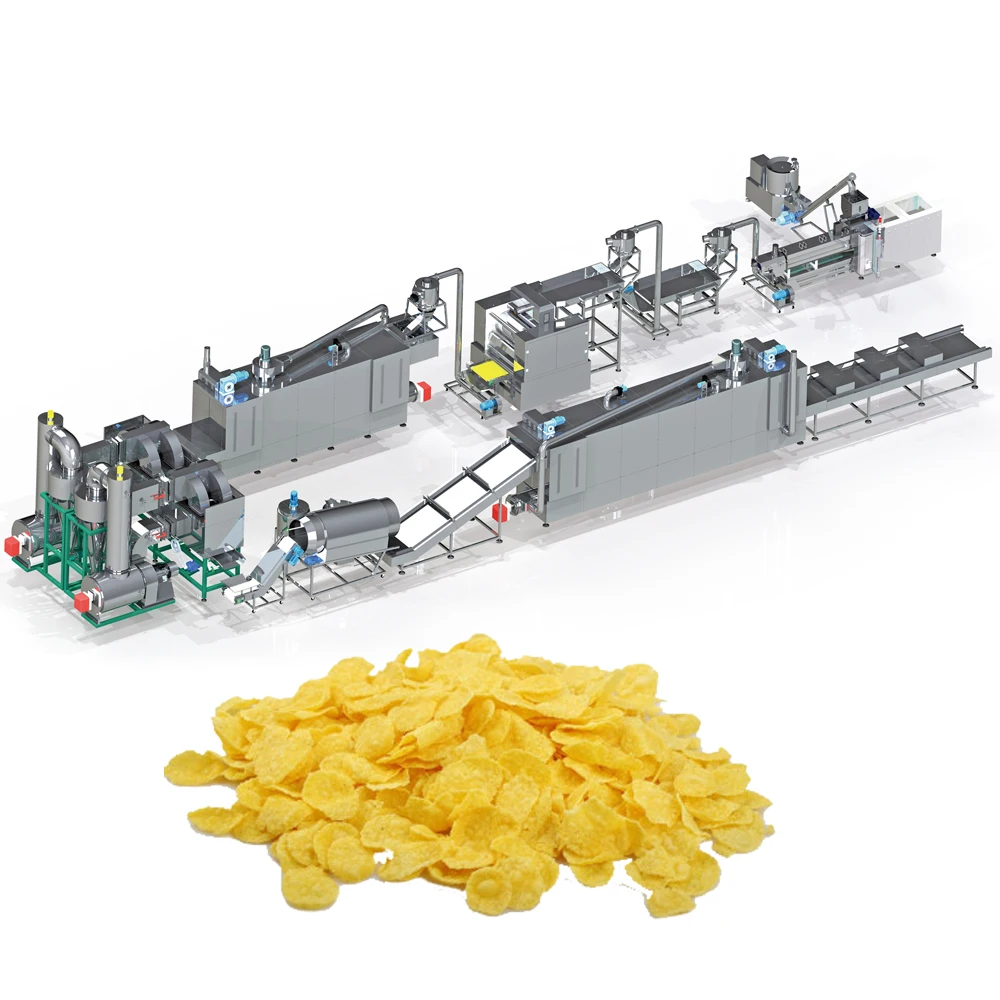
Screw Configuration Matched to Your Grain Blend — every barrel zone and die geometry is specified against the buyer’s actual corn, oat, or multigrain formulation before production begins.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-65 / MT-70 / MT-75 / MT-85 |
| Product Type | Corn Flakes Production Line |
| Screw Type | Twin screw (modular sections) |
| Installed Power | MT-65: 84 kW / MT-70: 132 kW / MT-75: 186 kW / MT-85: 239 kW |
| Real Power Consumption | MT-65: 59 kW / MT-70: 92 kW / MT-75: 140 kW / MT-85: 167 kW (basis to be confirmed) |
| Output Capacity | MT-65: 120–150 kg/h / MT-70: 200–250 kg/h / MT-75: 300–400 kg/h / MT-85: 400–500 kg/h (basis to be confirmed) |
| Overall Dimensions (L×W×H) | MT-65: 12000×1200×2200 mm / MT-70: 23000×1500×2200 mm / MT-75: 24000×1500×2800 mm / MT-85: 28000×1500×2800 mm |
| Mixer Tank Size | φ600×500 mm |
| Mixer Power | 4 kW |
| Screw Conveyor Power | 0.75 kW |
| Corn Flakes Press Power | 16.12 kW |
| Press Roller Size | 510×310×1050 mm |
| High-Temperature Oven Dimensions | 4500×1400×1800 mm |
| Oven Heating Source | Gas-fired baking |
| Sugar Spraying System Power | 28.75 kW |
| Sugar Spraying Roller Size | Ø600×2700 mm |
| Control System | PLC and MCC |
| Gear Box Lubrication | Oil forced automatic lubrication |
| Extruder Self-Cleaning | Yes |
| Warranty | 1 year with lifetime maintenance |
| Lead Time | 5–30 days after advance payment (basis to be confirmed) |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional corn flakes breakfast cereal | Corn grits and corn flour at controlled moisture |
| Oat-based breakfast flakes | Oat bran and oat flour blends requiring adjusted gelatinisation temperature |
| Multigrain flakes | Rice flour, wheat flour, and soya bean combinations |
| Sweetened and coated flakes | Corn base with sugar, chocolate, or honey coating |
| Puffed and extruded snack variants | Corn, peanut, and walnut formulations on reconfigured screw profile |
What a Generic Screw Profile Does to Your Flake Density
The extruder screw is not a commodity part — it defines whether your corn flakes float in the bowl or sink to the bottom.
I spent two weeks reworking a line that shipped with a standard screw build because the buyer switched from pure corn grits to a blend heavy in oat bran. The gelatinisation window shifted, the pellets came out dense, and after pressing and baking the flakes were too hard and too thick for the target market. When twin screw extruder corn flakes lines are configured without testing the actual raw material, the problems show up at the press roller, not at the extruder barrel — by which point the starch structure is already wrong. Generic die and screw combinations produce pellets that either over-expand or under-cook, and no amount of oven temperature adjustment can fix a pellet that was poorly gelatinised upstream. [NEED_CITE: starch gelatinisation behaviour across grain types in extrusion processing]
Barrel Temperature Zones and Starch Gelatinisation Control
Corn starch requires a specific thermal profile to reach full gelatinisation without premature expansion inside the barrel. The modular screw sections on the MT series allow transport, mixing, de-gassing, cooking, and forming zones to be arranged in a sequence matched to the moisture content and starch composition of the incoming blend. Each barrel zone operates under independent temperature control, which is critical when corn flakes extrusion technology must accommodate blends that shift between high-corn and high-oat formulations across production runs.
Die Geometry and Pellet Formation Before Pressing
The die plate determines pellet cross-section, wall thickness, and cut length — all of which directly influence how the pellet flattens under the press roller. A die opening that is too large produces pellets that spread unevenly and yield flakes with inconsistent thickness. Proper die selection, paired with the non-stop cutting system, ensures uniform pellet geometry so the downstream corn flakes press machine produces a consistent flake profile across the full width of the roller. [NEED_CITE: die design principles for pellet-based breakfast cereal extrusion]
Reading the Specs That Actually Matter for Flake Quality
The twin screw configuration across the MT-65 through MT-85 range provides a configurable L/D ratio that determines material residence time inside the barrel. Longer residence time supports complete starch gelatinisation for harder grains, while shorter configurations suit moisture-rich blends that cook faster. The oil forced automatic lubrication system on the gear box maintains torque stability during continuous runs, preventing screw speed fluctuation that would otherwise create density variation in the extruded pellets. The gas-fired high-temperature oven delivers dual-side baking, which is necessary because single-side heat produces flakes that curl unevenly and break during packing. The sugar spraying system with its Ø600×2700 mm roller applies coating uniformly before the final drying stage, and the PLC control system keeps barrel temperature, screw speed, and feed rate synchronised across every production batch.
When the Press Roller Gap Is Wrong
I have seen lines where the extruder performed well but the press roller gap was set without reference to the pellet moisture leaving the extruder. The result was flakes that were either paper-thin and brittle or thick enough to remain doughy after baking. When flake thickness is off, the sugar coating adheres unevenly, bowl life shortens, and the product fails texture tests at the buyer’s distribution centre. These problems are not visible at factory acceptance if the trial run uses a different raw material than the one the buyer will actually run. [NEED_CITE: post-extrusion pressing parameters and cereal flake texture outcomes]
Why the Line Must Be Specified as a System
Every station on this corn flakes production line — mixer, screw conveyor, twin screw extruder, press machine, high-temperature oven, and sugar spraying system — is matched for throughput by a single supplier, which means the press roller capacity aligns with extruder output and the oven length is calculated against the line speed. The screw configuration and die design are documented against the buyer’s raw material, not copied from a previous installation. An in-house testing workshop runs the buyer’s actual grain blend before shipment, generating a trial run report that confirms gelatinisation degree, pellet density, and flake crispness. Electrical schematics are prepared with voltage and frequency confirmed for the destination market before production starts. CE and ISO certification documentation is provided as part of the standard delivery package.
Documentation & Verification
- Screw and die configuration record matched to your grain formulation
- Trial run report on your raw material conducted before shipment
- Line layout with throughput calculation across every station
- Electrical schematic with destination voltage and frequency confirmed
- CE declaration of conformity and ISO certificate included
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Foundation plan aligned to the MT-85 footprint of 28000×1500×2800 mm
- Dedicated electrical circuit sized to the MT-75 real power draw of 140 kW
- Gas supply connection specified for the high-temperature oven burner configuration
- PLC parameter setting and barrel zone calibration during on-site commissioning
- Operator training on screw combination changes for different grain blends
- Wear parts list covering screws, dies, and press roller surfaces
Preparing Your Inquiry
To configure the right extrusion profile, we need your target flake specification, the exact grain blend and moisture range you will run, your daily output target, and the voltage and frequency standard at your facility. If you are replacing an existing line, share the current screw configuration and any throughput bottlenecks you have documented.
Frequently Asked Questions
Q: How is screw configuration selected for different grain blends?
A: The screw combination is built from modular sections arranged to control transport speed, shear intensity, and residence time. High-corn blends with lower moisture need more cooking zones and higher barrel temperatures, while oat-heavy blends gelatinise at lower thresholds and require gentler shear profiles. The configuration is finalised after a trial run on the buyer’s actual material.
Q: What barrel temperature profile prevents over-expansion in corn flakes?
A: Corn starch gelatinises within a narrow thermal window. Too much heat in the early zones causes premature expansion inside the barrel, producing hollow pellets that collapse at the press. The profile is ramped gradually across barrel zones, with the cooking zone held at the gelatinisation peak and the forming zone cooled slightly to stabilise pellet density before the die.
Q: How does press roller gap affect final flake crispness?
A: The roller gap determines flake thickness, which directly controls how thoroughly the flake bakes in the oven. Thinner flakes bake through completely and achieve a crisp bowl-life, while thicker flakes retain internal moisture and turn soft after packaging. The gap is set relative to pellet moisture content leaving the extruder and verified during the pre-shipment trial run.
Q: How is output capacity verified on actual raw material?
A: The buyer’s grain blend is run through the extruder in the testing workshop before shipment. Throughput is measured at the press and oven stages under production-equivalent conditions. The trial run report documents actual output alongside pellet density and flake texture measurements, replacing nominal capacity figures with verified data.
Q: What happens if voltage and frequency are not confirmed before production?
A: Motor ratings, PLC input specifications, and oven ignition systems are all voltage-dependent. A machine built for 380V/50Hz will not commission correctly on a 440V/60Hz supply without component replacement. Electrical schematics are therefore prepared with destination specifications confirmed, and any required transformer or drive adjustments are integrated at the factory.