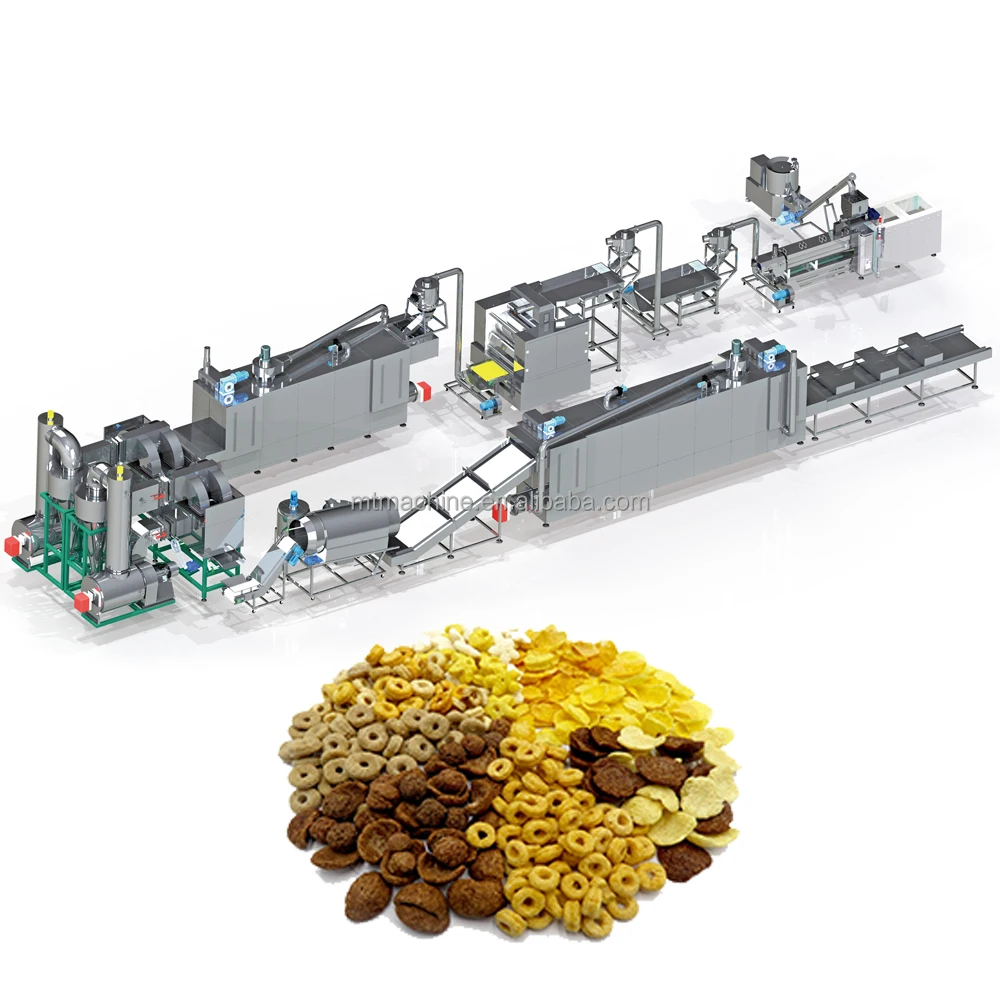
Screw and Die Geometry Matched to Your Grain — every MT75 line ships with a documented screw configuration record based on your actual corn, oat, or multi-grain formula, not a generic build copied across unrelated applications.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Corn Flake Breakfast Cereal Production Line |
| Model | MT75 |
| Extruder Type | Twin Screw (MT-75) |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/h (basis not stated in source — confirm raw material, moisture content, and flake thickness) |
| Extruder Capacity | 200–300 kg/h (basis not stated in source — confirm raw material and moisture) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC control with MCC available |
| Flaking System | Hydraulic double rollers, dual-motor drive, infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric (configurable) |
| Roasting Oven | Hot air with vibrating pan, high-temperature spraying tubes, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Basic Raw Materials | Corn, rice, wheat, oat, barley powder |
| Final Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (via die change) |
| Assembly State | Complete line, fully automatic |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | Corn grits and corn flour at controlled moisture |
| Sugar-coated breakfast cereal | Corn, rice, or wheat base with sugar spray and tumble coating |
| Multi-grain flake processing | Blends of oat, barley, wheat, and rice requiring screw profile adjustment |
| Extruded cereal snack shapes | Rings, loops, stars, and balls via die swap on the same extrusion platform |
Why "300 kg/h" Means Nothing Without the Formula Behind It
A capacity number detached from raw material behaviour is a promise the machine cannot keep on your shop floor.
I spent weeks in a Central American plant where the corn flakes extrusion production line was specified for standard corn grits, but the client switched to a high-fibre whole-grain blend the week before commissioning. Output dropped sharply, the flakes tore at the roller gap, and the entire screw profile had to be reworked on-site. That delay cost far more than getting the formula right at the proposal stage [NEED_CITE: impact of raw material variability on extrusion throughput]. When buyers treat a quoted throughput as a fixed guarantee rather than a function of moisture, starch content, and particle size, the line underperforms from day one.
Barrel Temperature Profile and Starch Gelatinisation
The twin-screw extruder on this line divides the barrel into independently heated zones, each contributing to a controlled thermal curve. Corn starch gelatinises within a specific temperature and moisture window; too cool and the dough lacks cohesion for clean flaking, too hot and the sheet blisters before reaching the roller station. Configuring the corn flakes extrusion production line around your grain’s gelatinisation behaviour is what separates consistent bowl-life from flakes that go soggy in minutes.
Die Geometry, Expansion Ratio, and Flake Density
The die plate determines the cross-section and initial expansion of the extrudate before it enters the flaking rollers. A wider die opening with a shorter land length produces a lower-density sheet that roasts into a lighter, more fragile flake. Tightening the geometry increases shear and density, yielding a thicker flake with longer crunch retention. Matching die design to the target texture is a core part of the engineering work before the line ships [NEED_CITE: relationship between die land length and extrudate expansion in food extrusion].
Reading the Spec Sheet: What the Numbers Actually Control
The MT75 runs a 210 kW installed motor array drawing approximately 150 kW during steady-state production — that gap reflects the thermal headroom needed when processing higher-moisture multi-grain blends that demand more barrel energy. The 45-metre line footprint covers every station from mixer through packing, meaning utility planning must account for the full stretch of electrical, gas, and compressed-air runs rather than just the extruder. The PLC-controlled flaking unit uses hydraulic pressure on dual independently driven rollers with infrared temperature sensing across the roller surface — this matters because uneven roller temperature produces flakes with variable thickness, and thickness directly determines roasting uniformity and final crunch. Gas or electric dryer heating is selectable to match local utility costs and availability, a decision that should be locked in before fabrication begins.
The Hidden Cost of Skipping the Trial Run
Lines that ship without a documented trial on the buyer’s actual raw material arrive with generic screw elements and a default die set. Commissioning then becomes the trial — except it happens on your production floor, burning your ingredients, your utilities, and your schedule while engineers swap configurations. Flakes produced on untested settings often fail density and bowl-life specifications, forcing reformulation or hardware changes that delay market launch [NEED_CITE: cost of post-installation line reconfiguration in food extrusion projects]. The problem compounds when downstream stations like the roasting oven and sugar coating drum are sized for a throughput the extruder never actually delivers on the real formula.
Why This Supplier Fits Technical Buyers
Screw configuration and die design are specified to each buyer’s raw material and target flake density, not pulled from a catalogue default. An in-house testing workshop runs your actual corn or multi-grain blend before shipment, producing a trial report that validates expansion, texture, and throughput. Every station — extruder, flaking rollers, dryer, roasting oven, coating drum — is matched for throughput under one supplier, eliminating the bottleneck that forms when equipment is sourced from separate vendors. Thermal management spans from barrel zones through drying and roasting, coordinated rather than independently tuned. Documentation includes a complete screw and die configuration record tied to your specific formula.
Documentation & Verification
- Screw and die configuration record matched to your corn or multi-grain formula
- Trial run report on your raw material validating flake density and texture before shipment
- Line layout with capacity calculation showing throughput balance across all stations
- Electrical schematic with voltage, frequency, and control language confirmed for your market
- CE declaration of conformity and ISO certificate included in shipping documentation
- Operation and maintenance manual with wear parts list specific to the MT75 configuration
Installation, Commissioning & Support
- Foundation plan accounts for the full 45-metre line length and vibrating roasting pan load
- Dedicated electrical circuit sized for 210 kW installed capacity with voltage and frequency confirmed pre-build
- Extruder barrel segments and screw elements shipped disassembled for site-specific reassembly and alignment
- Commissioning includes barrel temperature profiling and flaking roller gap calibration on your grain blend
- Operator training covers PLC interface navigation, die changeover, and roller temperature sensor maintenance
- Wear parts list specifies replacement intervals for screws, dies, and roller surfaces based on your material abrasiveness
What We Need to Build Your Line
Before any configuration is locked, share your primary grain type and any multi-grain blend ratios, target flake thickness and bowl-life specification, and daily or shift-based output expectation. We also need your facility’s available voltage and frequency, preferred control language for the PLC interface, and whether you require a trial run on your raw material before the line ships.
Frequently Asked Questions
Q: How is screw configuration selected for corn versus multi-grain blends?
A: Corn grits and whole-grain oat or barley blends differ in starch content, fibre level, and moisture absorption. Each blend requires a specific screw element sequence — varying kneading block angles and reverse elements — to control shear, residence time, and gelatinisation. The configuration is documented and tested on your material before the corn flakes extrusion production line ships.
Q: What barrel temperature range and moisture level produce the target flake density?
A: Most corn flake formulations gelatinise effectively between defined barrel zone temperatures at a moisture content that balances expansion with sheet integrity. The exact profile depends on your grain’s starch composition. A trial run establishes the thermal curve and moisture target that delivers the density and bowl-life your market expects.
Q: Can the line run a production trial on our specific raw material before shipment?
A: Yes. The in-house testing workshop runs your actual corn, oat, or multi-grain formula through the configured extruder, flaking unit, and roasting oven. The resulting trial report documents expansion ratio, flake thickness, and texture, confirming the line meets specification before it leaves the factory.
Q: How are roller gap and roasting temperature set for consistent flake thickness?
A: The hydraulic double-roller flaking unit holds a precise gap under PLC control, while infrared sensors monitor roller surface temperature to prevent uneven sheet compression. Downstream, the hot air roasting oven uses dual circulating fans and a vibrating pan to ensure uniform heat exposure, producing consistent surface bubbling and crunch across the entire batch.
Q: What die options allow switching between corn flakes and other cereal shapes?
A: The extruder accepts interchangeable die plates. Standard options produce flakes when paired with the flaking rollers, and shapes including rings, loops, stars, and balls when the extrudate is cut directly at the die face. Switching requires a die change and corresponding screw profile adjustment, both documented in the configuration record.