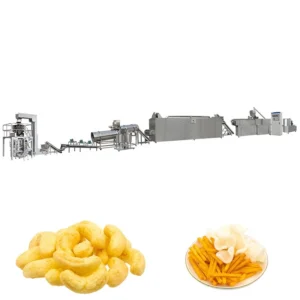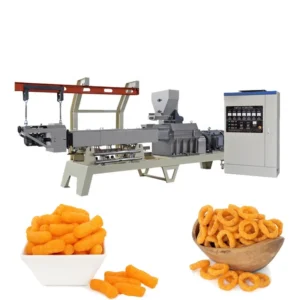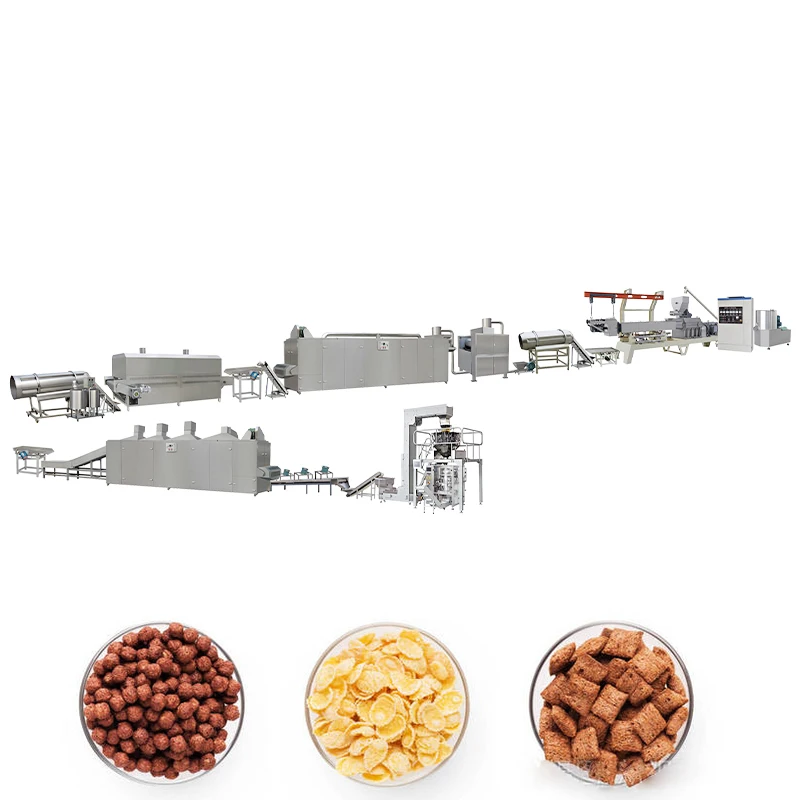
Screw Configuration Matched to Raw Material — die geometry and barrel zones are specified against the buyer’s actual grain blend before the line is built, not copied from a generic template.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Corn Flakes Production Line |
| Extruder Type | Twin Screw |
| Available Models | MT70, MT85, MT75 |
| Installed Power (MT70) | 160 kW |
| Installed Power (MT85) | 190 kW |
| Installed Power (MT75) | 210 kW |
| Power Consumption (MT70) | 120 kW |
| Power Consumption (MT85) | 140 kW |
| Power Consumption (MT75) | 150 kW |
| Output Capacity (MT70) | 150–200 kg/h (basis to be confirmed) |
| Output Capacity (MT85) | 300–400 kg/h (basis to be confirmed) |
| Output Capacity (MT75) | 300–500 kg/h (basis to be confirmed) |
| Overall Dimensions (MT70) | 41 × 1.5 × 2.2 m |
| Overall Dimensions (MT85) | 43 × 1.5 × 3.2 m |
| Overall Dimensions (MT75) | 45 × 1.5 × 3.5 m |
| Control System | PLC and MCC |
| Flaking Machine | PLC-controlled hydraulic double rollers, double motors, infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air with conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Screw Feature | Wear-resistant, special manufacturing technology |
| Lubrication | Automatic lubricating and cooling |
| Die Configuration | Adjustable mould for ball, tube, stick, ring, fruit loop, star, wheel, flower, heart |
| Raw Material Compatibility | Corn, rice, wheat, oat, barley powder |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits and corn flour blends |
| Sugar-coated corn flakes | Corn base with sugar or honey glaze |
| Multi-grain breakfast cereals | Rice, wheat, oat, and barley powder mixes |
| Shaped cereal variants | Fruit loops, stars, rings, hearts via interchangeable dies |
| Continuous-line cereal output | Integrated mixing through extrusion, flaking, roasting, and packing |
Why Nominal Capacity Figures Mislead on Corn Flakes Extrusion Line Specifications
A rated throughput number means nothing if the screw profile and barrel temperature zones were never matched to the grain blend you actually run.
I spent years on extruder service calls across the Yangtze Delta region before moving into technical pre-sales. One breakfast cereal producer commissioned a corn flakes line that looked solid on paper, but their in-house corn flour blend refused to gelatinise properly. The flakes turned to mush the moment they hit milk. The root cause was a barrel temperature curve and die compression ratio pulled from a standard build, never adjusted for their specific starch composition and particle size. The screw configuration had to be rebuilt from scratch before the line held stable output [NEED_CITE: starch gelatinisation temperature ranges for corn versus oat matrices]. When buyers evaluate corn flakes extrusion line specifications, the first question should always be whether the supplier has tested on the buyer’s actual raw material.
How Screw Geometry Governs Starch Gelatinisation in Corn Flakes
The twin-screw extruder is where the entire corn flakes texture is decided. Screw element arrangement — conveying, kneading, and reverse-pitch sections — controls shear intensity and residence time inside the barrel. Corn starch requires a specific thermal and mechanical input window to reach full gelatinisation without over-dextrinisation. If the kneading blocks are too aggressive, the dough shears into a sticky mass that flakes unevenly; too gentle, and the starch remains partially raw, producing flakes that shatter during roasting. Each barrel zone is independently heated, and the temperature profile must track the gelatinisation curve of the grain blend being processed, not a generic corn-only setting.
Barrel Zone Profiling and Die Compression for Target Flake Density
Achieving the correct flake density — the parameter that determines whether corn flakes stay crisp in milk or collapse within seconds — depends on how the extruder manages moisture and pressure through the final barrel zones and into the die. The die compression ratio must match the dough viscosity at the point of exit. A blend with higher oat or barley content behaves differently from pure corn grits because beta-glucan alters melt elasticity. The adjustable die on this line allows operators to tune the exit pressure, and the hydraulic double-roller flaking station downstream maintains uniform sheet thickness via PLC-controlled gap adjustment [NEED_CITE: relationship between extrudate moisture content and flake integrity in breakfast cereal processing]. Infrared sensors on the flaking rollers monitor surface temperature in real time to prevent sticking or tearing.
Reading the Specs That Actually Matter for Cereal Extrusion
Installed power ratings across the MT70, MT85, and MT75 models range from 160 kW to 210 kW, but the more telling figure is power consumption — 120 kW to 150 kW respectively — because that reflects the actual thermal and mechanical energy going into the barrel during steady-state production. The overall line length stretches from 41 metres to 45 metres depending on model, which signals how many drying and roasting stages are integrated; longer lines typically include dedicated sugar-coating and secondary drying stations for coated variants. The PLC and MCC control architecture means each station — mixing, extruding, flaking, drying, hot air roasting, cooling — communicates throughput status so that no single stage bottlenecks the rest. The hot air roasting oven uses a conciliation burner with two independent circulating fans and a cyclone dust removal device, which gives process engineers separate control over surface blistering intensity and airflow velocity, both critical to achieving the characteristic corn flake crispness without scorching.
The Cost of Skipping Raw Material Trials Before Shipment
When a corn flakes extrusion line arrives at a factory with screw elements configured for a generic corn recipe, and the buyer’s actual grain blend includes rice flour or oat bran, the commissioning period stretches from days into weeks. Operators waste raw material chasing the right gelatinisation point, adjusting barrel temperatures and moisture feed rates by trial and error. Flakes come off the roaster too dense, too fragile, or with inconsistent blistering [NEED_CITE: typical commissioning delays caused by untested screw configurations on food extrusion lines]. In worst-case scenarios, the die and screw combination must be replaced entirely, meaning new tooling, new lead times, and production schedules pushed back by months. All of this is avoidable if the supplier runs the buyer’s material through a test extruder before the line ships.
What This Line Brings to the Table
The extruder screw configuration and die design are specified to the buyer’s raw material and target flake density, not pulled from a catalogue default. Every station from the batching mixer through the roasting oven and coating drum is throughput-matched so that the flaking unit, dryer, and cooling conveyor keep pace with the extruder output rather than creating choke points. The in-house testing workshop runs trial batches on the customer’s grain blend before the equipment leaves the factory, producing a documented trial run report with the parameters that actually work. Pre-sales engineering covers line layout, utility planning, and electrical schematics confirmed against the buyer’s local voltage and frequency. Post-installation support includes operator training on the PLC interface and a wear parts list covering screws, dies, and roller surfaces.
Documentation & Verification
- Screw and die configuration record mapped to your grain blend and target flake density
- Trial run report on your raw material conducted before factory dispatch
- Line layout and capacity calculation confirming throughput balance across every station
- Electrical schematic with voltage and frequency confirmed for your local grid standard
- Operation and maintenance manual with PLC parameter reference tables
Installation, Commissioning & Support
- Foundation and floor space planning based on the 41–45 metre line footprint and station layout
- Dedicated electrical circuit sized to the 120–150 kW operating load with confirmed voltage and frequency
- Assembly and alignment of hydraulic flaking rollers and dual-fan roasting oven on site
- First-run parameter setting on your grain blend with barrel zone temperature and screw speed calibration
- Operator training on PLC interface, die changeover, and roller gap adjustment procedures
- Wear parts inventory plan covering screw elements, die inserts, and flaking roller surfaces
What to Include in Your Technical Enquiry
To configure a corn flakes line that actually holds throughput on your grain blend, share your raw material composition including particle size and moisture content, target product format (natural, sugar-coated, or shaped variants), daily output requirement, and available floor space with ceiling height. Confirm your local voltage and frequency standard, and specify whether the PLC interface needs to operate in a particular language. If you have an existing upstream mixer or downstream packing system, note the model and throughput so the line can be matched at the connection points.
Frequently Asked Questions
Q: How is screw configuration selected for a specific grain blend?
A: The screw element arrangement — conveying, kneading, and reverse-pitch sections — is configured based on the starch composition, fat content, and particle size of the buyer’s grain blend. A trial run on the actual raw material in the testing workshop confirms the correct geometry before the production line is assembled, ensuring gelatinisation targets are met without guesswork during commissioning.
Q: What barrel temperature profile produces correct starch gelatinisation for corn flakes?
A: The profile depends on the grain blend. Pure corn grits typically gelatinise in a different temperature window than blends containing oat or barley, where beta-glucan shifts the melt behaviour. Each barrel zone is independently controlled, and the profile is set during the pre-shipment trial run on the buyer’s material, then documented for the operator to reference.
Q: How is throughput verified on the buyer’s raw material?
A: Before shipment, the buyer’s grain blend is run through the extruder in the testing workshop at the intended production moisture and feed rate. Output is measured, flake density is checked after roasting, and the results are recorded in a trial run report that ships with the line, giving the buyer confirmed parameters from day one of installation.
Q: How do the flaking rollers and roasting oven control final flake texture?
A: The PLC-controlled hydraulic rollers maintain a precise gap to produce uniform sheet thickness, while infrared sensors monitor roller surface temperature to prevent dough sticking. Downstream, the hot air roasting oven uses a conciliation burner and dual circulating fans to control blistering intensity and moisture removal, which together determine the final crispness and milk-bowl stability of the corn flake.