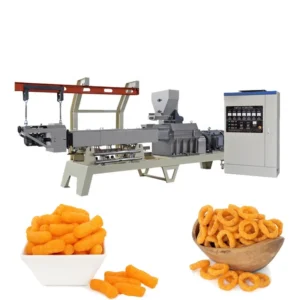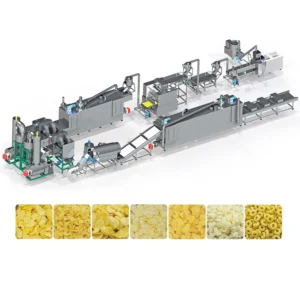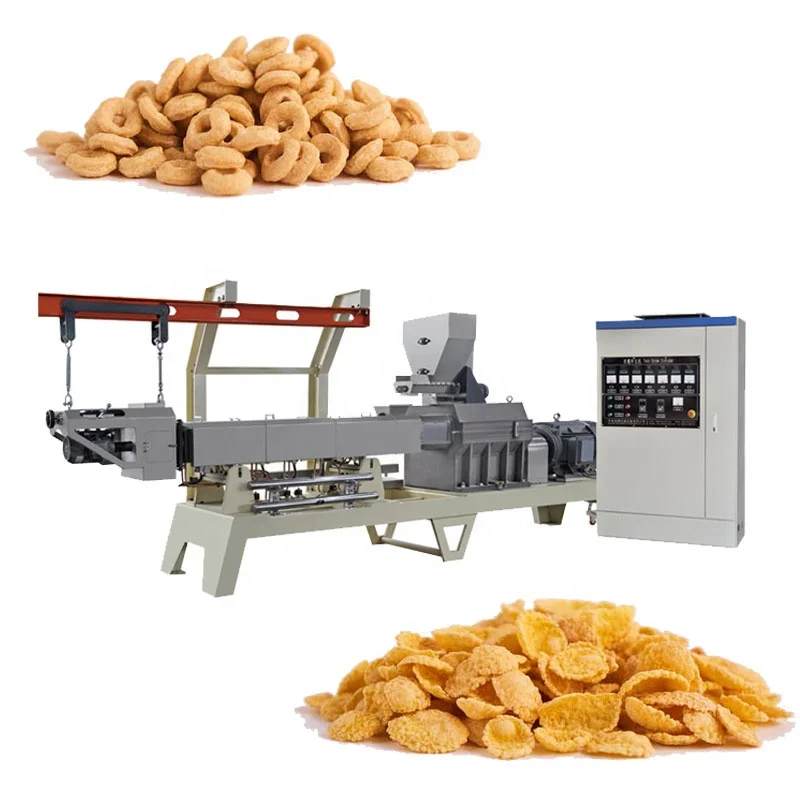
Screw Configuration Matched to Your Raw Material — Every module arrangement and die geometry is specified after analyzing your corn or multi-grain flour’s starch profile, not copied from a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Making Machine / Breakfast Cereal Production Line |
| Model | MT-65 / MT-70 / MT-85 / MT-75 |
| Screw Type | Co-rotating twin screw with sectional modules |
| Installed Power | MT-65: 84 kW; MT-70: 132 kW; MT-85: 239 kW; MT-75: 186 kW |
| Real Power Consumption | MT-65: 59 kW; MT-70: 92 kW; MT-85: 167 kW; MT-75: 140 kW |
| Output Capacity | MT-65: 120–150 kg/h (basis to be confirmed); MT-70: 200–250 kg/h (basis to be confirmed); MT-85: 300–400 kg/h (basis to be confirmed); MT-75: 400–500 kg/h (basis to be confirmed) |
| Overall Dimensions (L×W×H) | MT-65: 21000×1200×2200 mm; MT-70: 23000×1500×2200 mm; MT-85: 28000×3500×4300 mm; MT-75: 24000×1500×2800 mm |
| Control System | PLC and MCC with separate flaking press controller |
| Flaking Press Power | 16.12 kW |
| Flaking Press Roller Size | 510×310×1050 mm |
| High-Temperature Oven | Gas-fired, both-side baking, 4.5×1.4×1.8 m |
| Raw Material Form | Powder (flour) or grits |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional corn flake production | Corn grits or corn flour at controlled moisture |
| Multi-grain breakfast cereal | Rice, millets, wheat, oat, barley blends |
| Fortified cereal with nutritional additives | Base grain flour with vitamin and mineral premix |
| Puffed snack variants on same extrusion platform | Corn, rice or mixed grain formulations |
| Nutritional convenient food manufacturing | Oat, barley or composite grain recipes |
Why Generic Screw Builds Fail at Starch Gelatinisation
The corn flakes extrusion machine screw configuration die design must match your specific grain’s gelatinisation temperature window, or the flake will never achieve proper crispness.
I once watched a line in the Middle East produce dense, lifeless flakes that sank straight to the bottom of the milk bowl. The extruder was running a standard screw profile calibrated for low-fiber corn flour. The local supplier’s corn grits carried higher fiber and a different starch composition, so the barrel temperature zones never reached the gelatinisation threshold the material demanded. Two sleepless nights of adjusting feed pitch, kneading block angles and moisture injection later, the flakes finally expanded correctly. That gap between a generic build and a material-specific configuration is where most breakfast cereal projects quietly fail [NEED_CITE: starch gelatinisation temperature ranges by grain type].
A corn flakes extrusion machine screw configuration die design copied from a different product category will produce the wrong texture and density from day one, and no amount of downstream oven tuning can fix what was never cooked properly inside the barrel.
Barrel Zone Profiling for Controlled Expansion
The co-rotating twin screw arrangement with sectional modules allows each barrel zone to serve a distinct function — feed transport, initial hydration mixing, high-shear cooking, de-gassing and final forming. By rearranging forward and reverse pitch elements, the residence time and shear intensity inside the barrel are matched to the specific starch behaviour of corn, wheat or multi-grain blends. This is the core of the corn flakes extrusion machine screw configuration die design logic, ensuring that gelatinisation completes before the material reaches the die face.
Die Geometry and the Expansion Ratio
Die aperture diameter and land length directly govern the pressure drop at the exit, which in turn controls how much the cooked mass expands upon leaving the barrel. A shorter land length reduces resistance and yields a higher expansion ratio, producing a lighter, more porous pellet that flattens into a crisp flake after pressing. Getting this geometry wrong means the flake either stays too dense or over-expands into a fragile structure that shatters during conveying [NEED_CITE: die land length and expansion ratio relationship in twin-screw extrusion].
Reading the Specs Through a Process Lens
Installed power versus real power tells you how much energy the drive system can deliver at peak versus what the process actually draws during steady-state extrusion. On the MT-85, the gap between 239 kW installed and 167 kW real consumption reflects the thermal energy recovered from the barrel heaters and the mechanical efficiency of the co-rotating screw set. The flaking press at 16.12 kW with a 510×310×1050 mm roller set provides enough torque to compress the extruded pellets to precise thickness while the integrated cooling system prevents the warm flake from sticking to the roller surface. Oven dimensions of 4.5×1.4×1.8 m with a gas-fired both-side baking system ensure that moisture is driven off uniformly, which is essential for consistent bowl-life across the entire production batch.
What Happens When the Line Stations Are Mismatched
An extruder running at full output feeding into a dryer or flaking press that cannot keep up creates a bottleneck that forces the extruder to idle or dump product. I have seen lines where the oven could not remove moisture fast enough, leaving flakes that felt leathery rather than crisp. The throughput of every station — from the mixer and screw conveyor through the air conveyor, dryer, hoister, flavoring drum, cooling machine and packing station — must be calculated against the actual extruder output on your raw material, not against a nameplate number [NEED_CITE: throughput balancing in continuous food extrusion lines].
Why Process Engineers Choose This Platform
Screw configuration and die design are documented specifically for your raw material and target flake density, not pulled from a catalog default. The in-house testing workshop runs trial batches on your actual corn, oat or multi-grain flour before the line ships, so starch behaviour and expansion characteristics are validated early. Throughput is matched across every station — extruder, dryer, flaking press, oven, coating drum — under one supplier’s responsibility, eliminating the blame game between separate vendors. Voltage, frequency and control language are confirmed against your facility’s electrical infrastructure before production begins, avoiding commissioning delays. CE and ISO certification supports import documentation requirements across regulated markets.
Documentation & Verification
- Line layout with capacity calculation matched to your grain formulation
- Screw and die configuration record for your specific raw material
- Trial run report from in-house testing on your actual flour or grits
- Electrical schematic with confirmed voltage and control language
- Factory test record documenting steady-state output before dispatch
Installation, Commissioning & Support
- Foundation planning based on the MT-85’s 28000×3500×4300 mm footprint
- Dedicated circuit sizing for up to 239 kW installed extruder power
- PLC and MCC commissioning with operator language set to your preference
- Flaking press roller gap calibration for target flake thickness on first run
- Wear parts list covering screw modules, die plates and roller surfaces
Preparing Your Extrusion Inquiry
Provide your raw material specification including grain type, particle size and typical moisture content so the screw profile can be designed around actual starch behaviour. Share your target flake density and bowl-life expectation, along with daily output targets, to determine which model in the MT-65 through MT-75 range fits your production scale. Confirm your facility’s voltage, frequency and preferred control language so electrical documentation is aligned before the build starts.
Frequently Asked Questions
Q: How is screw configuration and die design specified to my raw material and target flake density?
A: The screw module arrangement — feed elements, kneading blocks and reverse pitch sections — is selected based on your grain’s starch gelatinisation temperature and fiber content. Die aperture and land length are then calculated to deliver the expansion ratio that produces your target flake density. A configuration record is generated for your specific formulation before production begins.
Q: What barrel temperature profile and moisture range are needed for proper starch gelatinisation in corn flakes?
A: Corn starch typically requires barrel zone temperatures that bring the dough mass above its gelatinisation threshold while maintaining sufficient moisture for even cooking. The exact profile depends on your corn variety, particle size and whether fiber or protein additives are present. These parameters are established during the pre-shipment trial run on your actual raw material.
Q: How is output capacity verified on my actual raw material during the pre-shipment trial run?
A: Your flour or grits are run through the extruder in the testing workshop under the same screw configuration, barrel temperatures and moisture conditions planned for your factory. Steady-state output is measured and documented in a trial run report, confirming what the line produces on your specific material rather than relying on generic capacity figures.
Q: How does the flaking press roller gap and cooling system affect final flake thickness and crispness?
A: The adjustable roller distance on the flaking press sets the compressed pellet thickness, which directly influences how the flake toasts in the oven. The integrated cooling system keeps the roller surface temperature stable, preventing warm extrudate from adhering and tearing. Consistent gap settings across the roller width produce uniform flake geometry and predictable bowl-life.
Q: What is the relationship between extruder shear, expansion ratio and the bowl-life of the finished corn flake?
A: Higher shear inside the barrel increases starch degradation, which can reduce the structural integrity of the expanded pellet. The expansion ratio at the die determines the internal porosity of the pellet before flaking. Together, these variables control how long the pressed and toasted flake resists moisture absorption in milk, defining the bowl-life that your market expects.
 词汇验证: - Industrial(通用限定词库) - Corn Flakes Production Line(来自【分类】breakfast cereals corn flakes machine + 【产品草稿】.product_type "Corn Flakes Production Line") - Complete Line(站点修饰词池:产线方案类角色→Production Line / Turnkey Solution / Complete Line) 记录ID 10631 数字和=11,11%6=5(结构5),11%3=2(池索引2→Complete Line) 无禁用词/无编造规格/无价格/无禁用符号](https://mtextrusion.com/wp-content/uploads/2026/05/He55b4c1cec294192a848b7f7f2ee8e4dS-300x300.webp)