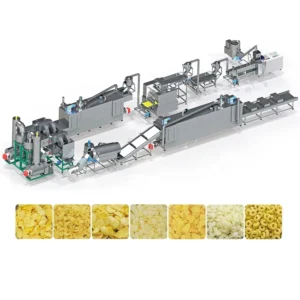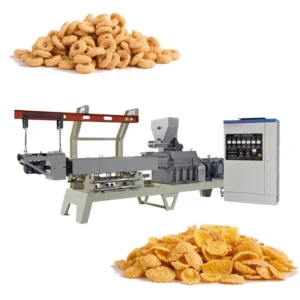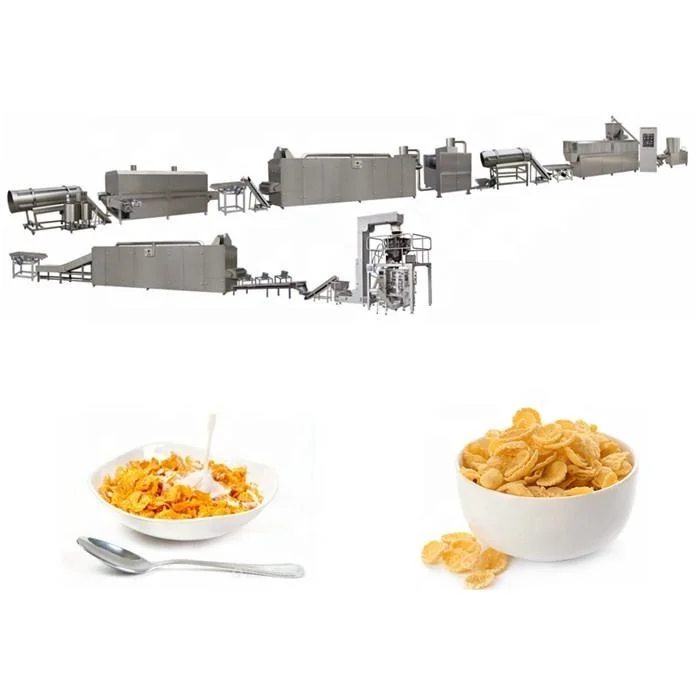
Matched screw configuration — element layout and die geometry specified to your corn, oat, or wheat formulation rather than a generic build sheet, ensuring target starch gelatinisation and flake density from day one.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes and Breakfast Cereal Production Line |
| Screw Type | Twin screw |
| Installed Power | MT70: 160 kW; MT85: 190 kW; MT75: 210 kW |
| Power Consumption | MT70: 120 kW; MT85: 140 kW; MT75: 150 kW |
| Output Capacity | MT70: 150–200 kg/h; MT85: 300–400 kg/h; MT75: 300–500 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Overall Dimensions (L×W×H) | MT70: 41 × 1.5 × 2.2 m; MT85: 43 × 1.5 × 3.2 m; MT75: 45 × 1.5 × 3.5 m |
| Control System | PLC control (flaking machinery), MCC and extruder control integrated |
| Screw Material | Special alloy technology, wear-resistant |
| Extruder Lubrication | Automatic lubricating and cooling function |
| Flaking Machinery Drive | Double motors for separate roller driving, hydraulic system for double rollers |
| Flaking Temperature Control | Infrared sensor for even temperature pipe control |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air roasting with vibrating pan, high temperature spraying tubes, conciliation burner, two separate circulating fans, cyclone dust removal device |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Line Stations (Natural Corn Flakes) | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Cooling → Packing |
| Line Stations (Sugar Coated Corn Flakes) | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Sugar Spraying → Sugar Coating → Drying → Cooling → Packing |
| Final Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (by adjusting extruder mould) |
| Raw Materials | Powder of corn, rice, wheat, oat, barley, etc. |
| Assembly State | Complete turnkey line |
| Customization | Factory layout designed to buyer’s factory size; voltage confirmed to local standard |
| Standards | CE certified; ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn powder or corn grits, uncoated clean-label cereal |
| Sugar-coated corn flakes | Corn-based extrudate with sugar slurry coating |
| Oatmeal rings and fruit loops | Oat, wheat, and multi-grain powder blends |
| Fortified breakfast cereals | Rice, barley, and mixed-cereal formulations with added nutrients |
| Multi-grain extruded shapes | Corn, rice, wheat, oat, and barley powder combinations |
Why a Generic Screw Build Fails Your Corn Flakes Extrusion Production Line
The extruder screw must be configured for your specific cereal formulation, not copied from a standard catalogue build.
I spent years doing after-sales service across the Yangtze River Delta, and the most frustrating calls always came from cereal producers running the wrong screw profile. A configuration meant for direct-expanded snacks pushes a corn flakes extrusion production line into over-expansion — the extrudate puffs too much, and when it hits the flaking rolls, it shatters instead of flattening. On the other side, an under-worked dough from a generic setup produces dense pellets that refuse to blister in the roasting oven. Neither failure mode shows up during a factory acceptance test on someone else’s raw material [NEED_CITE: twin-screw extrusion screw configuration for starch-based cereals].
Screw Element Arrangement and Starch Gelatinisation Control
The degree of starch gelatinisation inside the barrel determines whether the extrudate arriving at the flaking rolls has the right plasticity. For corn-based formulations, the kneading block section and reverse-conveying elements must be arranged to achieve partial gelatinisation — enough to create a coherent dough sheet, but not so much that the material fully expands at the die. When the corn flakes extrusion production line is reconfigured for oat or multi-grain blends, the L:D ratio and element spacing require adjustment because oat flour absorbs moisture at a different rate and gelatinises at a different temperature threshold than corn.
Barrel Temperature Profile and Moisture Injection Zones
Multi-zone barrel heating works in tandem with controlled steam or water injection at specific feed points. The temperature gradient across the barrel sections governs the melt rheology entering the die. Too much heat in the metering zone causes premature expansion before the material reaches the flaking stage; too little leaves uncooked starch particles that create hard spots in the finished flake. Process engineers running the corn flakes extrusion production line should verify that the PLC logs every barrel zone temperature and that moisture injection rates are documented per formulation [NEED_CITE: barrel temperature profiling in cereal extrusion].
Die Aperture, Land Length, and Extrudate Density
The die geometry — specifically the aperture diameter and land length — sets the cross-sectional area and density of the extrudate rope entering the flaking rolls. A shorter land length reduces die pressure and produces a less dense rope that flakes into thinner, more brittle flakes. A longer land length increases back-pressure and yields a denser rope suited to thicker, crunchier flakes. Die selection on the corn flakes extrusion production line is not a one-time decision; producers switching between natural flakes and shaped cereal pieces need interchangeable die plates with documented land lengths for each product.
Flaking Roll Temperature and Hydraulic Gap Precision
After the extrudate leaves the die and is cut into pellets, the flaking station compresses them into thin sheets. The infrared-monitored roller temperature prevents the pellets from sticking or tearing during compression. Hydraulic gap control between the two independently driven rollers maintains uniform flake thickness across the full roller width. Inconsistent thickness directly causes uneven roasting — thick zones remain doughy while thin zones burn. The corn flakes extrusion production line integrates this flaking stage immediately downstream of extrusion so that pellet temperature and moisture content remain within the window required for clean compression.
The Hidden Cost of a Mismatched Extruder-to-Dryer Ratio
I have watched producers install an extruder sized for their target capacity only to discover the downstream dryer cannot handle the moisture load, forcing the entire line to run at a fraction of the extruder’s output. The extrudate piles up between stations, cooling and hardening before it reaches the flaking rolls, which ruins flake integrity. On sugar-coated lines, an undersized coating drum creates a second bottleneck where roasted flakes wait in bins and absorb ambient humidity, losing crispness before packaging [NEED_CITE: throughput matching across cereal processing line stations]. These are not equipment defects — they are configuration errors that could be caught during line design if the buyer provides actual raw material data and target throughput figures upfront.
Why Source This Corn Flakes Extrusion Production Line Here
The screw configuration and die specification are documented against your raw material formulation, not copied from a generic twin-screw build. Every MT70, MT85, and MT75 line ships with a recorded screw element layout matched to the buyer’s target product.
In-house trial runs on the customer’s actual corn, oat, or multi-grain blend are completed in the testing workshop before dispatch, generating a trial run report that confirms gelatinisation, extrudate density, and flake quality.
The PLC and MCC control architecture integrates extruder barrel zones, flaking roll temperature, and roasting oven parameters into one system, giving operators a single interface for recipe management across natural and sugar-coated products.
Throughput calculations match extruder output to flaking, drying, roasting, and coating capacity so that no downstream station chokes the line. The line layout is designed around the buyer’s factory dimensions and local voltage standard.
Wear parts — screws, dies, and flaking roll surfaces — are specified with the initial shipment and documented in a parts list so that replacements are available before the first change-out is due.
Documentation & Verification
- Screw element layout and die configuration record matched to your cereal formulation
- Trial run report on your actual raw material from the in-house testing workshop
- Barrel zone temperature and moisture injection data logged during factory test
- Electrical schematic with voltage and frequency confirmed to your local standard
- CE declaration of conformity and ISO certificate for customs and compliance
- Wear parts list with part numbers for screws, dies, and flaking roll components
Installation, Commissioning & Support
- Foundation and floor space planned around line dimensions up to 45 m length, 3.5 m height
- Electrical supply verified against PLC and MCC requirements, typically 160–210 kW installed power
- Extruder barrel zones calibrated and moisture injection points set during on-site commissioning
- Flaking roll gap and infrared sensor calibrated to target flake thickness before first production run
- Operator training covers screw configuration changes for switching between corn, oat, and multi-grain recipes
- Spare screw elements and die plates shipped with initial order to prevent unplanned downtime
What to Include in Your Inquiry
To configure the corn flakes extrusion production line correctly, we need your raw material formulation including cereal types and moisture content, your target hourly output, and the specific flake or shape specifications you intend to produce. Share your factory floor dimensions and ceiling height so the line layout fits your space. Confirm your local voltage, frequency, and preferred control language so the PLC and MCC are programmed before dispatch.
Frequently Asked Questions
Q: How does screw configuration change when switching from corn to oat or multi-grain formulations?
A: Oat flour absorbs moisture differently and gelatinises at a lower temperature than corn. The kneading block arrangement and moisture injection points are adjusted to maintain correct dough rheology. The line supplier provides a documented screw element layout for each formulation you plan to run, so operators can swap configurations without trial-and-error on the production floor.
Q: What barrel temperature profile is needed for flaking versus direct-expanded cereal?
A: Flaking requires partial gelatinisation so the extrudate remains plastic enough to compress between rolls without shattering. Direct-expanded cereal needs higher barrel temperatures and greater shear for full expansion at the die. The PLC logs each zone temperature, allowing operators to store and recall distinct profiles for each product type on the same extruder.
Q: How is die geometry selected to control extrudate density for the flaking rolls?
A: Die aperture diameter and land length together determine back-pressure and the cross-section of the extrudate rope. Longer land length increases density, producing thicker flakes after compression. The supplier specifies die plates for each target flake thickness and documents the land length so replacements match the original performance.
Q: Can the same line produce both natural flakes and sugar-coated cereal shapes?
A: Yes. The natural corn flakes line follows mixing through extruding, flaking, drying, roasting, and cooling. The sugar-coated configuration adds sugar spraying, coating, and a second drying stage. The extruder and flaking stations serve both paths, and operators switch between product types by adjusting the die, screw profile, and downstream routing through the PLC.
Q: What trial run data confirms extrusion performance before shipment?
A: The manufacturer runs your actual raw material through the extruder in their testing workshop and documents extrudate density, gelatinisation degree, and flake quality. This trial run report ships with the equipment so you can verify that the screw configuration and barrel profile were matched to your formulation, not borrowed from a generic build.