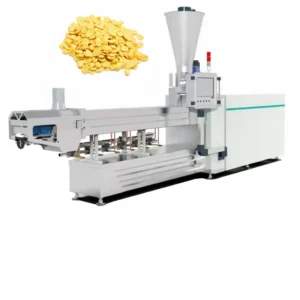
Precision-Matched Extrusion Parameters — screw elements and die geometry specified to the buyer’s grain blend, ensuring starch gelatinisation and expansion ratio hit the target flake density every run.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT75 / MT85 |
| Product Type | Corn Flakes Extrusion Production Line |
| Screw Type | Twin Screw |
| Installed Power | MT70: 160 kW / MT75: 210 kW / MT85: 190 kW |
| Power Consumption | MT70: 120 kW / MT75: 150 kW / MT85: 140 kW |
| Output Capacity | MT70: 150–200 kg/hr (basis to be confirmed) / MT75: 300–500 kg/hr (basis to be confirmed) / MT85: 300–400 kg/hr (basis to be confirmed) |
| Overall Dimensions | MT70: 41 × 1.5 × 2.2 m / MT75: 45 × 1.5 × 3.5 m / MT85: 43 × 1.5 × 3.2 m |
| Control System | PLC and MCC |
| Basic Raw Materials | Corn, rice, wheat, oat, barley powder |
| Heating Source (Dryer) | Gas or Electric |
| Flaking Machinery | Hydraulic double-roller system with separate motor drives and infrared temperature sensing |
| Hot Air Roasting Oven | Vibrating pan, high-temperature spraying tubes, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melter, elevator, coating drum, spraying nozzle |
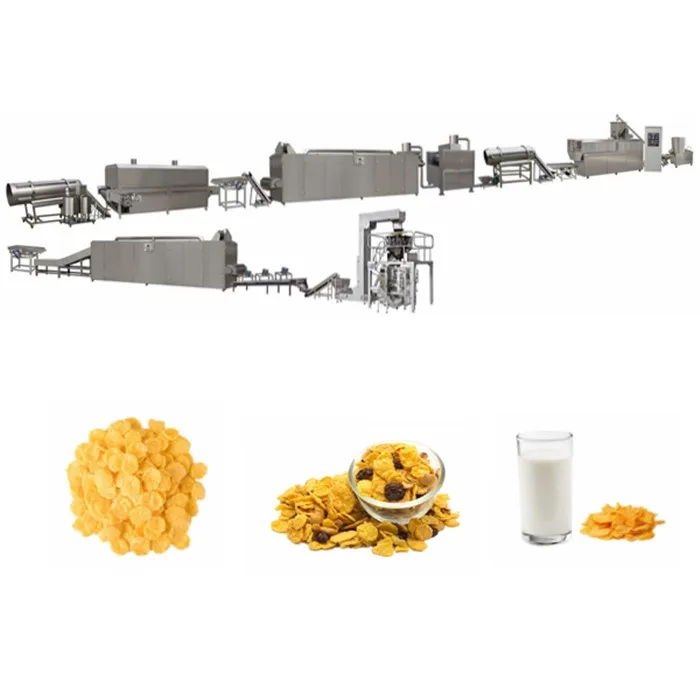
| Production Procedure | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Sugar Coating → Cooling → Packing |
| Assembly State | Complete production line |
| Standards | CE / ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal market | Corn grits or corn flour as primary grain base |
| Sugar-coated corn flakes with glazed finish | Corn base with sugar coating in tumble drum |
| Shaped breakfast cereals (rings, balls, stars, tubes) | Corn, rice, wheat, oat, or barley blends with die adjustment |
| Fortified breakfast cereals with added micronutrients | Grain powder blended with vitamin and mineral premix |
| Multi-grain puffed cereal formats | Mixed grain formulations combining rice, oat, and barley |
Why Generic Screw Builds Fail on Corn Flake Lines
A screw configuration lifted from a standard template rarely produces the correct corn flake texture or density — the flake either shatters on contact with milk or stays too dense and hard to bite. Here the corn flakes extrusion technology screw configuration die design parameters must be matched to the specific grain blend the buyer actually runs, not a default recipe.
I worked on a corn flake line last year where the initial build used a screw profile designed for wheat flour. The client’s actual raw material was coarse corn grits with a different gelatinisation window. Expansion came out uneven, and the flakes cracked during the flaking stage instead of pressing into clean sheets. We tore down the barrel, swapped the screw elements, and re-profiled the die — that rework delayed their commissioning by over two weeks [NEED_CITE: starch gelatinisation temperature variance between corn and wheat raw materials].
That experience sits behind every line we ship now. Before any extruder leaves the workshop, we run the buyer’s actual grain sample through a trial to confirm the expansion ratio, flake integrity, and final density meet the specification the market expects.
Barrel Temperature Zoning and Gelatinisation Control
Corn starch gelatinises within a narrow temperature band, and the barrel must deliver that heat profile consistently across every zone. The extruder on this line uses multiple independent heating zones along the barrel length, with the corn flakes extrusion technology screw configuration die design calibrated so that shear heat and external heating combine to bring the dough to the correct viscosity at the die face. Too cool and the starch remains partially raw, producing a hard, gritty flake. Too hot and the moisture flashes off prematurely, leaving the pellet brittle before it ever reaches the flaking rollers.
Die Geometry and Pellet Expansion Behaviour
The die determines the shape, size, and initial density of the extruded pellet — the intermediate form that gets pressed into a flake downstream. For corn flakes, the die orifice diameter and land length are chosen so the pellet exits with just enough expansion to create a porous internal structure, but not so much that it becomes a fully puffed snack. Die geometry also controls how the pellet behaves under the hydraulic flaking rollers. A pellet that expanded too much will collapse unevenly; one that expanded too little will resist flattening and crack at the edges [NEED_CITE: die land length influence on extrudate expansion ratio in cereal processing].
Reading the Specs Against Your Raw Material
Installed power ranges from 160 kW on the MT70 to 210 kW on the MT75, and these figures matter most when you match them against the moisture content and particle size of your grain blend. Coarser corn grits demand more mechanical energy to shear through the barrel than fine corn flour, so the motor must hold torque without stalling at the feed rate you need. The hydraulic flaking system uses separate motors for each roller, which means roll gap and pressure stay consistent even as roller surfaces wear over production cycles. Power consumption figures sit below installed capacity — the MT75 draws 150 kW against 210 kW installed — leaving thermal headroom for startup surges and heavier grain loads.
The hot air roasting oven uses a vibrating pan with high-temperature spraying tubes and two independent circulating fans, so heat distribution across the flake bed stays even and surface blistering develops uniformly. Cyclone dust removal on the roasting stage keeps fine particulate from recirculating and scorching against the flake surface.
What Happens When Extrusion Parameters Are Mismatched
When the screw configuration does not match the grain blend, the problems do not show up immediately — they emerge during the flaking and roasting stages where correction becomes expensive. Pellets with incomplete gelatinisation shatter under roller pressure, generating waste that clogs the dryer air circulation. Flakes with inconsistent density roast unevenly, leaving some batches under-toasted and others burnt at the edges. By the time the coating drum applies sugar, the texture variation is locked in and the final product fails the crispness test the buyer’s market demands [NEED_CITE: post-extrusion defects from incorrect screw element sequencing in cereal lines].
Why This Line Is Configured for Your Process
Every station from the mixer through the packing end is sized so that throughput matches — the extruder, flaking rollers, dryer, roasting oven, and coating drum are calculated together, not sourced separately and bolted into an unbalanced layout. The screw elements and die are selected after reviewing the buyer’s raw material data sheet, not pulled from a generic parts catalogue. Before shipment, a trial run on the buyer’s actual grain sample takes place in the in-house testing workshop, generating a report that documents expansion ratio, flake density, and texture against the agreed specification. Electrical schematics and voltage are confirmed against the target market’s grid standard before the control cabinet is wired. The PLC and MCC control architecture allows the operator to adjust barrel zone temperatures, screw speed, and feed rate from a single interface, keeping batch-to-batch consistency within tolerance.
Documentation & Verification
- Line layout drawing showing throughput matching between extruder, flaking rollers, and roasting oven
- Screw and die configuration record specific to your grain blend and target flake density
- Trial run report on your actual raw material documenting expansion, texture, and density results
- Electrical schematic with voltage and frequency confirmed for your local grid standard
- Machine specification sheet with dimensional footprint for facility planning
- Operation and maintenance manual covering barrel disassembly and roller gap calibration
Installation, Commissioning & Support
- Foundation requirements calculated from the MT75 line dimensions of 45 × 1.5 × 3.5 m with utility routing plan
- Dedicated power circuit sized for the 210 kW installed load with voltage and frequency matching your site supply
- Extruder barrel and flaking rollers shipped partially disassembled for container loading, reassembled on-site during commissioning
- First-run parameter setup including barrel zone temperatures, screw speed, and hydraulic roller pressure calibrated to your grain sample
- Operator training covering die changeover procedures for switching between flake and shaped cereal formats
- Wear parts list with lead times for screw elements, die plates, and flaking roller surfaces
What We Need to Scope Your Line
To size the extrusion and downstream stations correctly, share your primary grain type and particle size, the target output per shift, and your local voltage and frequency. If you plan to run both natural flakes and sugar-coated variants, or shaped cereal formats alongside standard flakes, let us know the changeover frequency so we can specify the die inventory and coating drum capacity. Sending a sample of your raw material allows us to run a trial before the quotation stage.
Frequently Asked Questions
Q: How is screw configuration selected for different grain blends like corn, rice, or oat?
A: Each grain has a distinct starch gelatinisation temperature and moisture absorption rate. We review your raw material composition, then select screw element types — conveying, kneading, and reverse elements — in a sequence that generates the right shear profile. The die orifice and land length are paired to that screw build so the pellet exits at the correct expansion ratio for flaking.
Q: What barrel temperature profile is needed for proper corn flake gelatinisation?
A: Corn starch typically gelatinises between 62°C and 72°C, but the barrel zones must account for frictional heat from screw rotation and the moisture already in the dough. We set a gradient across the heating zones, confirmed by thermocouples at each barrel section, then validate the result during the trial run on your specific corn grits or flour.
Q: How do you verify expansion ratio and flake density before the machine ships?
A: We run your raw material through the extruder in our testing workshop, collect the extruded pellets, measure their diameter and weight against the die orifice size, then pass them through the flaking rollers to check sheet integrity. A written report documents all readings against the agreed specification before dispatch.
Q: Can the same extruder produce both flat flakes and shaped cereals like rings or stars?
A: Yes. Switching from flakes to shaped cereals requires changing the die plate to the target geometry and adjusting the screw speed and barrel temperature to control expansion. The hydraulic flaking rollers are bypassed for shaped formats, and the extrudate goes directly to the dryer. We supply the die inventory and document the parameter set for each format.