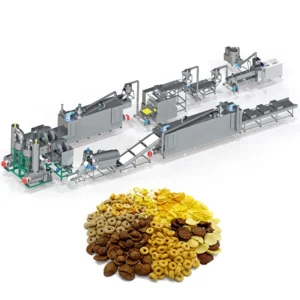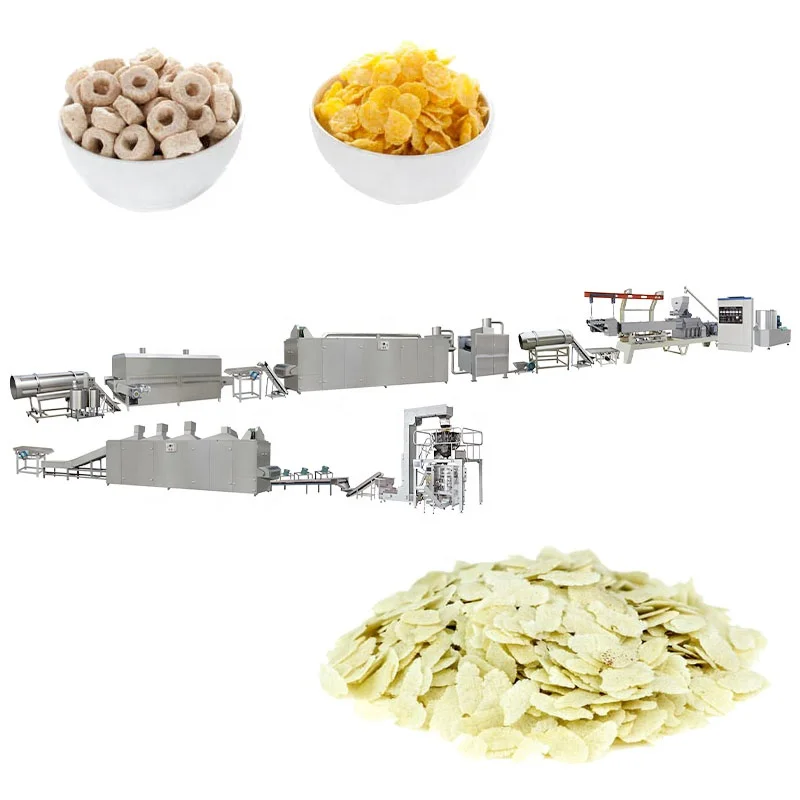
Screw Geometry Specified to Grain — Every MT-series corn flake extruder ships with screw elements and die plates matched to your actual corn, rice or multi-grain blend, verified through in-house trial runs before dispatch.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flake Production Line / Breakfast Cereal Extruder |
| Model | MT70 / MT85 / MT75 |
| Extruder Type | Twin Screw |
| Installed Power | 160 kW (MT70) / 190 kW (MT85) / 210 kW (MT75) |
| Operating Power | 120 kW (MT70) / 140 kW (MT85) / 150 kW (MT75) |
| Output Capacity | 150–200 kg/h (MT70); 300–400 kg/h (MT85); 300–500 kg/h (MT75) (basis not stated in source — confirm raw material type, moisture content and product format) |
| Overall Dimensions (L×W×H) | 41 × 1.5 × 2.2 m (MT70) / 43 × 1.5 × 3.2 m (MT85) / 45 × 1.5 × 3.5 m (MT75) |
| Control System | PLC (flaking machinery); MCC/PLC available for full line |
| Dryer Heating Source | Gas / Electric |
| Flaking Station | Hydraulic double-roller system, dual independent motors, infrared sensor temperature control |
| Roasting Oven | Hot air circulating with vibrating pan, high-temperature spray tubes, two separate fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spray nozzle |
| Screw Material | Wear-resistant alloy, special processing technology |
| Lubrication | Automatic lubricating and cooling system |
| Standards | CE (since 2014); ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal packaging | Corn powder or grits processed through mixing, extruding, flaking, drying, hot air roasting and cooling |
| Sugar-coated corn flakes with glazed surface finish | Corn or multi-grain base extruded, flaked, roasted then passed through sugar spraying and tumble coating stages |
| Multi-grain breakfast cereal formats | Blends of rice, wheat, oat and barley powder shaped into balls, tubes, rings, stars, wheels or flowers via die changes |
| Fortified infant and nutritional cereal | Vitamin and mineral premix incorporated at batching stage before extrusion, with gelatinisation locked in by barrel thermal profile |
Why Generic Screw Builds Sink Your Corn Flake Density
A twin-screw corn flake extrusion line rated at a headline capacity number means nothing if the screw profile was never matched to the starch behaviour of your specific grain source. The result shows up on day one: flakes that stick to the press rollers, uneven expansion in the barrel, or a final product that sinks straight to the bottom of the milk bowl instead of floating. We have walked onto sites where the previous supplier used a screw build copied from a generic wheat-based recipe, then wondered why a high-amylose corn variety refused to gelatinise at the same barrel temperatures. Screw configuration must be specified to the buyer’s actual raw material, not borrowed from a catalogue default.
When the extrusion section of a corn flakes extrusion production line is built on assumptions rather than trial data, the bottleneck migrates downstream. The dryer runs longer to compensate for excess moisture, the flaking rollers crush rather than press, and the roasting oven produces blistered surfaces on some flakes and pale undercooked surfaces on others. Operators end up throttling the feeder back, and the line never reaches the throughput the quotation promised [NEED_CITE: starch gelatinisation temperature thresholds for maize versus rice flour blends].
Barrel Zone Profiling for Starch Gelatinisation Control
Starch gelatinisation inside a twin-screw breakfast cereal extruder depends on three interacting variables: shear energy from the screw flights, residence time determined by barrel length, and the thermal gradient across successive heating zones. The MT-series barrels feature independently controlled heating zones so operators can establish a rising temperature profile — typically starting low in the feed section to prevent premature gelatinisation and ramping through the compression and metering sections. Adjusting this profile is how process engineers dial in the exact degree of cook that produces a flake with the right internal porosity for milk absorption without disintegration.
Die Geometry and Its Effect on Pellet Expansion
The die plate at the discharge end of a corn flakes extrusion production line determines pellet cross-section, which directly governs how the material behaves when it hits the flaking rollers. A die with too-large an orifice produces pellets that resist pressing and crack at the edges, while undersized orifices generate back-pressure that destabilises the extruder motor load. For the MT70, MT85 and MT75 models, die selection is documented against the target flake thickness and the buyer’s grain formulation so that pellet density entering the flaking station stays within the hydraulic roller system’s pressing range [NEED_CITE: relationship between die land length and extrudate density in cereal processing].
Reading the Spec Sheet for What It Actually Controls
The installed power figures — 160 kW for the MT70, up to 210 kW for the MT75 — reflect the thermal and mechanical energy budget available for starch conversion across the barrel length. Higher installed power supports longer barrel configurations with more heating zones, giving the operator finer control over the gelatinisation window. The automatic lubrication and cooling system on the screw shaft maintains bearing temperature within tolerance during continuous runs, which matters because a bearing running hot transfers unwanted heat into the feed zone and disrupts the moisture balance. Twin-screw operation over single-screw provides positive material conveyance through the compression section, essential when processing high-fat or high-fibre grain blends that tend to slip in a single-screw channel. The PLC-controlled flaking station with hydraulic double rollers and infrared temperature monitoring ensures each pellet is pressed at a consistent surface temperature, eliminating the thickness variation that leads to mixed crispness in the final pack.
The Cost of Skipping the Trial Run
Sending an extruder to site without first running the buyer’s grain through the barrel is how commissioning delays start. The screw elements arrive configured for a reference material, the operator loads local corn flour with different particle size and moisture content, and the extrudate comes out either under-cooked or over-sheared. Flaking rollers then apply pressure to pellets that lack the internal structure to compress evenly, producing broken fragments rather than intact flakes. Two weeks of line downtime follow while replacement screw elements are manufactured and shipped, and the roasting oven parameters have to be recalibrated from scratch to match the new pellet characteristics [NEED_CITE: common causes of commissioning delay in cereal extrusion installations].
Engineering Decisions That Reach the Site Intact
Screw configuration and die design are specified to the buyer’s grain blend and target flake density, documented in a configuration record that travels with the machine. Every corn flakes extrusion production line undergoes a full trial run in the testing workshop using the customer’s actual raw material before packing, generating a report on expansion ratio, pellet density and flake integrity. Line throughput is calculated station by station — extruder output balanced against dryer capacity, flaking roller feed rate, roasting oven dwell time and coating drum volume — so no single section chokes the rest. Electrical schematics are confirmed for voltage, frequency and PLC language against the destination facility before the control panels are wired. Wear parts including screw elements, die plates and roller surfaces are inventoried and packed alongside the line so the first scheduled replacement does not halt production.
Documentation & Verification
- Line layout drawing with capacity calculation matched to your grain blend and target output rate
- Screw and die configuration record specifying element profile and orifice geometry to your formulation
- Trial run report documenting expansion, density and flake texture on your raw material before shipment
- Electrical schematic with voltage, frequency and PLC control language confirmed to your facility standard
- CE declaration of conformity and ISO certificate for customs and site regulatory compliance
- Operation and maintenance manual covering barrel zone settings, roller pressure calibration and lubrication intervals
Installation, Commissioning & Support
- Foundation plan accounting for the full 41–45 m line length and vibrating roasting pan dynamic loads
- Dedicated electrical circuit sized to the 120–150 kW operating draw with confirmed voltage and frequency
- Modular delivery with flaking station, roasting oven and coating drum reassembled on site by project engineers
- First-run commissioning including barrel temperature ramp-up, hydraulic roller pressure setting and PLC parameter entry
- Operator training on die changeover, screw element inspection and infrared sensor calibration at the flaking station
- Spare wear parts kit with initial screw elements, die plates and roller surfaces for the first maintenance cycle
What to Include in Your Enquiry
To configure a corn flakes extrusion production line that holds capacity on your actual material, send through the grain type and blend ratios you plan to run, along with moisture content at the batching stage. Include your target daily output, the floor area and ceiling height available for the line layout, and the local voltage and frequency at your facility. If you have existing upstream mixers or downstream packing equipment, share the model and throughput so we can match station capacity across the full line.
Frequently Asked Questions
Q: How is screw configuration and die design matched to my specific grain formulation and target flake density?
A: We run your actual grain blend through the extruder in our testing workshop, measuring expansion ratio and pellet density at different barrel temperatures and screw profiles. The configuration that produces pellets pressing cleanly into intact flakes is documented and locked in before the machine is built. That record ships with the line so your process team has the baseline for future adjustments.
Q: Can the line hold its rated output on my actual raw material blend, and how is this verified?
A: Rated output figures are based on reference conditions and must be confirmed against your specific grain type and moisture content. We verify throughput during the pre-shipment trial run in our workshop, running your material through every station from extrusion to packing. The trial report documents actual output and identifies any station that needs capacity adjustment before dispatch.
Q: What barrel temperature profile and moisture range are needed for proper starch gelatinisation?
A: The required profile depends on your grain’s amylose-to-amylopectin ratio and the starting moisture at the feeder. High-amylose corn typically needs a steeper temperature ramp and slightly higher moisture than rice or oat blends. Our trial run establishes the zone-by-zone settings that achieve full gelatinisation without over-shearing, and those settings are recorded in your operation manual.
Q: How are voltage, frequency and PLC control language confirmed before commissioning?
A: We request your facility’s electrical specification during the quotation stage and confirm it on the electrical schematic before the control panels are built. The PLC interface language is set to match your operator team’s requirement. This prevents rewiring or software reloading during on-site commissioning.
Q: What spare wear parts are included, and what is the replacement schedule?
A: The initial spare kit includes screw elements, die plates and flaking roller surfaces sized to your configuration. Replacement intervals depend on grain abrasiveness and daily run hours — your maintenance manual provides inspection checkpoints and estimated service life for each component based on the trial run data.