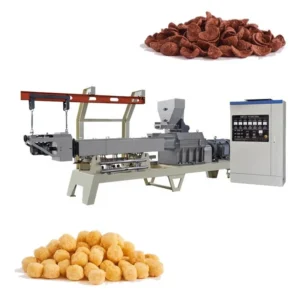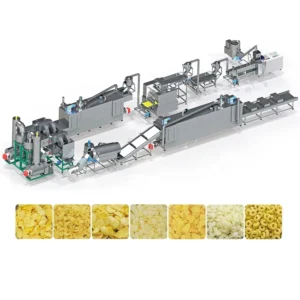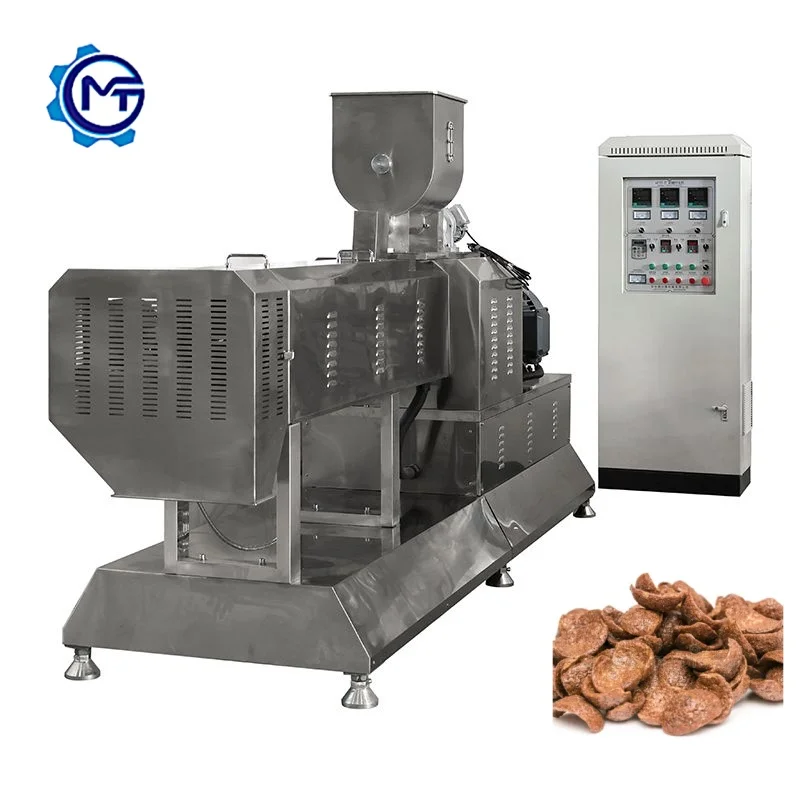
Screw Profile Matched to Your Flour Blend — Every MT75 corn flakes line ships with screw elements and die geometry configured after trial runs on the buyer’s actual cereal formula, not a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Corn Flakes Production Line |
| Extruder Type | Twin Screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC control with MCC integration |
| Heating Source (Dryer) | Gas / Electric / Steam options |
| Flaking Machinery | Hydraulic double-roller system with infrared sensor temperature control |
| Roasting Oven | Conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits or corn flour blends |
| Sugar-coated breakfast cereals | Corn, rice, or multi-grain flakes with sugar syrup coating |
| Cocoa-flavoured cereal flakes | Wheat or corn base with cocoa powder integration |
| Multi-grain flake formats | Rice, wheat, oat, and barley powder blends |
| Shaped puffed cereal snacks | Rings, balls, stars, and fruit loops via die changeover |
Why Barrel Temperature Zoning Decides Your Flake Density
Precise heat staging across the barrel sections determines whether starch gelatinises fully before the die — and that controls whether your flakes stay crisp in the bowl or go soggy within minutes.
When I first started setting up cereal lines, I watched a producer in Eastern Europe lose an entire production run because their corn flakes cracked during flaking. The expansion ratio was wrong. The barrel profile had been copied from a standard wheat formula, but they were running a high-amylose corn variety. Corn flakes extrusion production line technology demands that each heating zone be mapped to the specific starch behaviour of your raw material. Moisture content entering the barrel, shear rate from the screw elements, and residence time all interact to set the final pellet density before it reaches the flaking rollers [NEED_CITE: starch gelatinisation temperature ranges for corn versus rice flour].
Get this wrong and the flakes either shatter under roller pressure or compress into dense chips that never achieve the surface blistering consumers associate with quality breakfast cereal.
Shear Control and Starch Gelatinisation
The twin-screw configuration allows independent adjustment of screw element sequencing to manage mechanical shear alongside thermal input. For corn-based formulas, this means the corn flakes extrusion production line technology can maintain the gelatinisation window long enough for complete starch conversion without triggering premature expansion at the die face. Different cereal blends — particularly those incorporating oat or barley — require reconfigured screw profiles because their lipid and fibre content alters how heat transfers through the dough mass inside the barrel.
Die Geometry and Pellet Consistency
The die design controls back-pressure and flow uniformity, which directly affects how consistently each pellet exits the extruder. Uniform pellets mean the flaking rollers apply even pressure across every piece, producing flakes of consistent thickness. If the die orifices are sized for a different viscosity range, some pellets extrude thicker than others, and the downstream flaking station cannot compensate [NEED_CITE: die land length and its effect on extrudate swell in twin-screw systems]. This is why die specification must be locked to your confirmed formula before production begins.
Reading the Power and Dimension Data
The MT75 draws 210 kW installed with 150 kW operational consumption, indicating the thermal and mechanical headroom available for high-moisture cereal doughs that demand substantial energy input for gelatinisation. The 45-metre line footprint encompasses every station from mixing through packing, which matters when planning factory layout and utility routing. The hydraulic flaking system with infrared temperature sensing maintains roller surface conditions within a narrow band, preventing the thermal shock that causes flake delamination. Dual circulating fans in the roasting oven create the convective profile needed for surface blistering without over-drying the flake interior, while the cyclone dust removal keeps particulate from recirculating onto product surfaces.
What Happens When Extruder and Dryer Capacity Mismatch
A line assembled from separate vendors often arrives with an extruder rated for throughput that the dryer cannot match, creating a bottleneck where product backs up and cools before entering the roasting phase. This thermal gap means flakes enter the oven below the temperature needed for proper blistering, and the result is a flat, dense texture that fails bowl-life expectations. Corn flakes extrusion production line technology only delivers consistent output when throughput is calculated across every station simultaneously, not specified in isolation [NEED_CITE: throughput matching principles in multi-stage food processing lines].
Engineering Accountability Across the Line
Screw configuration and die design are specified to your raw material formula and target flake density, documented in a configuration record you receive before shipment. The in-house testing workshop runs your actual cereal blend before the line leaves the factory, generating a trial run report that locks parameters. Line layout and capacity calculation account for your factory footprint rather than forcing a standard arrangement. Electrical schematics confirm voltage, frequency, and control language before production starts, eliminating commissioning delays caused by mismatched power supplies. The PLC and MCC control architecture integrates every station under one system, so throughput coordination is managed programmatically rather than relying on manual speed adjustments between standalone machines.
Documentation & Verification
- Line layout and capacity calculation matched to your factory dimensions and throughput targets
- Screw and die configuration record specifying element sequence for your cereal formula
- Trial run report documenting results on your raw material before shipment
- Electrical schematic confirming voltage, frequency, and PLC control language
- Factory test record verifying integrated line performance prior to dispatch
Installation, Commissioning & Support
- Foundation requirements calculated for the 45-metre line footprint and 210 kW total power draw
- Dedicated electrical circuits specified for PLC and MCC control cabinet integration
- Sequential station assembly from extruder through roasting oven with utility connection mapping
- First-run parameter setting using trial run report data as baseline for your raw material
- Operator training covering screw configuration adjustments and die changeover procedures
- Wear parts list covering screw elements, die plates, and flaking roller surfaces
What We Need to Configure Your Line
Provide your cereal flour formulation, including the ratio of corn to any secondary grains, along with target flake thickness and bowl-life expectations. Confirm your factory floor dimensions and ceiling height so the line layout can be drafted to your space. Specify local voltage and frequency, preferred control language for the PLC interface, and whether you need the sugar coating station integrated or a natural-flake-only configuration.
Frequently Asked Questions
Q: How is screw configuration selected for different cereal flour blends and target flake densities?
A: Screw elements are sequenced based on your specific flour blend’s starch composition, lipid content, and fibre ratio. High-amylose corn requires different shear staging than oat-heavy blends. The configuration is validated through trial runs on your raw material in the testing workshop, and the final element sequence is documented in a configuration record supplied before shipment.
Q: What barrel temperature profile and moisture range produce the correct expansion for crispy corn flakes?
A: Temperature zones are staged to bring the dough through gelatinisation without triggering premature expansion. Moisture entering the barrel typically falls within a range that supports full starch conversion while allowing controlled flash-off at the die. Exact setpoints are established during your raw material trial run and recorded for commissioning reference.
Q: Can a trial run be performed on my specific raw material before the line ships?
A: Yes. The in-house testing workshop conducts production runs using your cereal formula on the configured extruder and downstream stations. A trial run report documents output quality, flake density, and parameter settings, which then serve as the baseline for on-site commissioning at your facility.
Q: How do you ensure throughput is matched across extruder, flaker, dryer, and roaster to avoid bottlenecks?
A: Line capacity is calculated across all stations simultaneously during the layout phase. The extruder output rate is balanced against flaking roller throughput, dryer belt speed, and roasting oven residence time so that no single station creates a product backlog or thermal gap between stages.
Q: What die and mould options are available for producing shaped cereal formats beyond standard flakes?
A: The extruder accepts interchangeable die plates that produce pellets in shapes including rings, balls, tubes, stars, and fruit loops. These shaped pellets bypass the flaking station and proceed directly to drying and roasting. Die changeover allows a single line to alternate between flake production and shaped cereal formats.