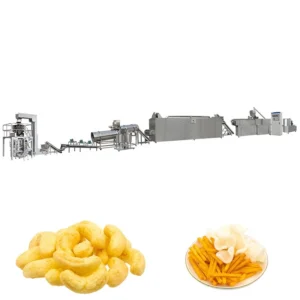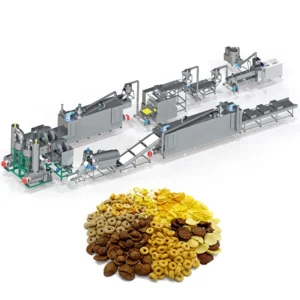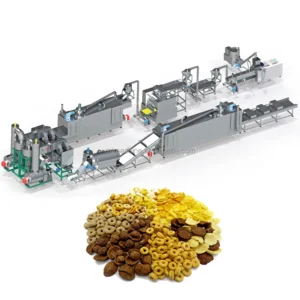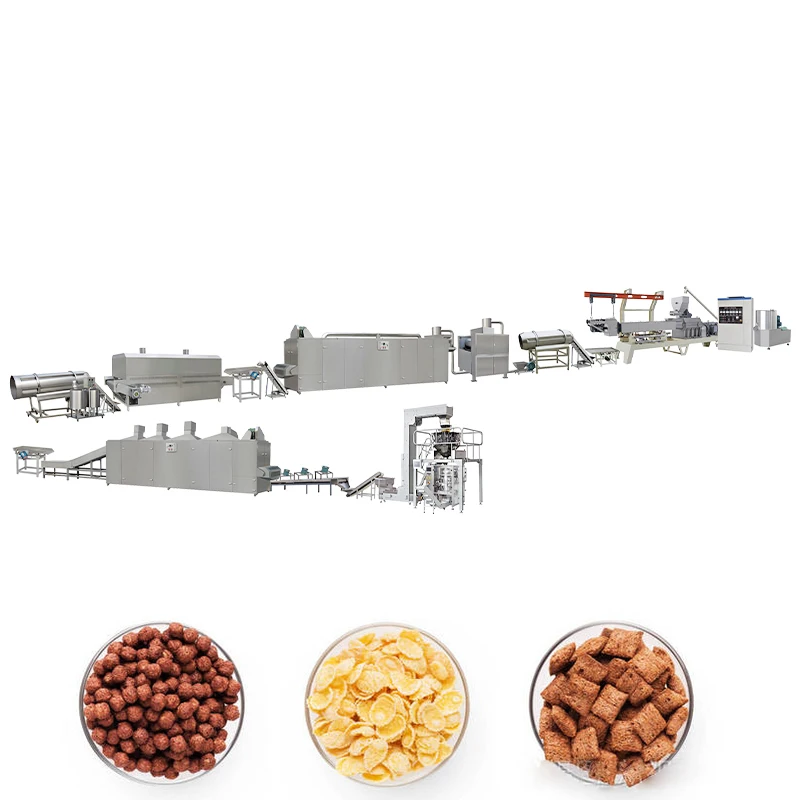
Engineered Screw Profiles — Every MT75 barrel and screw element is matched to your specific grain blend and target flake density, then proven with an in-house trial run on your actual raw material before the line ships.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line / Twin Screw Food Extruder Line |
| Extruder Type | Twin Screw |
| Available Models | MT70 / MT75 / MT85 |
| Installed Power (MT75) | 210 kW |
| Power Consumption (MT75) | 150 kW |
| Output Capacity (MT75) | 300–500 kg/h (basis not stated in source — confirm raw material, moisture, product format) |
| Overall Dimensions (MT75) | 45 × 1.5 × 3.5 m |
| Control System | PLC on flaking machinery; MCC & PLC available for full line |
| Screw Material | Special wear-resistant alloy |
| Flaking Station | Hydraulic double-roller system, dual independent motors, infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric (selectable) |
| Roasting Oven | Hot air circulating, conciliation burner, dual circulating fans, cyclone dust removal, vibrating pan |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Die Configuration | Interchangeable moulds for multiple cereal shapes |
| Line Stations | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Cooling → Packing (natural variant); additional Sugar Spraying → Sugar Coating → Drying for coated variant |
| Automation | Automatic lubrication, cooling function, PLC-controlled key stations |
| Assembly State | Complete line, pre-assembled stations |
| Customization | Layout to buyer’s factory size; voltage and frequency confirmed pre-production |
| Standards | CE (since 2014), ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn, rice, wheat, oat, barley powder |
| Sugar-coated corn flakes | Corn grits with sugar glaze or honey coating |
| Variety-shaped breakfast cereals | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart shapes via interchangeable dies |
| Granola and fortified cereals | Multi-grain blends with added vitamin and mineral premix |
| Puffed snack diversification | Same twin-screw extruder platform adapted for direct-expanded snacks |
What Your Flour Blend Has to Do with Extrusion Stability
Screw configuration must be selected against the actual raw material — not the brochure grain.
A nominal throughput figure on a corn flakes line tells you almost nothing if your local corn flour has higher fiber or different starch composition than what the extruder was tuned for. I have watched lines stall within the first hour because the compression ratio was set for a standard maize profile while the mill was feeding something far more abrasive and less gelatinisation-friendly. The result is uneven expansion, inconsistent flake thickness downstream, and a roasting oven that cannot deliver uniform blistering. Matching the corn flakes extrusion technology twin screw profile to your specific flour blend, moisture content, and target bowl-life is the difference between a line that runs and one that constantly needs operator intervention [NEED_CITE: raw material variability in grain processing across regional supply chains].
Shear, Moisture, and Starch Gelatinisation in the Barrel
Getting a corn flake that holds its crunch in milk requires controlling how starch gelatinises inside the barrel. The twin-screw configuration allows operators to adjust shear intensity and residence time by rearranging conveying and kneading elements along the shaft. Moisture content at the feed point and any steam injection along the barrel directly influence the degree of gelatinisation — too little and the flake turns out hard and glassy, too much and it collapses after flaking. This is where corn flakes extrusion technology twin screw design earns its keep: the ability to dial in the exact mechanical and thermal energy input that your grain blend demands, rather than relying on a single fixed screw profile that only works on one reference material.
Barrel Temperature Profile and Flake Density Control
Each heating zone along the barrel contributes to a temperature gradient that governs how the dough transitions from raw flour to a plasticised mass ready for the die. A flat or poorly staged profile produces extrudate that expands unpredictably when it exits the die, making it nearly impossible for the flaking rollers to achieve uniform thickness. On the lines I have commissioned across West Africa, we spent more time tuning zone temperatures than any other parameter, because the ambient humidity and local water temperature shift the energy balance enough to change the final flake density [NEED_CITE: starch gelatinisation temperature ranges for maize and multi-grain blends]. The PLC-controlled barrel zones on the MT75 give operators the resolution to correct these drifts shift by shift.
Reading the Specs That Actually Matter
The installed power of 210 kW on the MT75 configuration signals the mechanical energy available for shear and conveying inside the barrel — a higher figure generally means the extruder can handle tougher, higher-fiber grain blends without stalling. The hydraulic double-roller flaking station with independent dual motors lets each roller respond to load variations separately, which matters when extrudate density fluctuates slightly between batches. Infrared sensor temperature control at the flaking point catches surface temperature deviations before they translate into inconsistent sheet thickness. The interchangeable die set means a single extruder platform can shift between corn flakes rings, fruit loops, and stars without a full line changeover — useful when a producer wants to test new formats on the same corn flakes extrusion technology twin screw installation.
The Hidden Cost of a Generic Screw Build
When screw elements are copied from a standard template rather than configured for your material, the problems rarely show up during a factory test on reference flour. They emerge weeks after commissioning, when your actual supply arrives and the extrudate starts arriving at the flaking station either over-expanded or undercooked. The flakes crack during roasting, the coating drum cannot apply an even glaze, and your packing line sees a rejection rate that creeps upward every production run [NEED_CITE: post-installation product consistency failures in grain extrusion]. Operators compensate by slowing the line, which means your actual throughput never reaches the numbers you planned around.
Why Buyers Spec the Line Here
Screw configuration and die design are documented against your raw material sample and target flake density, not pulled from a generic build sheet. The in-house testing workshop runs your actual flour blend through the extruder before the line ships, producing a trial run report you can review. Throughput is matched across every station — mixing, extruding, flaking, drying, roasting, cooling, packing — so no single unit bottlenecks the rest. Electrical schematics are confirmed for your local voltage and frequency before fabrication starts, avoiding the commissioning delays I have seen strand equipment on factory floors for weeks. CE and ISO certification documentation is supplied as part of the delivery package.
Documentation & Verification
- Line layout and capacity calculation with throughput matched across every station
- Screw and die configuration record specific to your grain blend and target flake shape
- Trial run report on your raw material conducted before shipment
- Electrical schematic with voltage and frequency confirmed for your market
- Operation and maintenance manual with wear parts list for screw elements and dies
Installation, Commissioning & Support
- Foundation plan accounts for the MT75 line footprint of up to 45 m in length
- Power supply routed for 210 kW installed load with dedicated circuit breaker sizing
- Pre-assembled stations reduce on-site mechanical fitting time during installation
- PLC parameter sets loaded with barrel zone profiles matched to your trial run results
- Operator training covers screw element rearrangement for different grain blends
- Wear parts list identifies high-wear screw sections and die plates for first reorder
What to Prepare Before You Request a Quote
Share the specific grain or multi-grain flour you plan to run, including typical moisture content and any fiber or protein data from your mill. Confirm the daily output target and whether you need both natural and sugar-coated variants from the same line. Send your local voltage, frequency, and preferred control language so the electrical package can be locked in before production.
Frequently Asked Questions
Q: How is screw configuration selected for different grain blends and target flake density?
A: The screw element sequence — conveying, kneading, and reverse elements — is arranged based on your flour’s starch content, fiber level, and the density your market expects. A trial run on your actual raw material in the testing workshop confirms the configuration before the extruder ships, so adjustments happen at the factory, not on your floor.
Q: What barrel temperature profile supports proper starch gelatinisation in corn flakes?
A: A staged profile gradually raises dough temperature through the barrel zones, typically starting moderate at the feed section and increasing toward the die. The PLC-controlled zones on the MT75 let operators fine-tune each section independently to match their grain blend’s gelatinisation window and ambient workshop conditions.
Q: How are expansion and flake crispness controlled during extrusion and roasting?
A: Expansion at the die is governed by moisture content, barrel temperature, and screw shear intensity. The downstream hot air roasting oven with dual circulating fans and precise temperature control then sets the final surface blistering and crispness, while cyclone dust removal keeps the product clean throughout the cycle.
Q: Can the die be changed to produce multiple cereal shapes on the same line?
A: Yes. The extruder accepts interchangeable moulds for shapes including ball, tube, stick, ring, fruit loop, star, wheel, flower, and heart. Switching dies allows the same twin-screw platform to produce varied breakfast cereal formats without replacing the core extrusion hardware.
Q: How does moisture content and steam injection affect extrudate texture before flaking?
A: Moisture determines how completely starch gelatinises inside the barrel. Too little moisture leaves hard, under-expanded extrudate that cracks under the flaking rollers. Controlled steam injection at specific barrel zones raises moisture locally, improving plasticity and producing a sheet that flakes evenly and roasts to a consistent crispness.